Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer specializing in the design, development, and production of material handling systems. The company is headquartered in Shandong, China, and has established a strong reputation in the industry for its advanced technology and reliable products. One of the core offerings from headpowder is the Rare Earth Crystal Powder Material Handling System, which is engineered to meet the specific demands of handling and transporting rare earth crystal powders efficiently and safely.
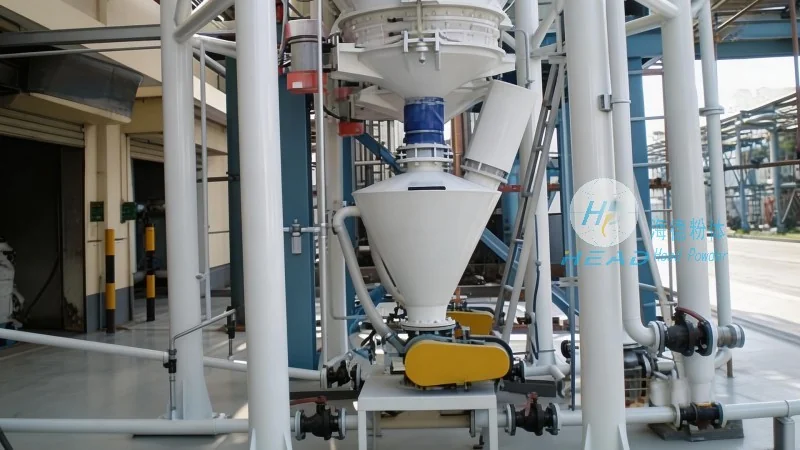
Overview of the Rare Earth Crystal Powder Material Handling System
The Rare Earth Crystal Powder Material Handling System is a sophisticated solution designed to handle the unique properties of rare earth crystal powders. These materials are often characterized by their fine particle size, high value, and potential for dust generation, which requires specialized equipment to manage effectively. The system integrates multiple components, including feeding mechanisms, conveying equipment, storage solutions, and control systems, to ensure a seamless and controlled material flow. By leveraging advanced engineering principles, headpowder has developed a system that not only enhances operational efficiency but also maintains the integrity and purity of the rare earth crystal powders throughout the handling process.
Operation Process of the Material Handling System
The operation of the Rare Earth Crystal Powder Material Handling System typically begins with the intake of raw materials. The system is equipped with a specialized feeding hopper that can accommodate bulk rare earth crystal powders. The hopper is designed with a smooth interior surface to minimize material buildup and ensure consistent flow. Once the material is loaded into the hopper, an electric or pneumatic feeder initiates the feeding process. The feeder controls the rate of material discharge, which is crucial for maintaining a stable and controlled flow to the subsequent conveying equipment. The conveying equipment, such as a screw conveyor or a pneumatic conveyor, then transports the powder from the feeding hopper to the storage silo or processing unit. The system may include multiple stages of conveying, with intermediate storage bins to buffer the material and prevent bottlenecks. Each stage is monitored by sensors and control devices to ensure that the material is moved at the optimal speed and volume. The final stage of the operation involves the discharge of the powder into the processing equipment or storage containers, completing the material handling cycle.
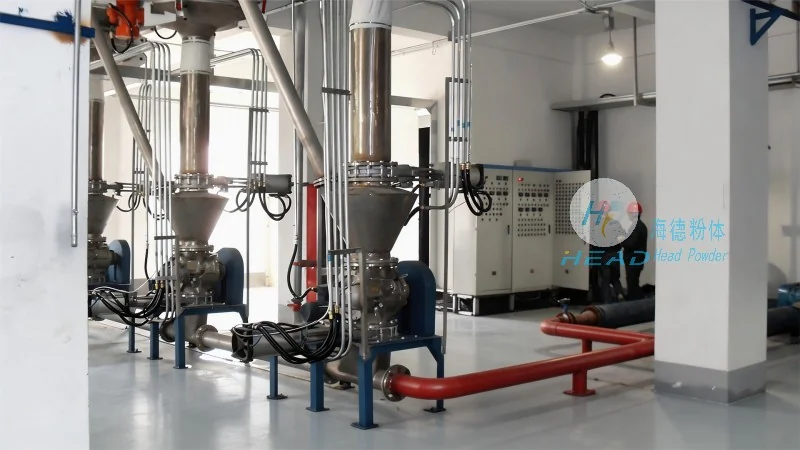
Working Principle of the System Components
The Rare Earth Crystal Powder Material Handling System operates based on a combination of mechanical, pneumatic, and electrical components, all working in harmony to achieve efficient material handling. The feeding mechanism, often a rotary valve or a vibratory feeder, ensures that the powder is released in a controlled manner from the hopper. The conveying equipment, such as a screw conveyor, uses rotating screws to move the powder forward. The screw design is optimized to handle fine powders without causing excessive friction or particle degradation. For systems requiring longer distances or more complex routes, a pneumatic conveyor may be employed, which uses compressed air to transport the powder through a network of pipes. The control system, typically a programmable logic controller (PLC), monitors all operational parameters, including flow rate, pressure, and temperature. Sensors are strategically placed throughout the system to detect any abnormalities, such as blockages or overfilling, and trigger appropriate responses to prevent equipment damage or material loss. The integration of these components allows the system to operate autonomously, with minimal human intervention, while maintaining high levels of accuracy and reliability.
Key Features and Benefits
Headpowder's Rare Earth Crystal Powder Material Handling System is equipped with several key features that enhance its performance and usability. One of the primary features is the dust control system, which includes sealed hoppers and conveyor sections to prevent dust emissions and protect the environment. The system also incorporates a level monitoring system to ensure that the storage silos are not overfilled or underfilled, which helps in maintaining consistent material levels and preventing spills. Additionally, the system is designed with easy access points for maintenance and cleaning, reducing downtime and operational costs. The use of high-quality materials, such as stainless steel for the hopper and conveyor components, ensures durability and resistance to corrosion, which is essential for handling rare earth powders that may be chemically reactive. The overall benefits of the system include improved operational efficiency, reduced labor costs, enhanced safety, and better material quality control. By implementing this system, companies can achieve higher throughput, minimize material loss, and comply with environmental regulations more effectively.
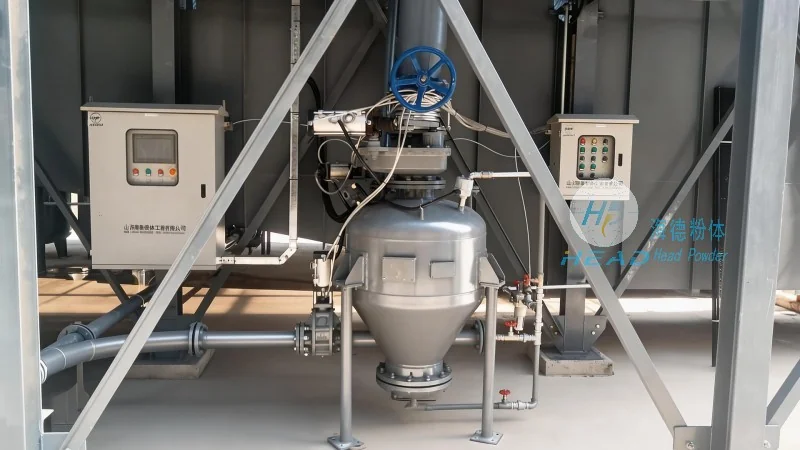
Application and Industry Relevance
The Rare Earth Crystal Powder Material Handling System is widely used in industries that rely on rare earth crystal powders, such as electronics, aerospace, and renewable energy. In the electronics industry, these powders are used in the production of magnets and other components, where precision and purity are critical. The system's ability to handle fine powders without degradation makes it ideal for these applications. In the aerospace sector, rare earth powders are used in high-performance alloys, and the system ensures that the materials are transported safely and efficiently to the manufacturing lines. The system's adaptability allows it to be customized for various production scales, from small-scale laboratory applications to large-scale industrial operations. By providing a reliable and efficient material handling solution, headpowder helps its clients to improve their production processes and maintain a competitive edge in the market.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s Rare Earth Crystal Powder Material Handling System represents a significant advancement in material handling technology. Through its integrated design and advanced components, the system offers a comprehensive solution for the efficient and safe handling of rare earth crystal powders. The operation process, which includes feeding, conveying, and storage, is carefully engineered to optimize performance and maintain material integrity. The working principle, based on mechanical, pneumatic, and electrical components, ensures smooth and controlled material flow. With key features such as dust control and level monitoring, the system provides enhanced safety and operational efficiency. As industries continue to rely on rare earth materials for their advanced applications, the importance of reliable material handling systems cannot be overstated. Headpowder's system, with its proven performance and customization options, is a valuable asset for any company looking to enhance its production capabilities and meet the demands of the modern manufacturing landscape.




