Dust-removed coke powder pneumatic conveying is a specialized method used in industrial applications to transport fine coke powder materials efficiently and safely. This technology plays a crucial role in various industries, particularly in the chemical, metallurgical, and power sectors, where handling fine powders requires precise control to prevent dust explosions and ensure material integrity. The process involves using compressed air or other gas to transport the powder through a pipeline system, making it an ideal solution for long-distance and high-temperature applications.
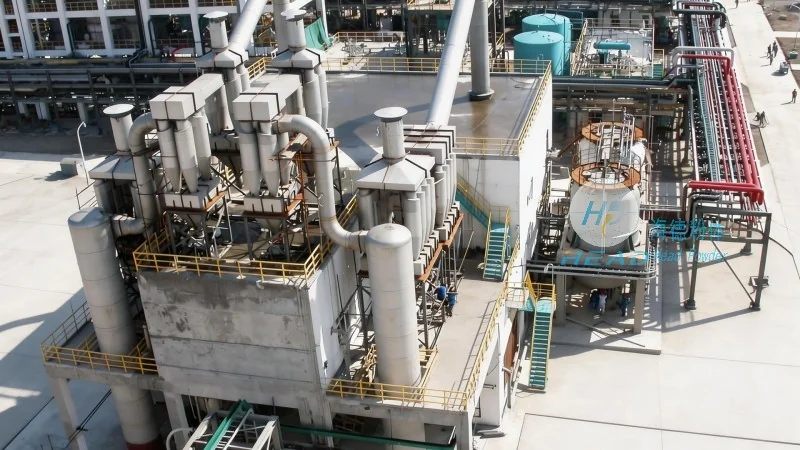
Understanding Dust-Removed Coke Powder Pneumatic Conveying
Dust-removed coke powder pneumatic conveying refers to the process of transporting coke powder that has been pre-treated to remove dust and moisture. The primary goal is to eliminate the risk of dust accumulation and explosion hazards, which are common in traditional bulk powder handling. By removing dust, the system ensures a cleaner, more controlled environment, reducing operational risks and improving material quality. The technology is particularly relevant for industries dealing with coke, a byproduct of coal processing, which is widely used in steel production and other industrial processes.
The Core Design Principles of Pneumatic Conveying Systems
The design of a dust-removed coke powder pneumatic conveying system is based on several key principles to ensure optimal performance and safety. First, the system must incorporate efficient dust removal mechanisms, such as cyclone separators or bag filters, to capture fine particles before they enter the conveying line. This step is critical for preventing dust contamination and maintaining the purity of the coke powder. Second, the system relies on a consistent and controlled air flow, typically generated by positive displacement blowers or rotary lobe pumps, to move the powder through the pipeline. The air velocity must be maintained at a level that prevents particle settling and ensures smooth transport.
Third, the pipeline design is crucial for minimizing pressure drop and preventing blockages. The use of appropriate pipe diameters, bends, and elbows, along with the installation of airlocks and surge tanks, helps maintain the flow rate and prevents material buildup. Additionally, the system may include features like in-line mixers or agitators to prevent caking or agglomeration of the coke powder, which could impede the conveying process. These design elements work together to create a reliable and efficient system that meets the specific requirements of coke powder handling.
Key Components and Their Functions in the System
A typical dust-removed coke powder pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. The first component is the material feed system, which includes a hopper or bin equipped with a feeder, such as a rotary valve or screw conveyor, to control the flow of coke powder into the system. This component ensures a steady and controlled input of material, preventing overloading or underloading of the conveying line.
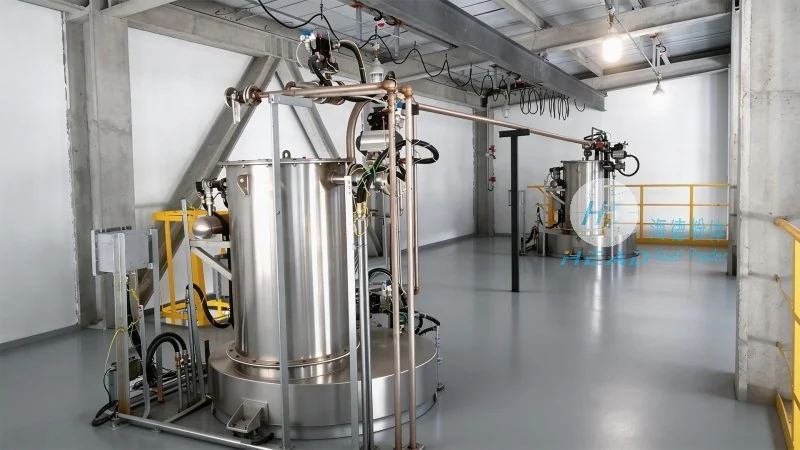
Next, the dust removal unit is essential for maintaining the purity of the coke powder. This unit typically includes a cyclone separator, which uses centrifugal force to separate dust particles from the air stream, and a bag filter or cartridge filter to capture any remaining fine particles. The collected dust is then discharged into a collection bin for disposal or recycling. The efficiency of the dust removal system directly impacts the overall performance and safety of the conveying process.
The air supply system, which includes the blower or pump, provides the necessary pressure and volume of air to transport the powder. Positive displacement blowers are commonly used due to their ability to maintain consistent pressure even at low flow rates, which is important for handling fine powders that may settle in the pipeline. The air is then introduced into the pipeline through a venturi or a straight inlet, ensuring a smooth transition of the powder into the conveying line.
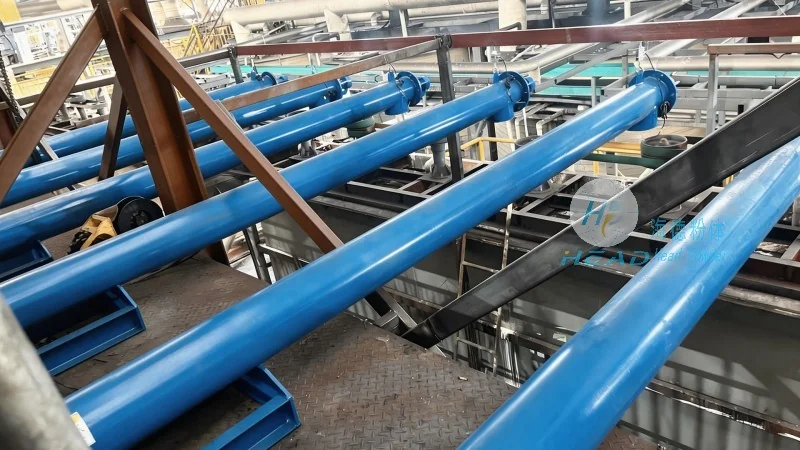
The pipeline itself is constructed from materials that are resistant to corrosion and wear, such as stainless steel or high-density polyethylene. The choice of material depends on the properties of the coke powder, including its abrasiveness and chemical compatibility. The pipeline is designed with appropriate bends and elbows to minimize pressure losses and prevent particle accumulation. Airlocks and surge tanks are also included in the system to regulate the flow and prevent backflow or overpressure conditions.
Advantages of Dust-Removed Coke Powder Pneumatic Conveying
Implementing dust-removed coke powder pneumatic conveying offers several advantages over traditional handling methods. First, it significantly reduces the risk of dust explosions by removing fine particles that could ignite. This enhances workplace safety and compliance with industry regulations. Second, the system provides a more controlled and efficient way to transport coke powder, reducing material loss and improving overall process efficiency. The ability to handle fine powders without caking or agglomeration ensures that the material remains in a consistent state, which is crucial for downstream processes like blending or combustion.
Third, the system allows for long-distance and high-temperature transport, making it suitable for applications where traditional methods may be impractical. The use of compressed air as the conveying medium also enables the system to operate in environments where electric motors are not feasible or safe. Additionally, the dust removal process improves the quality of the coke powder by removing contaminants, which can enhance its performance in industrial applications.
Applications and Industries Benefiting from This Technology
Dust-removed coke powder pneumatic conveying is widely used in various industries that rely on coke as a raw material. In the steel industry, for example, coke is used as a fuel and reducing agent in blast furnaces. The ability to transport coke powder efficiently and safely is critical for maintaining the productivity and safety of these operations. Similarly, in the chemical industry, coke powder is used in the production of carbon black and other chemical products, where consistent material quality is essential.
Other industries that benefit from this technology include the power generation sector, where coke is used as a fuel in power plants, and the metallurgical industry, where coke is used in the production of ferroalloys. The system's ability to handle fine powders and maintain material purity makes it an ideal solution for these applications. Additionally, the dust removal process helps in reducing environmental impact by minimizing dust emissions, which is increasingly important in today's industrial operations.
Conclusion and Company Overview
Dust-removed coke powder pneumatic conveying is a sophisticated and essential technology for handling fine coke powder materials in industrial settings. By incorporating efficient dust removal mechanisms and controlled air flow, the system ensures safe, efficient, and reliable transport of the material. The design principles and components work together to address the unique challenges of coke powder handling, making it a preferred choice in various industries.
Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the specific needs of clients. With a focus on safety, efficiency, and quality, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to meet the highest standards of performance and compliance, ensuring that clients can operate their facilities with confidence and minimal risk. The company's commitment to innovation and customer satisfaction has made it a key player in the development and application of dust-removed coke powder pneumatic conveying technology.




