Principles and Application Characteristics of Dry Coffee Powder Conveying Systems
Release time:2026-09-19 05:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dry coffee powder conveying systems. These systems are engineered to efficiently handle the unique challenges of transporting coffee powders, ensuring minimal product degradation and maintaining consistent quality throughout the process.
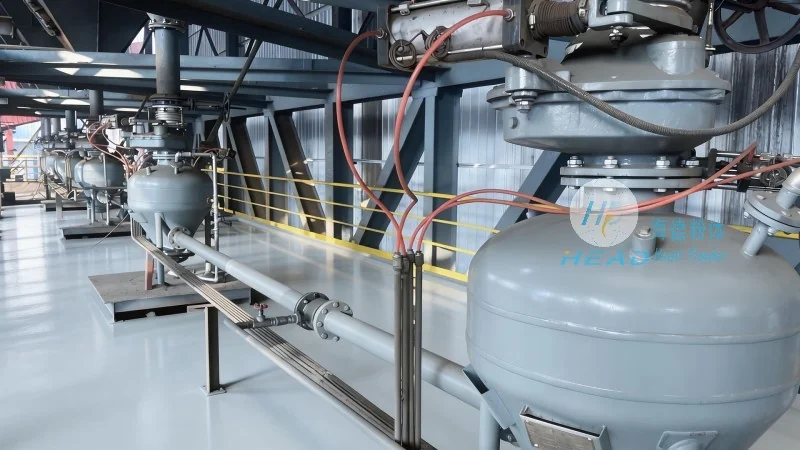
Understanding the Core Principles of Dry Coffee Powder Conveying Lines
The fundamental principle behind dry coffee powder conveying lines lies in the use of specialized equipment that can handle the delicate nature of coffee powders without causing agglomeration or excessive friction. Key components typically include high-efficiency screw conveyors, pneumatic conveying systems, and dust collection units. These components work in tandem to ensure that coffee powders are moved smoothly from storage to processing areas, while maintaining the product's integrity. The design of these systems often incorporates features such as low-speed operation to prevent particle breakdown and the use of non-stick materials to avoid product buildup on surfaces. This approach not only enhances the efficiency of the conveying process but also extends the lifespan of the equipment by reducing maintenance needs.
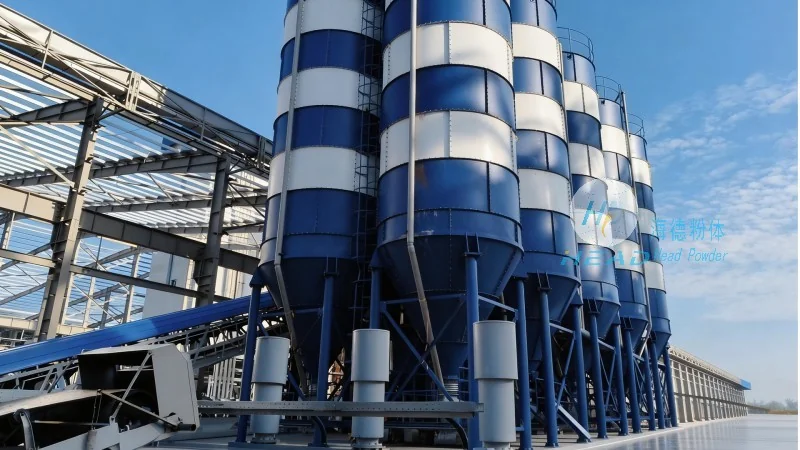
Key Working Scenario Features of Dry Coffee Powder Conveying Systems
Dry coffee powder conveying systems are widely used in various operational scenarios within the coffee processing industry. For instance, in large-scale coffee roasting facilities, these systems are essential for transferring freshly roasted coffee beans into grinding machines, where they are converted into fine powders. The conveying lines are designed to handle the high volume of coffee powders produced during peak production periods, ensuring a continuous and uninterrupted workflow. In addition, these systems are commonly employed in coffee blending operations, where different types of coffee powders are mixed to create customized blends for various markets. The ability to precisely control the flow rate and direction of the coffee powders is crucial in these scenarios, as it directly impacts the final product's flavor profile and consistency. Furthermore, in quality control environments, dry coffee powder conveying systems are used to transport samples for testing, allowing for rapid and accurate analysis of the product's characteristics. This ensures that only high-quality coffee powders are released for further processing or packaging.
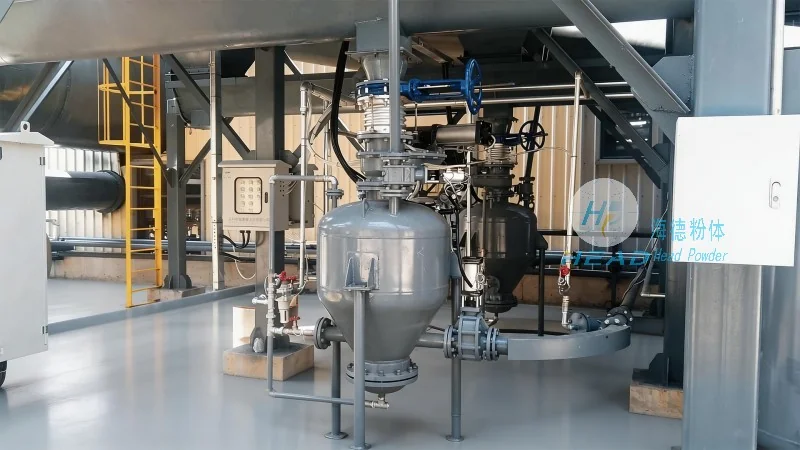
Technical Advantages and Customization Options
HeadPowder's dry coffee powder conveying systems offer several technical advantages that make them suitable for diverse applications. One of the primary benefits is the ability to handle a wide range of coffee powder types, from fine to coarse grinds, without compromising the product's quality. The systems are also designed to be energy-efficient, reducing operational costs for businesses. Additionally, the modular design allows for easy integration with existing production lines, minimizing downtime during installation. Customization is a key feature, as HeadPowder can tailor the conveying systems to meet specific customer requirements, such as varying conveyor lengths, material types, and control systems. This flexibility ensures that clients receive solutions that are perfectly aligned with their operational needs, whether they are in small-scale artisanal coffee production or large-scale commercial operations.




