HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced solutions for quartz stone handling and transportation. The company's expertise lies in designing and implementing efficient pneumatic conveying systems tailored to the unique demands of the quartz stone industry.
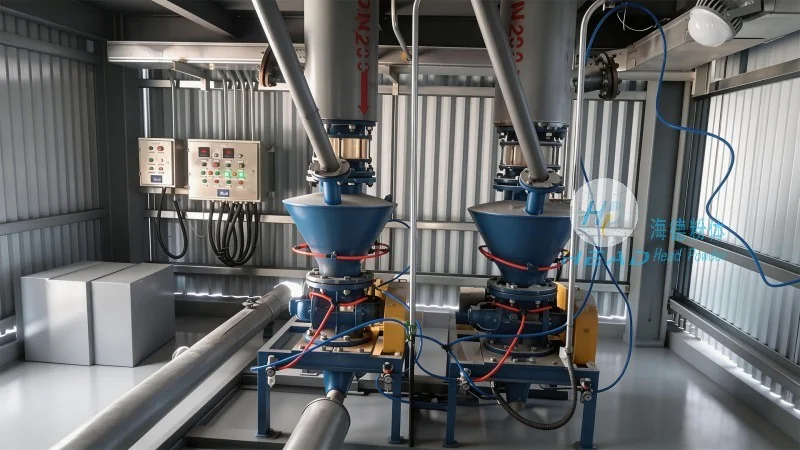
Overview of Quartz Stone Pneumatic Conveying Systems
Quartz stone, a widely used material in construction, manufacturing, and decorative applications, requires reliable and efficient transportation methods to ensure smooth production processes. Pneumatic conveying systems offer a versatile and effective solution for moving quartz stone from storage to processing facilities, reducing the need for manual handling and minimizing material loss. These systems utilize air pressure to transport dry bulk materials like quartz stone through a network of pipes, making them ideal for applications where dust control and material integrity are critical.
Key Features and Benefits of Our Pneumatic Conveying Solutions
Our quartz stone pneumatic conveying systems are engineered with several key features that enhance performance and user experience. Firstly, the system employs high-efficiency air compressors and specialized nozzles to ensure consistent and reliable material transport. This design minimizes the risk of blockages and ensures that quartz stone is conveyed at optimal speeds, reducing downtime and increasing overall productivity. Secondly, the system incorporates advanced filtration and dust collection mechanisms, which not only maintain a clean working environment but also protect the quartz stone from contamination, preserving its quality for downstream applications. Additionally, the modular design of our systems allows for easy integration with existing production lines, enabling seamless upgrades or expansions without significant disruptions to operations. The use of durable materials, such as stainless steel and high-grade plastics, ensures long-term durability and resistance to the abrasive nature of quartz stone, reducing maintenance costs over the system's lifespan.
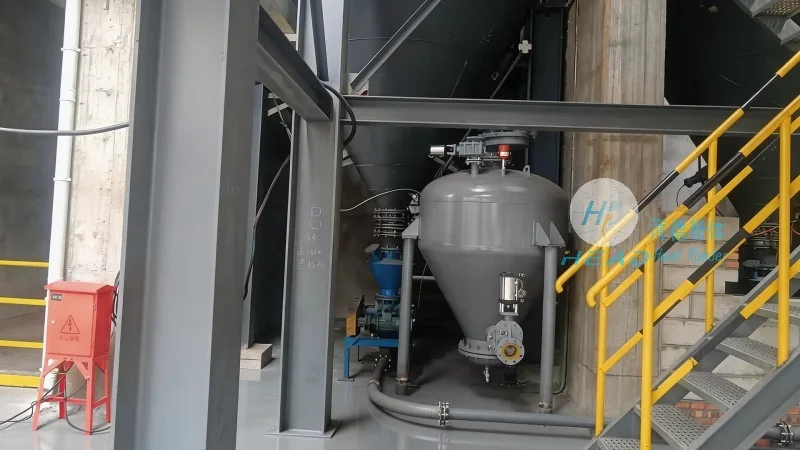
Customization and Application Flexibility
Recognizing that each quartz stone processing facility has unique operational requirements, HeadPowder offers fully customizable pneumatic conveying solutions. Our engineering team works closely with clients to assess their specific needs, including the volume of quartz stone to be transported, the distance between source and destination points, and any environmental or safety constraints. This collaborative approach ensures that the final system is optimized for maximum efficiency and minimal operational costs. The systems can be configured for various conveying modes, including dilute phase and dense phase, allowing flexibility in handling different types of quartz stone, from fine powders to larger aggregates. Furthermore, the integration of automation and control systems enables real-time monitoring and adjustment of the conveying process, enhancing operational control and reducing human error. This level of customization and flexibility makes our pneumatic conveying systems suitable for a wide range of applications, from small-scale production lines to large industrial facilities.
Installation and Maintenance Services
HeadPowder provides comprehensive support throughout the entire lifecycle of our quartz stone pneumatic conveying systems. From initial installation to ongoing maintenance, our team of experienced engineers and technicians ensures that the system operates at peak performance. The installation process is conducted with precision, adhering to industry standards and safety protocols to minimize risks and ensure a smooth setup. Post-installation, we offer regular maintenance services, including routine inspections, component replacements, and performance tuning, to keep the system running efficiently. Our technicians are trained to handle the unique challenges of quartz stone handling, such as dealing with abrasive materials and ensuring proper air pressure management. By offering these services, HeadPowder aims to provide long-term value to our clients, reducing the total cost of ownership and maximizing the return on investment in our pneumatic conveying solutions.
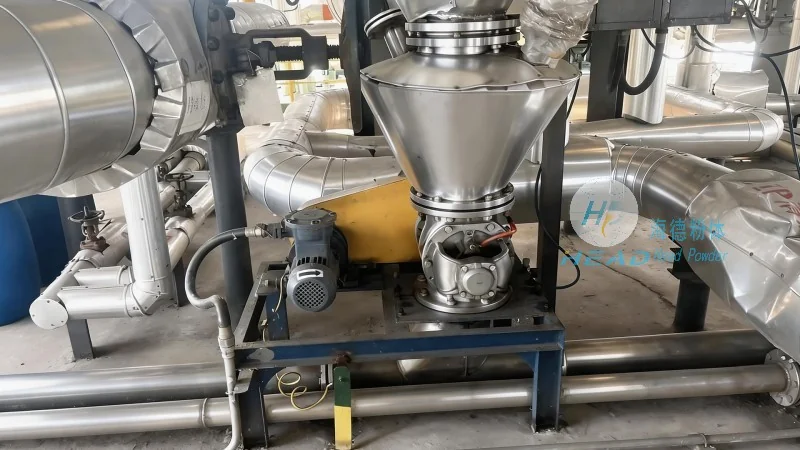
Quality Assurance and Compliance
At HeadPowder, we prioritize quality and compliance in all our engineering solutions. Our quartz stone pneumatic conveying systems are manufactured in accordance with international standards and undergo rigorous testing to ensure they meet the highest performance criteria. The materials used in the construction of the system components are selected for their durability and resistance to corrosion, ensuring that the system can withstand the harsh conditions associated with quartz stone processing. Additionally, our systems are designed to comply with local environmental regulations, incorporating features that minimize dust emissions and noise pollution. This commitment to quality and compliance not only enhances the reliability of our products but also provides our clients with peace of mind, knowing that they are investing in a solution that meets both operational and regulatory requirements.
Conclusion
HeadPowder Engineering Co., Ltd. offers a comprehensive range of quartz stone pneumatic conveying systems that are designed to meet the diverse needs of the quartz stone industry. By combining advanced engineering, customization capabilities, and comprehensive support services, we provide our clients with reliable and efficient solutions for their material handling challenges. Our commitment to quality, durability, and customer satisfaction ensures that our pneumatic conveying systems are not only effective but also a long-term investment in the productivity and success of their operations. With a strong presence in Shandong, China, HeadPowder continues to be a trusted partner for businesses seeking to optimize their quartz stone processing and transportation processes.




