Efficient and clean material handling is a critical requirement in modern industrial operations, particularly in sectors where dust control and product purity are paramount. The dust-free pneumatic conveying system represents a sophisticated solution designed to meet these stringent demands, offering a reliable method for transporting bulk materials while maintaining a contamination-free environment. This article explores the fundamental principles behind such systems and highlights key application scenarios where their implementation delivers significant advantages.
Understanding the Core Principles of Dust-Free Pneumatic Conveying
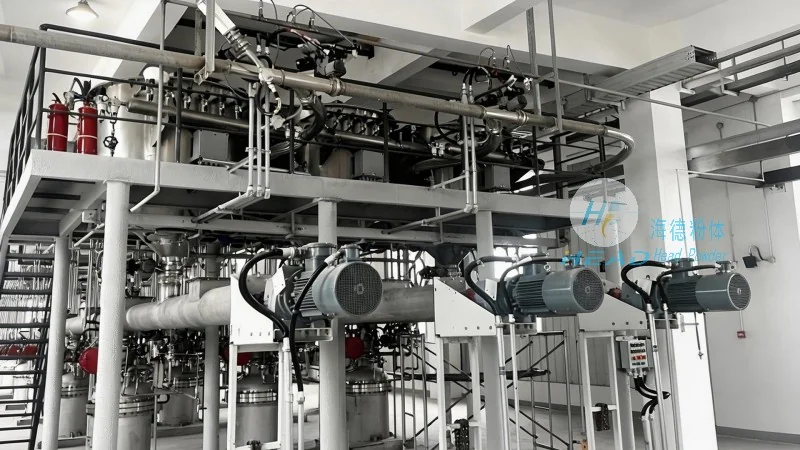
The dust-free pneumatic conveying system operates on the principle of using compressed air or other gases to transport solid materials through a closed pipeline system. Unlike traditional pneumatic conveying methods that may generate dust and particles, this advanced system incorporates specialized components and design features to minimize or eliminate dust emissions. The primary mechanism involves the creation of a low-pressure or high-pressure air stream within the pipeline, which draws or pushes the material particles along the conveying line. Key components typically include a feeding device, a conveying line, a separation unit, and a discharge mechanism. The feeding device ensures the material is introduced into the system in a controlled manner, while the separation unit, often equipped with filters or cyclones, separates the conveyed material from the air stream, ensuring that only clean material is discharged and that the air is filtered to prevent dust release. The entire system is designed to operate under negative pressure or positive pressure conditions, depending on the specific application requirements, to maintain the integrity of the material and the cleanliness of the environment.
Key Application Scenarios and Operational Advantages
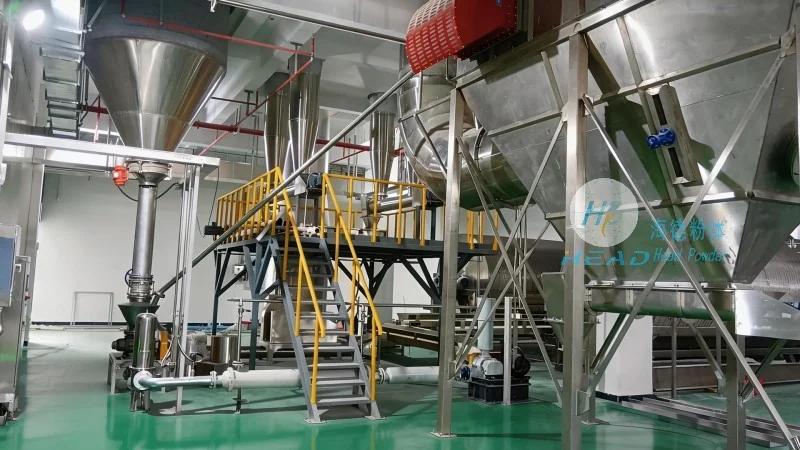
Dust-free pneumatic conveying systems find extensive application across various industries, including pharmaceuticals, food processing, chemical manufacturing, and electronics. In the pharmaceutical industry, for instance, the system is crucial for transporting active pharmaceutical ingredients (APIs) and other sensitive materials where contamination control is non-negotiable. The ability to maintain a sterile and dust-free environment during material transfer ensures product quality and compliance with regulatory standards. Similarly, in the food industry, systems are used to handle powders and granules, such as flour, sugar, and spices, where maintaining product purity and preventing cross-contamination is essential for consumer safety and brand reputation. The chemical industry benefits from these systems when handling hazardous or reactive powders, as they provide a safe and enclosed method of material transport that minimizes exposure risks to operators and the environment. In the electronics sector, dust-free conveying is vital for transporting sensitive components and powders used in the manufacturing of semiconductors and other precision devices, where even minute dust particles can cause defects in the final product.
Operational Efficiency and Environmental Benefits
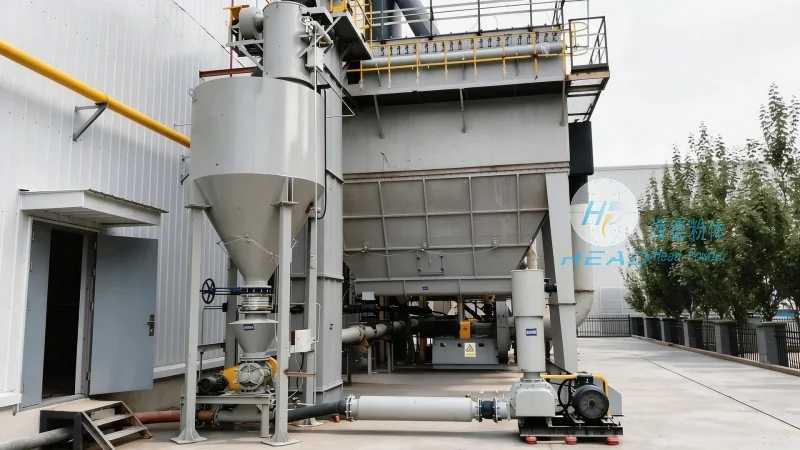
One of the most significant advantages of dust-free pneumatic conveying systems is their ability to enhance operational efficiency while reducing environmental impact. By eliminating the need for manual handling or open-air transport, these systems reduce the risk of material spillage and contamination, leading to lower waste and rework costs. The enclosed pipeline design also minimizes dust emissions, contributing to a cleaner working environment and compliance with environmental regulations. Furthermore, the system's ability to handle a wide range of materials, from fine powders to bulk granules, makes it a versatile solution for diverse industrial needs. The energy efficiency of modern systems, often incorporating advanced control technologies, helps reduce operational costs and lower the carbon footprint of material handling processes. In addition, the reduced need for cleaning and maintenance due to the enclosed design contributes to overall operational savings and increased system reliability.
About Shandong HeadPowder Engineering Co., Ltd.
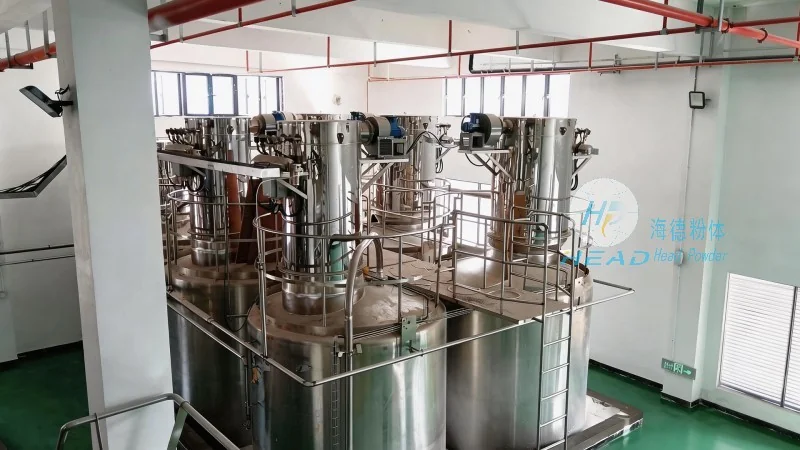
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced material handling solutions, including dust-free pneumatic conveying systems. With headquarters in Shandong, China, the company specializes in designing, manufacturing, and implementing customized solutions tailored to the specific needs of various industries. HeadPowder's expertise lies in integrating cutting-edge technology with robust engineering to deliver systems that meet the highest standards of efficiency, reliability, and environmental compliance. The company's commitment to innovation and customer satisfaction has established it as a trusted partner for businesses seeking to optimize their material handling processes while maintaining stringent quality and safety requirements. Through continuous research and development, HeadPowder ensures that its products remain at the forefront of industrial technology, providing clients with sustainable and effective solutions for their material transport challenges.




