Understanding the fundamentals of dry slurry powder conveying is crucial for industries that rely on efficient material handling. This technology involves the transport of dry powders and fine particles through a pressurized system, often using air or gas as the conveying medium. The process is distinct from traditional wet slurry transport, as it focuses on maintaining the dry state of the material throughout the conveying process. By leveraging advanced engineering principles, dry slurry powder conveying systems can achieve high efficiency, low maintenance, and minimal material degradation.
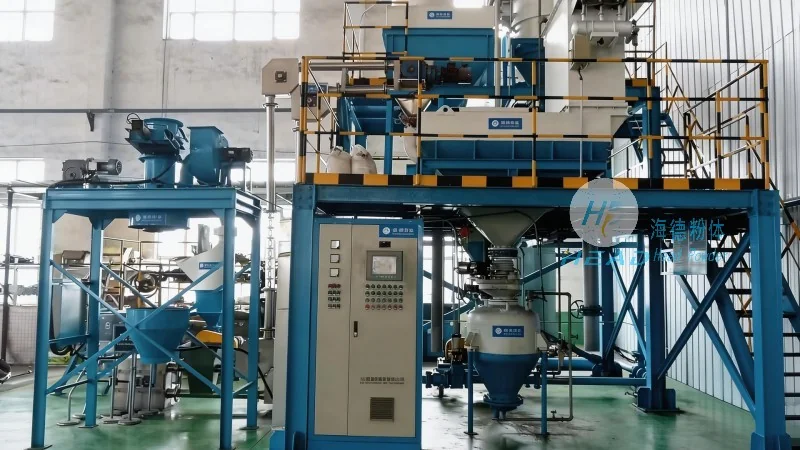
Design Principles of Dry Slurry Powder Conveying Systems
The design of a dry slurry powder conveying system is governed by several critical principles that ensure optimal performance and reliability. First, the system must maintain a consistent pressure and flow rate to prevent material clogging or degradation. This is achieved through the use of specialized pumps, such as rotary lobe or positive displacement pumps, which are capable of handling dry powders without causing excessive wear. The choice of pipeline material is also paramount; materials like stainless steel, PTFE, or high-density polyethylene are commonly used to prevent corrosion and ensure the integrity of the conveyed material. Additionally, the system incorporates effective sealing mechanisms to minimize air leakage and maintain the dry environment, which is essential for preserving the quality of the powder. The design also considers the particle size distribution and moisture content of the material, as these factors directly impact the conveying efficiency and system performance. Proper sizing of the pipelines and components, along with the implementation of filtration and cleaning systems, further enhances the longevity and effectiveness of the conveying process.
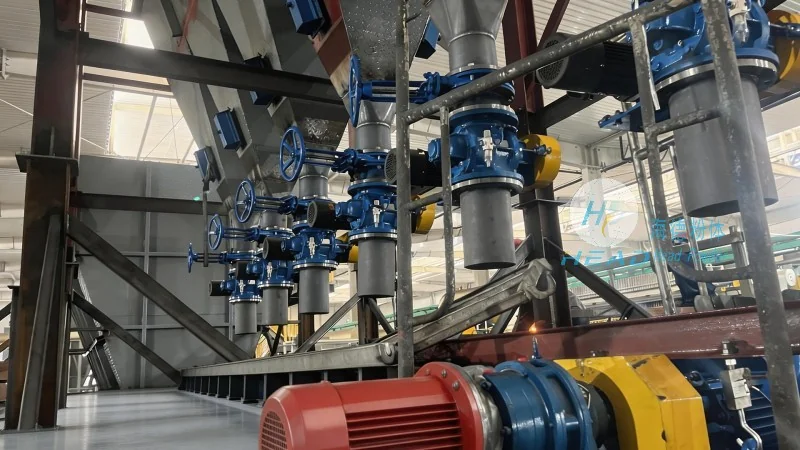
Key Components in Dry Slurry Powder Conveying Systems
Several key components work in tandem to enable the smooth operation of dry slurry powder conveying systems. The primary component is the conveying pump, which generates the necessary pressure to move the powder through the system. These pumps are designed to handle dry powders without the need for liquid additives, ensuring that the material remains in its dry state. The pipeline network, which connects the pump to the discharge point, is another critical element. The diameter and length of the pipelines are carefully calculated to maintain the required pressure drop and flow rate. Valves, including check valves and control valves, are integrated into the system to regulate the flow and prevent backflow. Additionally, the system may include filters and cyclones to separate any fine particles or contaminants from the powder stream, ensuring that the material delivered is of high quality. The control system, which monitors pressure, flow, and temperature, provides real-time feedback to adjust the operation of the pump and other components, ensuring optimal performance. Each component is selected based on the specific characteristics of the powder being conveyed, such as its abrasiveness, moisture content, and particle size, to maximize efficiency and minimize downtime.
Applications and Industries Benefiting from This Technology
Dry slurry powder conveying technology finds extensive applications across various industries, where the efficient and reliable transport of dry powders is essential. In the chemical industry, this technology is used to transport raw materials like calcium carbonate, talc, and other fine chemicals to production lines. The pharmaceutical industry also relies on dry slurry powder conveying for the handling of active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are transferred without contamination or degradation. The mining and mineral processing sector utilizes this technology to transport ore powders from processing plants to storage facilities or for further processing. In the food and beverage industry, dry slurry powder conveying is employed to handle ingredients like flour, sugar, and spices, maintaining the quality and freshness of the products. Additionally, the agricultural sector benefits from this technology for the transport of fertilizers and other dry agricultural products. The versatility of dry slurry powder conveying makes it suitable for a wide range of applications, where traditional methods may be less effective or inefficient.
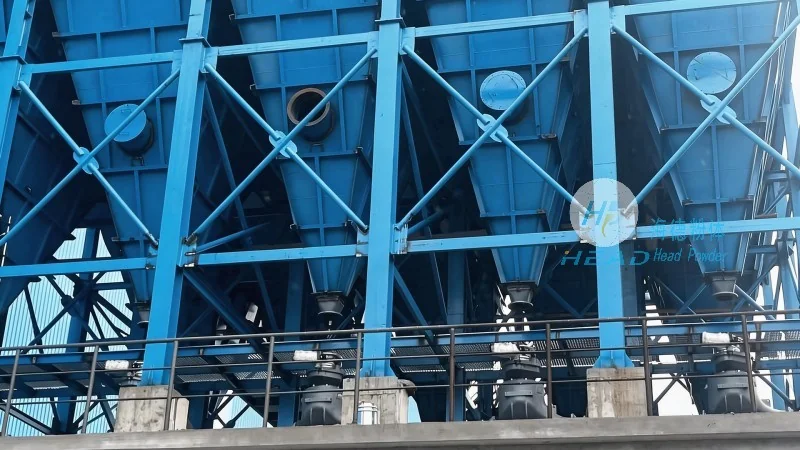
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of dry slurry powder conveying solutions. With its headquarters located in Shandong, China, the company specializes in designing, manufacturing, and installing advanced conveying systems tailored to the specific needs of various industries. HeadPowder's expertise lies in the integration of cutting-edge technology with practical engineering solutions, ensuring that their systems deliver high performance, reliability, and cost-effectiveness. The company's team of experienced engineers and technicians work closely with clients to understand their material handling challenges and develop customized solutions that meet their operational requirements. HeadPowder's commitment to quality and innovation has made it a trusted partner for businesses seeking efficient and sustainable dry slurry powder conveying systems. By leveraging its extensive knowledge and state-of-the-art equipment, HeadPowder continues to set industry standards in the field of material handling technology.




