Magnesite, a vital industrial material utilized in refractory production and high-temperature applications, demands efficient material handling solutions. The magnesite pneumatic conveying system is a specialized technology that transports magnesite powder or granules through a closed pipeline using compressed air or other gas as the conveying medium. This system offers significant advantages over traditional mechanical conveying methods, including reduced dust generation, enhanced safety, and improved process control. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of such systems, leveraging decades of industry experience to deliver optimal solutions for clients worldwide.
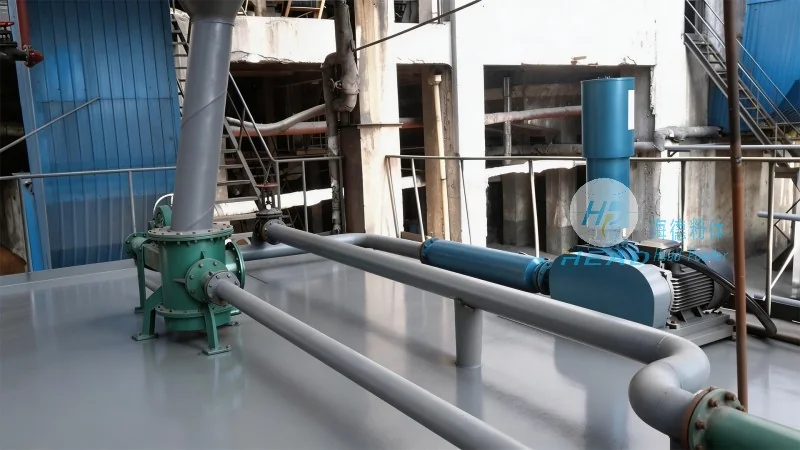
Key Components and Working Principle
The magnesite pneumatic conveying system comprises several critical components that operate in unison to achieve efficient material transport. The primary components include a material feeder, which ensures a consistent and controlled flow of magnesite into the system; a conveying pipeline, typically constructed from corrosion-resistant materials like stainless steel or specialized alloys to withstand magnesite's chemical properties; a separation and collection system, which separates the material from the conveying air and collects it in a designated container; and a gas source, which provides the necessary pressure and flow rate for the conveying process. The working principle involves feeding magnesite into the feeder, where it is introduced into the pipeline alongside compressed air. The air-magnesite mixture travels through the pipeline, and at the receiving end, the material is separated from the air using a cyclone or other separation device. The separated magnesite is then collected, while the air is either filtered and recirculated or vented to the atmosphere, depending on the system design. This process minimizes material loss and ensures a clean, efficient operation.
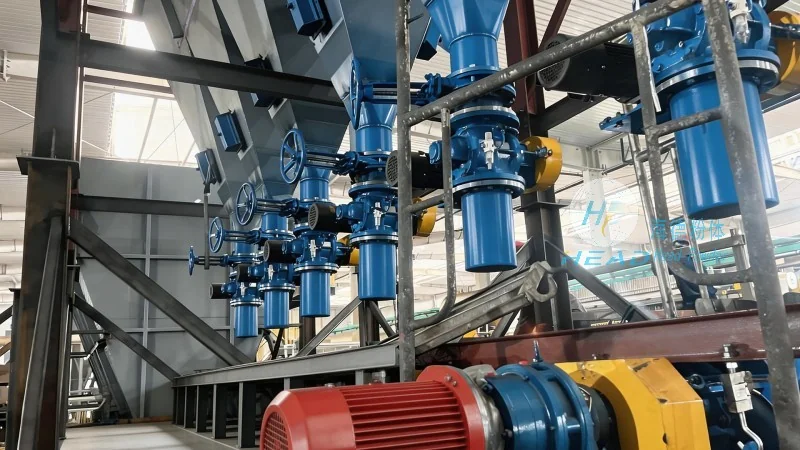
Material Handling Efficiency and Process Integration
Efficiency is a core aspect of magnesite pneumatic conveying systems, as they are engineered to handle high volumes of material with minimal downtime and maintenance. The system's ability to integrate seamlessly with existing industrial processes is another key advantage. For example, in a refractory manufacturing plant, magnesite can be conveyed directly from storage silos to mixing or processing equipment, eliminating the need for manual handling or intermediate storage. This integration not only improves operational efficiency but also reduces the risk of material contamination and dust exposure. The system's flexibility allows for customization to fit various process requirements, including different material flow rates, pipeline lengths, and environmental conditions. By optimizing conveying parameters such as air velocity and pressure, the system can achieve the desired material throughput while minimizing energy consumption and wear on components.
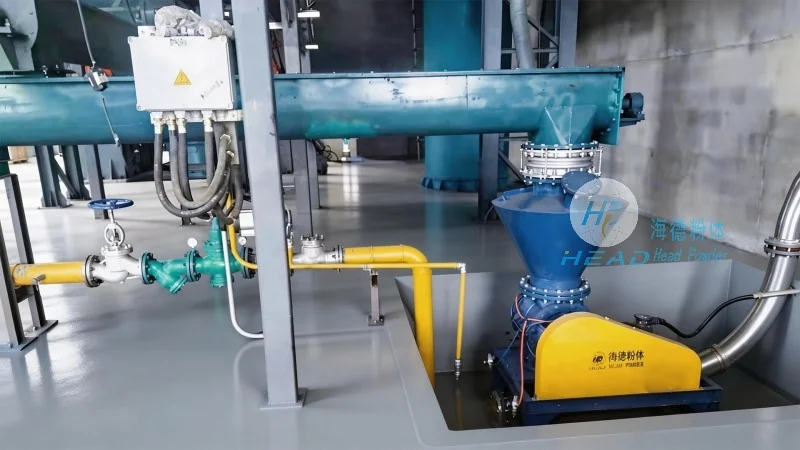
Technical Advantages and Performance Characteristics
Compared to traditional mechanical conveying methods, magnesite pneumatic conveying systems offer several technical advantages that make them preferable for many applications. One of the most significant benefits is the reduction in dust generation, which is critical for maintaining a safe and healthy working environment. The closed pipeline design prevents dust from escaping into the air, reducing the risk of respiratory issues and environmental contamination. Additionally, the system provides better control over material flow, allowing for precise dosing and consistent product quality. This is particularly important in industries where uniform material properties are essential, such as in the production of high-quality refractory products. The system also offers advantages in terms of space utilization, as the conveying pipeline can be installed vertically or horizontally, optimizing the use of available floor space. Furthermore, the system's ability to handle abrasive materials like magnesite without excessive wear on components is a key performance characteristic. The use of high-quality materials for the pipeline and components ensures long service life and minimal maintenance requirements, contributing to overall cost savings.
Application Scenarios and Industry Use Cases
Magnesite pneumatic conveying systems are widely used in various industries where magnesite is a critical raw material. In the refractory industry, these systems are commonly employed to transport magnesite from storage to mixing and molding equipment, ensuring a consistent supply of material for the production of refractory bricks, linings, and other products. The system's ability to handle large volumes of material efficiently makes it ideal for high-throughput manufacturing facilities. In the chemical industry, magnesite is used as a raw material for the production of magnesium compounds, and pneumatic conveying systems facilitate the transport of these materials between processing stages. The system's flexibility also makes it suitable for use in research and development laboratories, where precise material handling is required for experimental work. Additionally, in the construction industry, magnesite-based materials are used for insulation and other applications, and pneumatic conveying systems can be used to transport these materials to job sites. The adaptability of the system to different industries and applications highlights its versatility and importance in modern industrial operations.
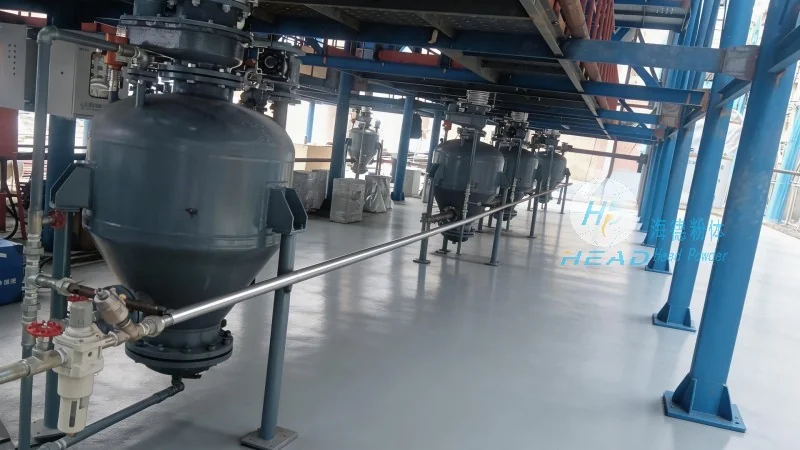
Conclusion and Company Overview
In conclusion, the magnesite pneumatic conveying system is a highly efficient and reliable technology for handling magnesite in industrial applications. Its ability to minimize dust, improve safety, and enhance process control makes it a preferred choice over traditional mechanical conveying methods. Shandong HeadPowder Engineering Co., Ltd. has established itself as a leading provider of such systems, leveraging advanced engineering and manufacturing capabilities to deliver customized solutions that meet the specific needs of clients. With a focus on quality, innovation, and customer satisfaction, the company continues to play a vital role in the industrial material handling sector, helping businesses optimize their operations and achieve greater productivity. Based in Shandong, China, HeadPowder Engineering Co., Ltd. serves clients globally, providing comprehensive support from system design and installation to maintenance and after-sales service. The company's commitment to excellence and its deep understanding of industrial processes ensure that clients receive the best possible solutions for their magnesite conveying needs.




