For companies in the fine chemical industry, the efficient and safe transportation of powders is a critical operational challenge. Pneumatic conveying equipment has emerged as a key solution, offering a reliable method to move fine powders with precision and minimal contamination. This article explores the fundamental principles behind such equipment and highlights the specific application scenarios where they excel, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
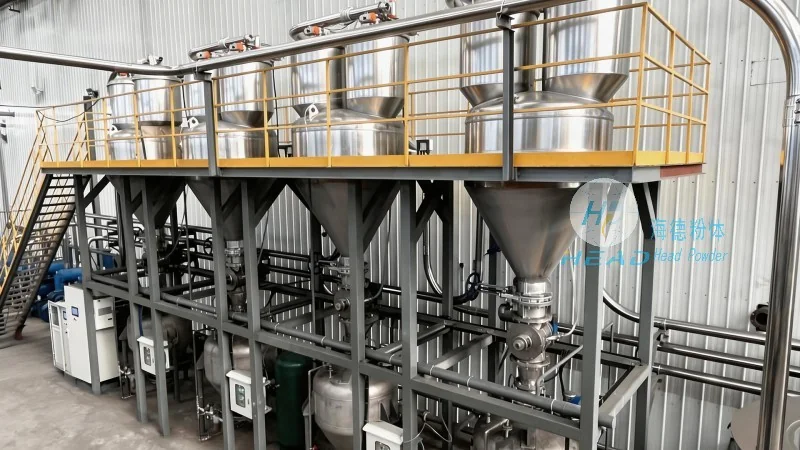
Principles of Pneumatic Conveying for Fine Chemical Powders
Pneumatic conveying systems operate by transporting solid particles through a pipeline using a gas stream, typically air or other inert gases. The core principle involves creating a pressure differential to move the material. There are two primary types of pneumatic conveying: positive pressure and negative pressure systems. Positive pressure systems generate air pressure at the conveying point, pushing the powder through the pipeline. This method is often used for long-distance or high-volume applications and is particularly effective for handling fine powders that are prone to caking or agglomeration. Negative pressure systems, on the other hand, create a vacuum at the receiving end, drawing the powder into the pipeline. This approach is suitable for applications requiring a clean environment or when the material is sensitive to air exposure.
For fine chemical powders, which often have specific handling requirements due to their size, density, and reactivity, the choice of system depends on factors such as particle size distribution, moisture content, and the desired level of product integrity. Advanced systems may incorporate features like pulse-jet technology or rotary valves to ensure consistent flow and prevent blockages. These technologies help maintain the quality of the powder by minimizing particle degradation and preventing contamination from external sources.
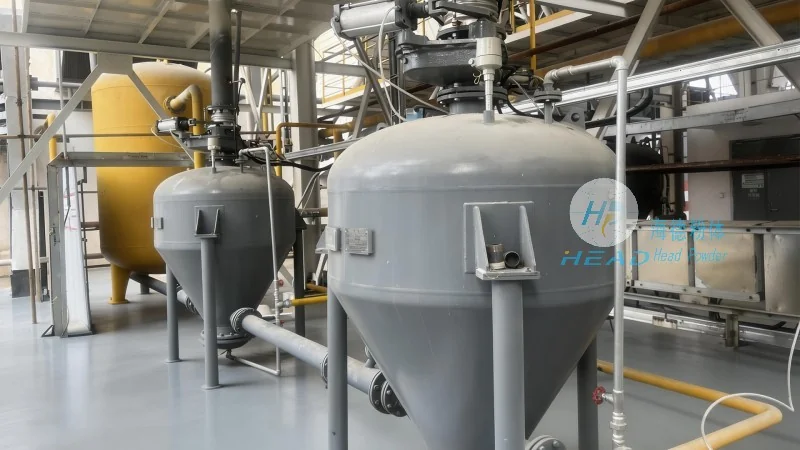
Key Working Characteristics and Advantages
The working characteristics of pneumatic conveying equipment for fine chemicals are designed to address the unique challenges of this industry. One of the most significant advantages is the ability to handle powders with high precision, ensuring that the material is transported without segregation or loss of quality. This is crucial for products where uniformity is essential, such as pharmaceuticals or specialty chemicals. Additionally, pneumatic systems offer a closed-loop operation, which enhances safety by preventing dust emissions and protecting both the product and the environment from contamination. The equipment is also highly flexible, allowing for integration into existing production lines and adapting to varying throughput demands.
Application Scenarios in the Fine Chemical Industry
Pneumatic conveying equipment is widely used in various stages of the fine chemical production process. In the raw material handling phase, it efficiently transports raw powders from storage silos to processing units, ensuring a continuous supply without manual intervention. During the manufacturing process, the equipment can be employed to move intermediate products between reactors and storage tanks, maintaining the integrity of the material. Finally, in the packaging stage, pneumatic systems are used to transfer finished products into containers, reducing the risk of product damage and ensuring accurate dosing.
Specific industries that benefit from this technology include pharmaceuticals, where the strictest standards for product purity and safety are required. The equipment is also essential in specialty chemicals, such as pigments, catalysts, and food additives, where the consistency of the final product directly impacts its performance. Furthermore, in the chemical processing sector, where powders are often used as catalysts or reagents, the ability to handle these materials with minimal loss or degradation is critical for maintaining process efficiency and product quality.
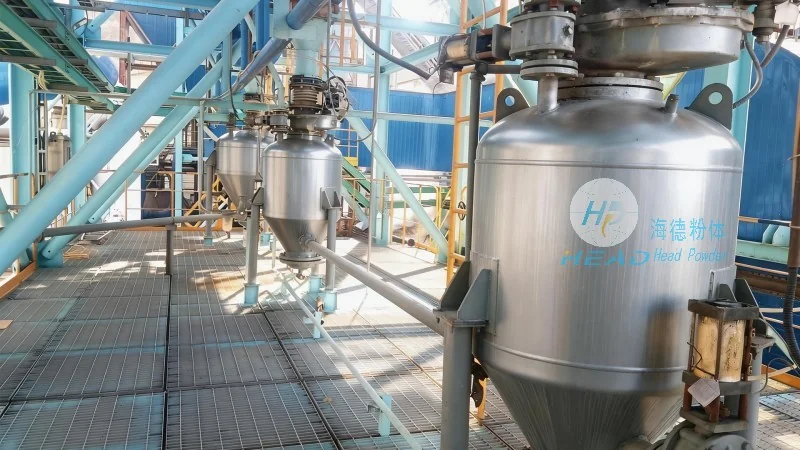
Role of Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer of pneumatic conveying equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized solutions tailored to the unique needs of the fine chemical industry. The company’s expertise lies in designing systems that meet the stringent requirements for product purity, safety, and efficiency. By leveraging advanced engineering and materials science, HeadPowder develops equipment that is robust, reliable, and easy to maintain. Their products are designed to handle a wide range of fine powders, from pharmaceutical actives to specialty pigments, ensuring that clients can achieve optimal performance in their operations.
HeadPowder’s commitment to quality is evident in their manufacturing processes, which adhere to international standards and are continuously improved through research and development. The company’s team of engineers works closely with clients to understand their specific challenges and develop solutions that enhance productivity and reduce operational costs. With a strong presence in China, particularly in Shandong, HeadPowder serves a global market, providing equipment that is trusted by industries worldwide for its performance and reliability.




