For companies in the cereal industry, efficient and reliable material handling is crucial to maintaining production flow and product quality. Pneumatic conveying systems offer a solution that meets these demands by transporting cereal powders and granules with precision and minimal contamination. This article explores the principles behind cereal powder pneumatic conveying equipment and highlights the key working scene characteristics that make it an ideal choice for modern food processing operations.
Understanding the Core Principles of Pneumatic Conveying Systems
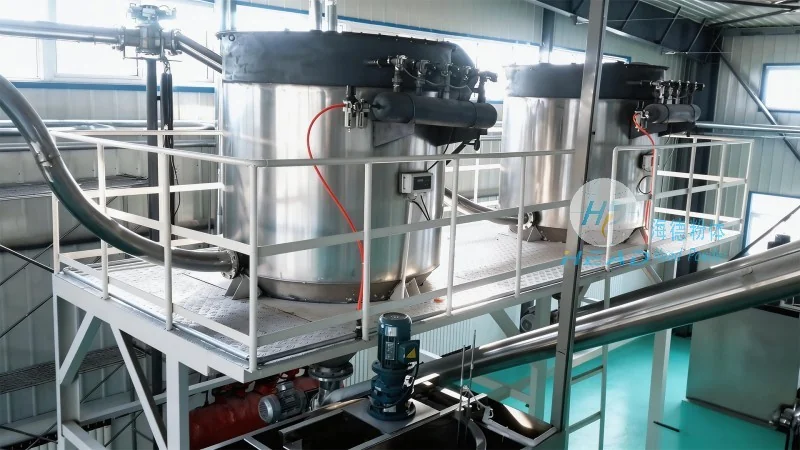
The fundamental principle of pneumatic conveying is the use of air or gas to move bulk materials through a pipeline. In the case of cereal powder applications, this technology involves creating a flow of air that propels the powder particles from a source point to a destination point. The system typically consists of a blower or compressor that generates the necessary air pressure, a hopper or feeder to introduce the material, and a pipeline network that transports the material. The design of the system, including the type of air flow (positive or negative pressure) and the configuration of the pipeline, is tailored to the specific characteristics of the cereal powder, such as particle size, density, and moisture content. This ensures optimal performance and prevents issues like blockages or material degradation.
Key Working Scene Characteristics of Cereal Powder Pneumatic Conveying Equipment
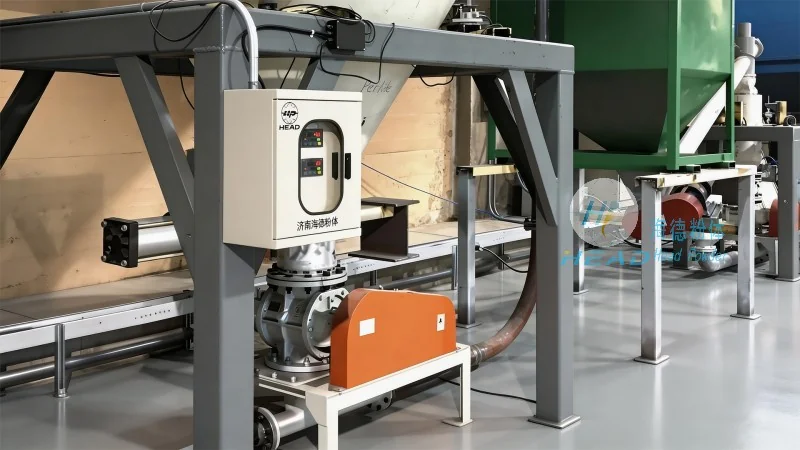
When evaluating pneumatic conveying systems for cereal powder handling, several working scene characteristics are critical to consider. These include the system's ability to handle varying particle sizes and flow rates, its capacity to maintain product integrity, and its integration with existing production lines. For instance, in a large-scale cereal manufacturing facility, the system must be capable of transporting large volumes of powder efficiently while minimizing dust generation and product loss. The working scene also involves the system's adaptability to different processing stages, such as from raw material storage to packaging. Additionally, the equipment's durability and ease of maintenance are important factors, as they directly impact operational costs and downtime. The working scene characteristics of a pneumatic conveying system for cereal powders are therefore a balance between technical performance and practical application in real-world food processing environments.
Applications and Benefits in Cereal Processing
Pneumatic conveying equipment is widely used in various stages of cereal processing, from raw material handling to finished product packaging. In raw material reception, the system can efficiently transport bulk cereal powders from storage silos or trucks to processing areas, reducing manual handling and associated risks. During the production process, it can convey ingredients like flour, oats, or cornmeal between different processing units, ensuring consistent mixing and blending. At the packaging stage, the system can deliver finished cereal products to packaging machines, maintaining product freshness and preventing contamination. The benefits of using pneumatic conveying for cereal powders include improved hygiene, as the system is enclosed and prevents dust exposure. It also enhances operational efficiency by automating material transport, reducing labor costs, and increasing production throughput. Furthermore, the system's flexibility allows it to be integrated with existing infrastructure, making it a cost-effective solution for upgrading or expanding cereal processing facilities.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
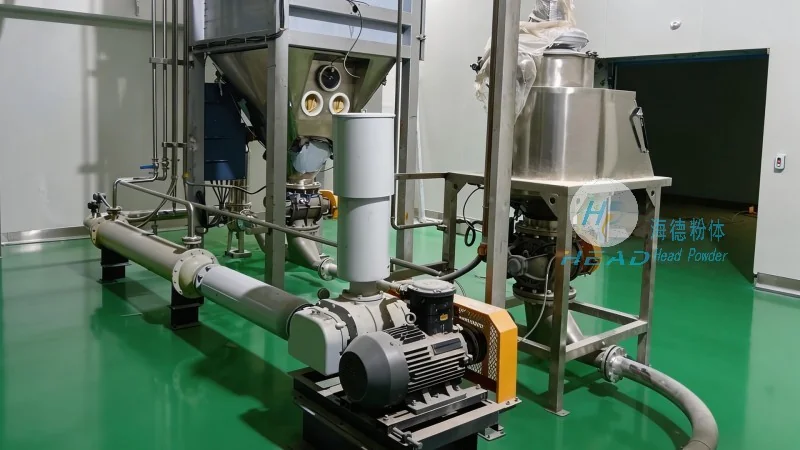
As a leading provider of pneumatic conveying solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing equipment tailored to the unique needs of the cereal industry. With a focus on innovation and quality, the company has developed advanced systems that address the specific challenges of handling cereal powders, such as their light weight and tendency to create dust. The company's expertise lies in understanding the technical requirements of different cereal products and designing systems that ensure reliable, efficient, and safe material transport. Based in Shandong, China, HeadPowder has established a strong reputation for delivering high-performance pneumatic conveying equipment that meets international standards and customer expectations. Their commitment to customer service and technical support ensures that clients receive comprehensive solutions that enhance their production capabilities and product quality.




