Understanding the principle and operational characteristics of lithium carbonate material conveying lines is crucial for optimizing industrial processes in the lithium battery manufacturing sector. These systems are designed to efficiently transport lithium carbonate, a key raw material in lithium-ion battery production, from processing stages to final application points. The following sections explore the technical principles underlying these conveying lines and the specific characteristics of their working environments.
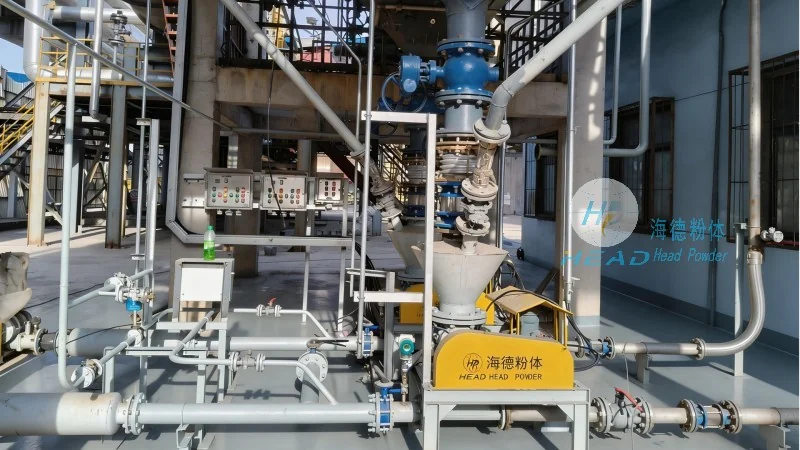
Technical Principles of Lithium Carbonate Material Conveying
The core principle of lithium carbonate material conveying lines revolves around the mechanical transport of bulk materials using specialized equipment. Common components include belt conveyors, bucket elevators, and pneumatic conveyors, each tailored to handle the unique properties of lithium carbonate. For instance, belt conveyors are widely used due to their ability to transport large volumes of material over long distances with minimal maintenance. The design of these systems often incorporates features such as adjustable speed controls, which allow for precise control of material flow rates, and robust sealing mechanisms to prevent dust emissions and material loss. Additionally, the material's tendency to absorb moisture and its fine particle size necessitate the use of equipment with smooth surfaces and effective dust suppression systems to maintain product quality and operational safety.
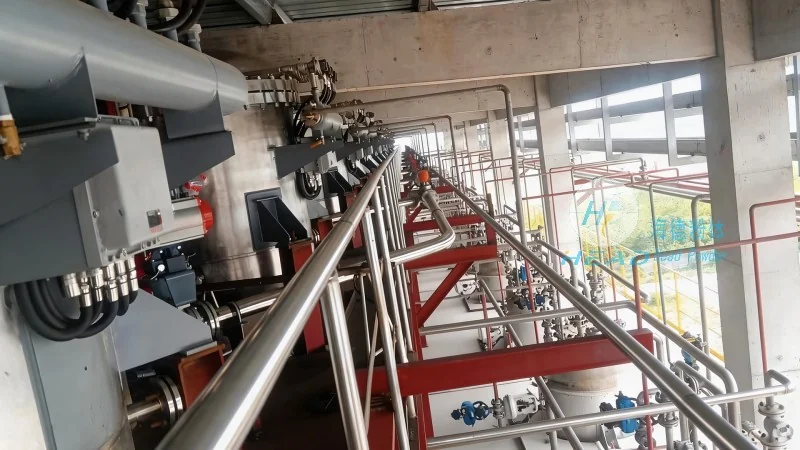
Working Scene Characteristics
The working scene characteristics of lithium carbonate material conveying lines vary significantly based on the industrial application and the scale of operation. In lithium mining and processing facilities, conveying lines are typically integrated into larger production workflows that include crushing, grinding, and screening stages. These systems must handle high volumes of raw material and operate in environments with fluctuating temperatures and humidity levels. The operational characteristics in such settings emphasize durability, reliability, and the ability to withstand harsh conditions. In contrast, conveying lines used within battery manufacturing plants often operate in more controlled environments, focusing on precision and cleanliness to ensure the quality of the final product. These lines may involve automated material handling systems that integrate with other production equipment, such as mixers and extruders, to maintain consistent material flow and reduce human intervention.
Application Scenarios and Operational Features
Application scenarios for lithium carbonate material conveying lines span from primary mining operations to downstream battery production. In mining sites, the conveying lines are responsible for transporting crushed lithium ore to processing plants, where it is converted into lithium carbonate. The equipment used in these scenarios is often heavy-duty and designed to handle abrasive materials and high throughput. In battery manufacturing facilities, the conveying lines play a critical role in moving lithium carbonate from storage silos to production lines, where it is combined with other components like graphite and binders. The operational features in these scenarios include real-time monitoring of material levels and flow rates, as well as automated control systems that adjust conveyor speeds based on production demands. Furthermore, the design of these systems considers factors such as space constraints and integration with existing infrastructure, ensuring seamless operation within the overall production environment.
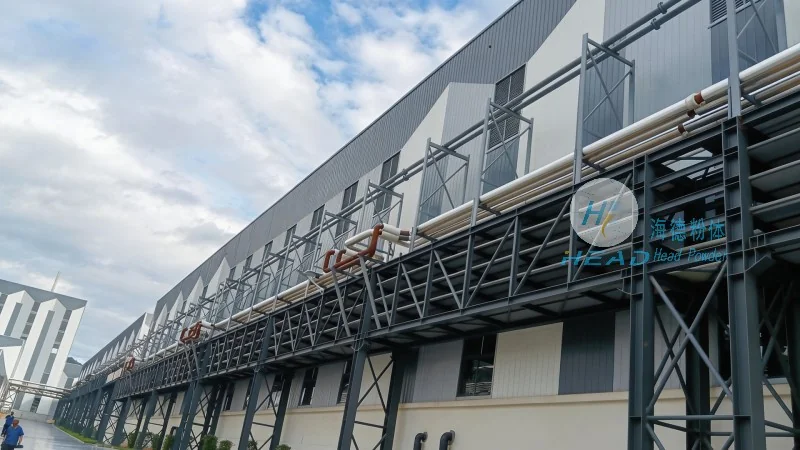
Company Background and Technical Expertise
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of specialized material handling equipment, including lithium carbonate material conveying lines. With headquarters in Shandong, China, the company leverages decades of experience in engineering and manufacturing to deliver high-quality, customized solutions for the lithium industry. Their expertise lies in understanding the unique challenges of handling lithium carbonate, such as its hygroscopic nature and fine particle size, and designing conveying systems that address these challenges effectively. The company's products are known for their durability, efficiency, and compliance with industry standards, making them a trusted choice for businesses operating in the lithium battery sector.




