Compound fertilizer powder conveying systems are critical components in modern agricultural and industrial applications, designed to efficiently transport bulk powder materials such as compound fertilizers. These systems integrate advanced engineering principles to ensure reliable, safe, and efficient material handling. The operation process and working principle of such systems involve multiple stages, from material feeding to final discharge, each optimized for performance and durability.
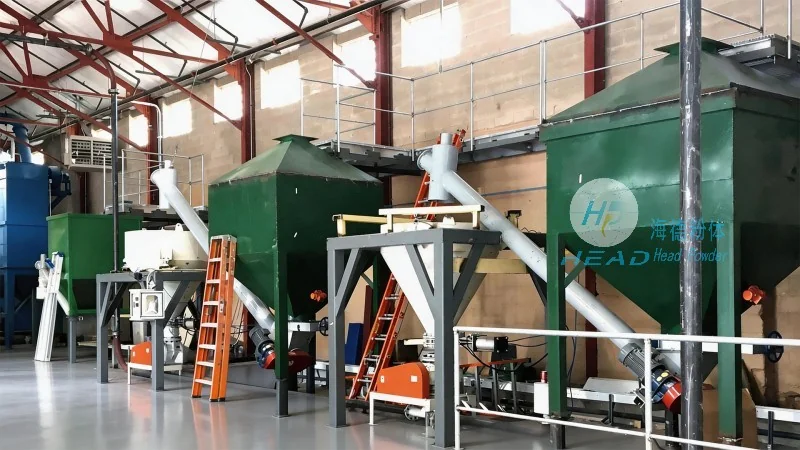
Key Components of the Conveying System
The compound fertilizer powder conveying system typically consists of several core components, including a hopper for material storage, a feeder to control the flow rate, a conveyor mechanism (such as a screw or pneumatic conveyor), and a discharge outlet. Each component plays a vital role in the overall system performance. The hopper is designed to hold a sufficient quantity of fertilizer, ensuring a steady supply to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the material flow, preventing overloading or underflow. The conveyor mechanism then transports the powder to the desired location, while the discharge outlet allows for controlled release of the material.
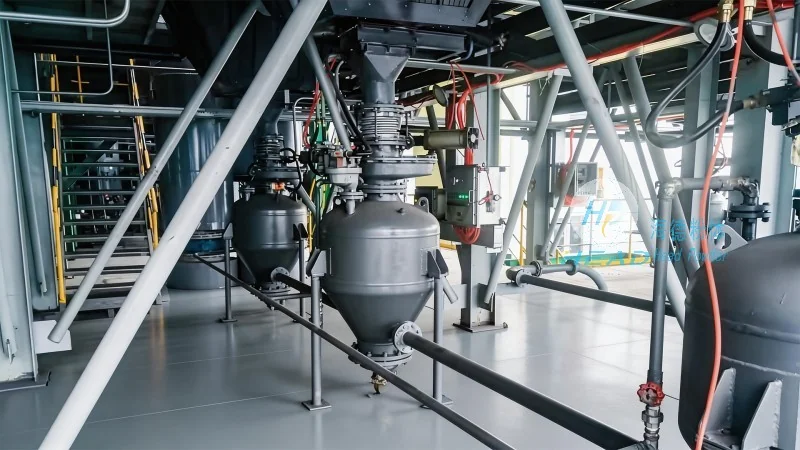
Operation Process of the System
The operation process of a compound fertilizer powder conveying system begins with material loading into the hopper. The material is then transferred to the feeder, where the flow rate is adjusted based on the system's requirements. The feeder ensures a consistent flow of powder to the conveyor. The conveyor mechanism, whether mechanical or pneumatic, moves the fertilizer through the system. For mechanical conveyors, a screw or belt system rotates to push the powder forward. In pneumatic systems, air pressure is used to create a flow, transporting the powder through pipes. The system continues to operate until the material is fully conveyed to the discharge point. During operation, sensors and controls monitor the system's performance, ensuring it operates within safe and efficient parameters.
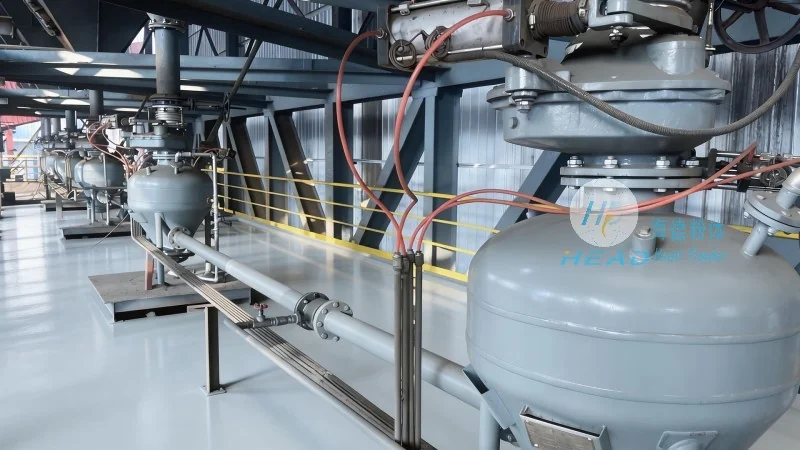
Working Principle of the System
The working principle of a compound fertilizer powder conveying system is based on the principles of fluidization and mechanical transport. In mechanical systems, the conveyor rotates, creating a moving surface that pushes the powder forward. The screw or belt design ensures that the powder is continuously moved without segregation or caking. Pneumatic systems utilize compressed air to create a flow, where the powder is suspended in the air stream and transported through the system. The system's design minimizes friction and material degradation, ensuring the fertilizer remains in its original state. The control system manages the flow rate, pressure, and speed, optimizing the operation for maximum efficiency and minimal energy consumption.
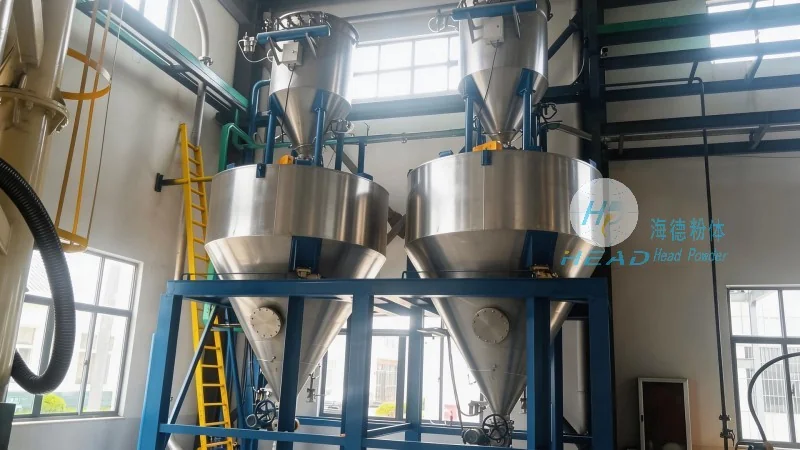
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of compound fertilizer powder conveying systems. With headquarters in Shandong, China, the company specializes in designing and manufacturing high-quality conveying solutions tailored to the agricultural and industrial sectors. headpowder's systems are engineered to meet the demanding requirements of fertilizer handling, ensuring reliability, durability, and efficiency. The company's commitment to innovation and quality has made it a trusted partner for businesses seeking advanced material handling solutions.




