Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional engineering company based in Shandong, China. With a focus on advanced powder handling solutions, the company specializes in the design, manufacturing, and integration of pneumatic conveying systems tailored for the petrochemical industry. HeadPowder leverages decades of industry experience to deliver efficient, reliable, and customized solutions that meet the stringent requirements of modern chemical processing facilities.
Principles of Pneumatic Conveying Technology
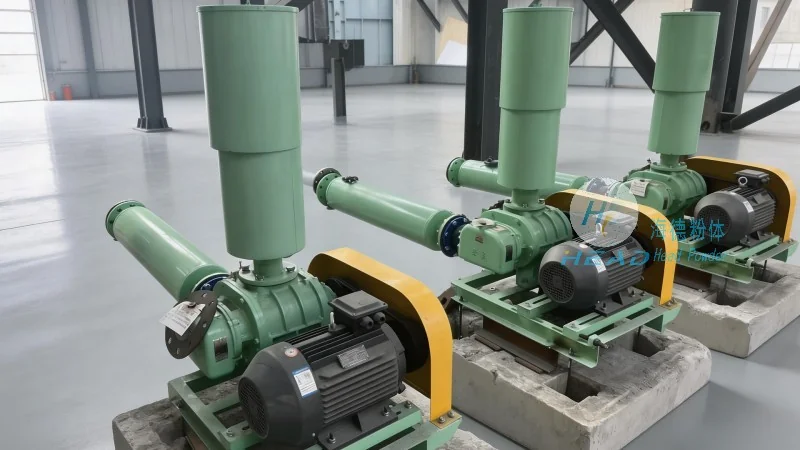
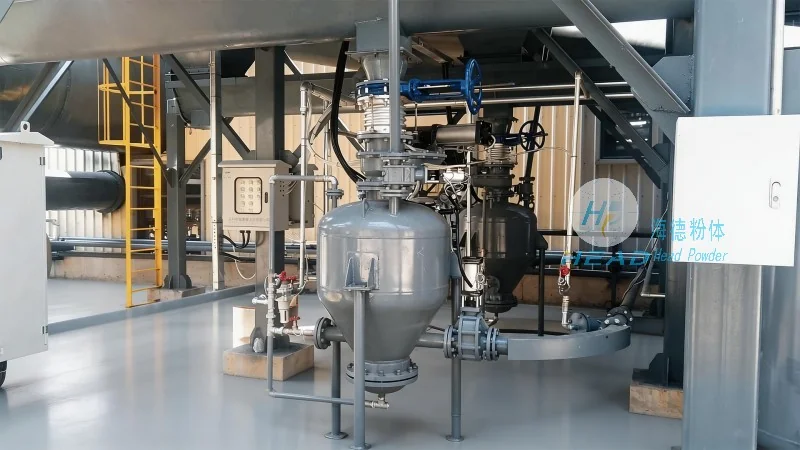
Pneumatic conveying systems operate by transporting bulk powders through a pipeline using compressed air or other gas streams. The core principle involves creating a pressure differential between the conveying line and the ambient environment. In positive pressure systems, air is forced into the pipeline, carrying the powder particles forward. Negative pressure systems, on the other hand, draw air and powder from the source using a vacuum. This fundamental mechanism allows for the safe and efficient movement of powders over long distances, with minimal product degradation and contamination. The technology is particularly effective for handling abrasive, corrosive, or sensitive materials commonly found in petrochemical applications.
Working Scene Characteristics and Applications
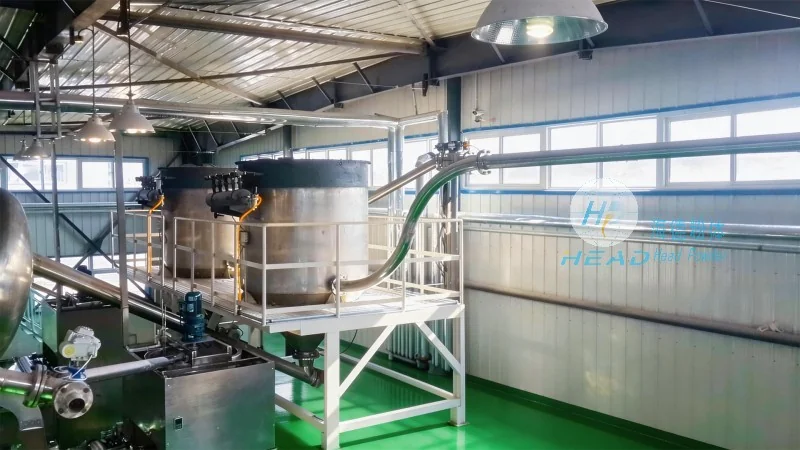
The working scene characteristics of petrochemical powder pneumatic conveying systems are defined by several key factors that influence system design and performance. First, the material properties—such as particle size, density, and flowability—dictate the choice of conveying method (e.g., dilute phase vs. dense phase). For example, fine powders with low bulk density are typically conveyed in dilute phase systems, where the powder is suspended in the air stream, while cohesive or high-density materials may require dense phase systems, where the powder moves in a slurry-like state. Second, the operational environment, including temperature and pressure conditions, must be considered. Petrochemical plants often operate under high temperatures and pressures, requiring systems with robust materials of construction and thermal resistance. Third, the system's integration with existing plant infrastructure is critical. HeadPowder designs systems that can seamlessly connect to existing pipelines, storage silos, and processing equipment, minimizing downtime and installation complexity. Additionally, the need for dust control and environmental compliance is paramount in petrochemical facilities, making advanced filtration and containment systems integral to the design. Typical applications include the transport of catalysts, chemicals, and raw materials between reactors, storage tanks, and processing units within petrochemical plants.
Technical Advantages and Practical Implementation
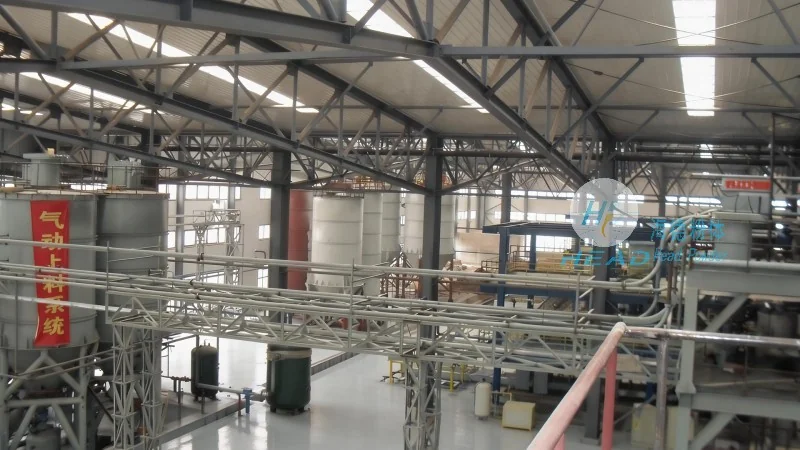
HeadPowder's pneumatic conveying systems offer several technical advantages that enhance operational efficiency and reliability. One key benefit is the ability to handle a wide range of powder types, from fine chemicals to bulk raw materials, without the need for additional processing steps like screening or drying. The systems also provide superior product protection, as the enclosed pipeline prevents exposure to moisture, air, or contaminants, preserving the material's quality and shelf life. Furthermore, the technology enables flexible and scalable solutions, allowing plants to adapt to changing production demands by adjusting the conveying capacity or adding additional lines. From small-scale laboratory applications to large industrial facilities, HeadPowder's systems are engineered to meet diverse needs with consistent performance. The company's expertise in system optimization ensures that energy consumption is minimized, contributing to cost savings and environmental sustainability. By leveraging advanced control systems and monitoring technologies, HeadPowder's solutions provide real-time data on system performance, enabling proactive maintenance and reducing downtime. The systems are also designed for easy maintenance, with accessible components and modular designs that facilitate repairs and upgrades without extensive plant shutdowns.




