In industrial settings where bulk material handling is a daily operation, the tonne bag unloading material conveying system stands out as a vital technology for optimizing workflow and enhancing operational efficiency. This system is specifically engineered to facilitate the seamless transfer of materials from large flexible containers, commonly referred to as tonne bags or super sacks, into processing or storage systems. By integrating advanced mechanical and sometimes pneumatic components, the system ensures that material is discharged quickly, safely, and with minimal human intervention. The following sections will delve into the core principles governing this technology and explore the diverse working environments where it is most effectively applied.
System Overview: Components and Functionality
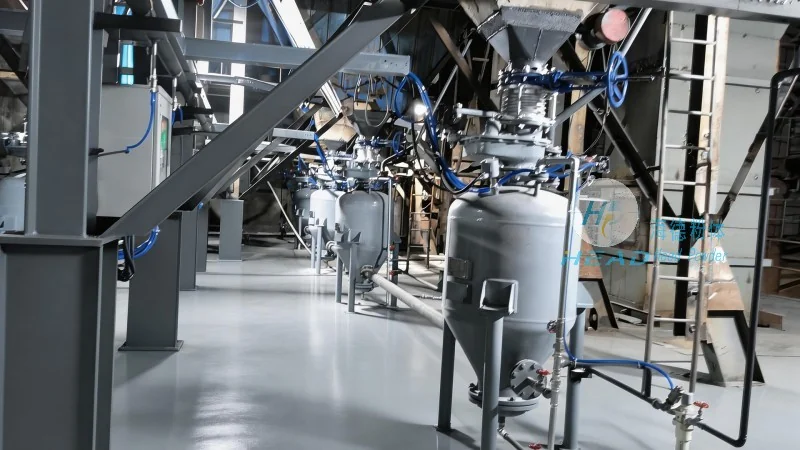
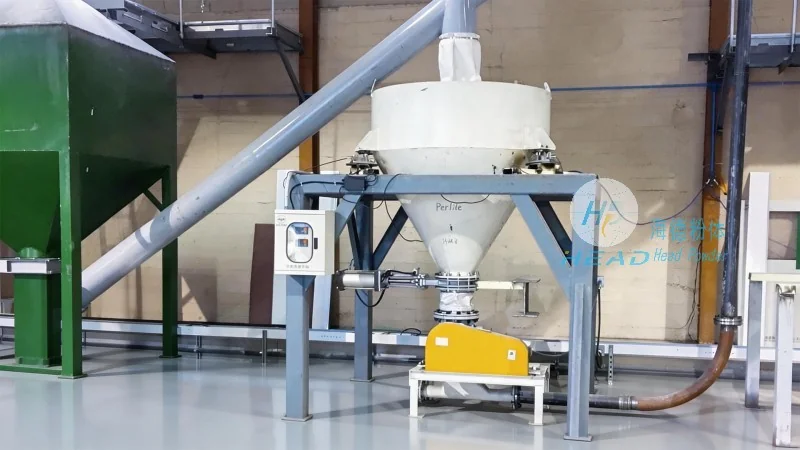
The tonne bag unloading material conveying system comprises several essential components that work in tandem to achieve efficient material transfer. At the heart of the system is the bag opening mechanism, which is designed to safely and cleanly release the contents of the tonne bag. This may involve automated cutting tools or specialized bag openers that can handle various bag materials and sizes. Once the bag is opened, the material falls into a hopper or chute that is connected to the conveying system. The conveying component, which can be a screw conveyor, belt conveyor, or pneumatic conveyor, then transports the material to the next stage of processing. The system may also include features such as a material level sensor, a bag empty detection sensor, and a control panel to monitor and regulate the flow of material. These components are typically constructed from durable materials, such as stainless steel or heavy-duty plastics, to withstand the harsh conditions often encountered in industrial environments.
Core Principle: Controlled Material Flow
The fundamental principle of the tonne bag unloading material conveying system is to maintain a controlled and continuous flow of bulk materials from the bag into the conveying system. This is achieved through a combination of gravity and mechanical forces. The bag opening process is critical, as it must be designed to prevent material spillage or blockages. For example, in systems handling fine powders, the bag opening may be equipped with a dust extraction system to minimize airborne particles and ensure a clean working environment. The hopper or chute is designed with smooth surfaces and appropriate angles to guide the material downward without causing clogging. The conveying mechanism then uses rotational or linear motion to move the material forward, with adjustable speed and capacity settings to match the specific requirements of the application. The system's ability to handle different material characteristics, such as varying densities or moisture content, is a key factor in its effectiveness.
Working Scene Characteristics: Diverse Industrial Applications
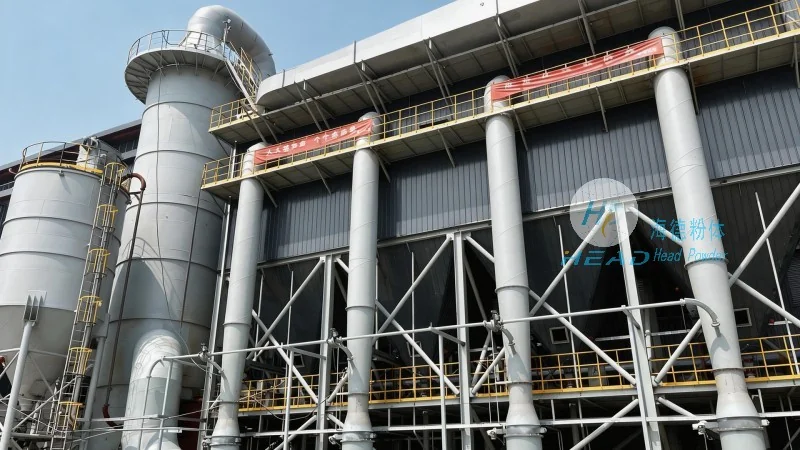
The tonne bag unloading material conveying system is widely adopted across multiple industries due to its versatility and reliability. In the mining industry, this system is essential for transferring ore, coal, or other minerals from tonne bags into crushing or grinding equipment. The high throughput capability of the system allows mining operations to maintain production rates while reducing the time and labor required for manual bag emptying. In the construction sector, the system is commonly used to handle raw materials like sand, gravel, or cement from bulk bags to batching plants or storage silos. The robust design of the system enables it to operate in challenging outdoor conditions, including dust, rain, and extreme temperatures. In the agricultural industry, the system is utilized to transport fertilizers, seeds, or animal feed from storage bags to application equipment, ensuring that these materials are transferred efficiently and without loss. The chemical processing industry also benefits from this technology, as it allows for the safe handling of various chemicals and powders from tonne bags into processing lines, minimizing the risk of exposure and contamination. Each of these applications leverages the system's ability to handle large volumes of material while maintaining operational safety and efficiency.
Advantages and Key Features
Several key advantages make the tonne bag unloading material conveying system a preferred choice for industrial material handling. First, the system significantly reduces manual labor by automating the bag emptying process, which is often a time-consuming and physically demanding task. This not only improves worker safety but also increases overall productivity. Second, the system is designed for high efficiency, with minimal downtime due to its robust construction and reliable components. The ability to adjust the conveying speed and capacity allows operators to match the system's performance to the specific needs of the production line. Third, the system is highly adaptable, with options available to handle a wide range of materials, including powders, granules, and bulk solids. This adaptability makes it suitable for diverse applications across multiple industries. Additionally, the system is equipped with monitoring and control features, such as material level indicators and bag empty sensors, which enable operators to track the system's performance and address any issues promptly. The integration of these features ensures optimal operation and reduces the risk of material loss or equipment damage.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer and supplier of advanced material handling equipment, including tonne bag unloading material conveying systems. HeadPowder has established itself as a trusted partner for industries requiring reliable and efficient solutions for bulk material handling. The company is headquartered in Shandong, China, and has a dedicated team of experienced engineers and technicians who specialize in designing and manufacturing equipment tailored to the specific needs of their clients. With a strong commitment to innovation and quality, HeadPowder continuously invests in research and development to improve the performance and functionality of their products. The company's products are widely recognized for their durability, efficiency, and ease of use, making them a preferred choice for businesses across various industries. HeadPowder's customer-centric approach and focus on delivering high-quality solutions have contributed to its reputation as a leading provider in the material handling industry.




