The Baking Soda Powder Conveying System, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized equipment designed for the efficient and safe transportation of sodium bicarbonate powder. This system is crucial in various industrial applications where precise powder handling is essential, ensuring minimal loss and contamination during the conveying process. HeadPowder, a leading manufacturer in the field, has engineered this system to meet the stringent requirements of modern industrial operations, combining advanced technology with robust design to deliver reliable performance.
Key Components of the Conveying System
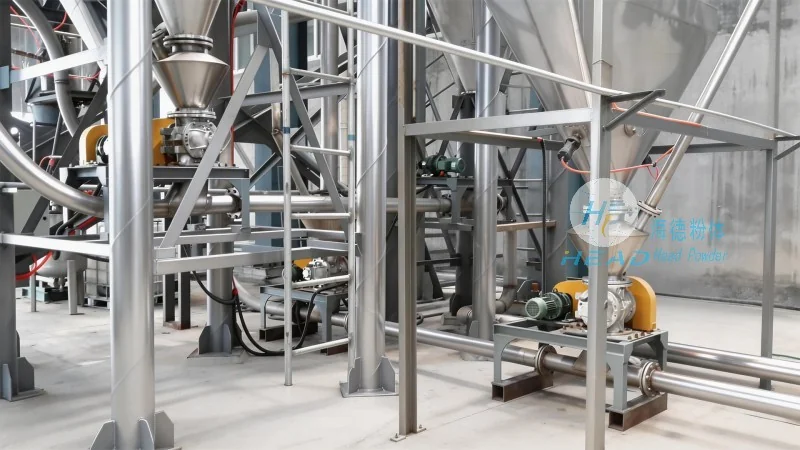
The Baking Soda Powder Conveying System consists of several critical components that work in tandem to ensure smooth operation. The main components include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic system), a control panel for operational management, and a dust collection system to maintain air quality. Each component is carefully selected and integrated to handle the unique properties of baking soda powder, which is light, fine, and prone to dust generation. The hopper is designed with a sloped bottom to facilitate material flow, while the conveyor system is equipped with anti-static features to prevent powder accumulation and ensure safe operation. The control panel allows operators to monitor and adjust the conveying speed, pressure, and other parameters in real-time, enhancing the system's adaptability to varying production demands.
Operation Process of the Conveying System
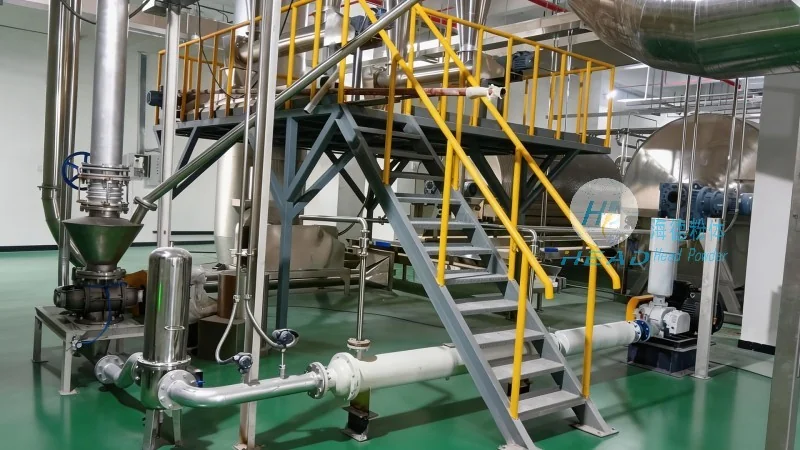
The operation of the Baking Soda Powder Conveying System follows a systematic process that ensures efficient material transfer from the storage hopper to the destination point. The process begins with the loading of baking soda powder into the hopper. The powder is then released into the conveyor mechanism under controlled conditions. For systems utilizing a screw conveyor, the rotating screw pushes the powder forward through the conveyor tube. In pneumatic conveying systems, the powder is carried by a stream of air, which is then separated from the powder at the discharge point. The control panel continuously monitors the pressure and flow rate, adjusting the air or screw speed as needed to maintain optimal conveying efficiency. The system also includes safety features such as pressure relief valves and dust filters to prevent over-pressurization and ensure environmental compliance. Throughout the operation, the system maintains a consistent flow rate, minimizing variations that could affect downstream processes. The entire process is automated to a large extent, reducing the need for manual intervention and enhancing operational efficiency.
Working Principle of the Conveying System
The working principle of the Baking Soda Powder Conveying System is based on the principles of fluid dynamics and mechanical force. In a screw conveyor system, the rotating screw acts as a positive displacement pump, pushing the powder forward by creating a pressure gradient. The screw's pitch and diameter are optimized to handle the specific characteristics of baking soda powder, ensuring minimal friction and wear. The system's design minimizes the risk of clogging by using smooth, corrosion-resistant materials and incorporating self-cleaning features. In pneumatic conveying systems, the principle of air movement is utilized to transport the powder. The air is compressed and directed through the conveying line, carrying the powder particles. The velocity of the air is carefully controlled to ensure that the powder is suspended without causing excessive wear on the system components. The separation of powder and air at the discharge point is achieved through a cyclone or filter, which allows the powder to be collected while the air is released back into the system or exhausted. The control system continuously adjusts the air pressure and flow rate to maintain the optimal conveying velocity, ensuring that the powder is transported efficiently without degradation. The working principle also incorporates safety mechanisms to prevent dust explosions, such as grounding and bonding of the system to dissipate static electricity.
Advantages of the Baking Soda Powder Conveying System
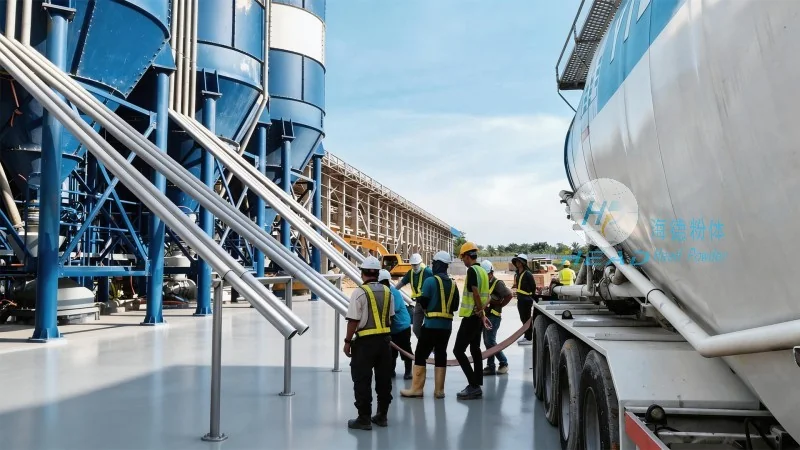
Shandong HeadPowder Engineering Co., Ltd.'s Baking Soda Powder Conveying System offers several advantages that make it a preferred choice in industrial applications. The system's design minimizes material loss and contamination, which is critical in processes where the purity of baking soda powder is essential. The automated operation reduces labor costs and improves consistency, as the system can maintain a constant flow rate regardless of variations in material feed. The system's robust construction ensures long-term reliability, with components designed to withstand the abrasive nature of the powder. Additionally, the system's energy efficiency is enhanced by optimized control mechanisms, reducing operational costs. The safety features, including dust collection and anti-static measures, comply with environmental regulations and protect personnel from health hazards. The system's adaptability allows it to be integrated into existing production lines with minimal modifications, making it a cost-effective solution for upgrading or expanding powder handling capabilities.




