Efficient and reliable sugar material conveying systems are crucial for the smooth operation of sugar processing facilities. These systems ensure that raw sugar, intermediate products, and finished goods are transported safely and efficiently from one stage of production to another. Understanding the operation process and working principles of such systems is essential for optimizing industrial processes and maintaining high productivity in the sugar industry.
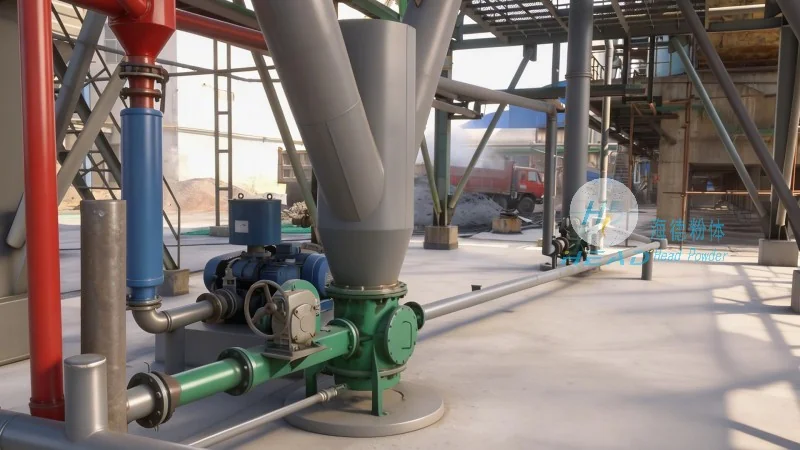
Overview of Sugar Material Conveying Systems
Sugar material conveying systems are specialized equipment designed to handle the transportation of various forms of sugar, including raw cane sugar, refined sugar, and other sugar derivatives. These systems are integral to the overall workflow in sugar processing plants, connecting different processing units such as crushing, refining, and packaging. The design and operation of these systems are tailored to meet the specific requirements of the sugar production process, ensuring minimal loss, maximum throughput, and adherence to safety standards.
The Operation Process of Sugar Material Conveying
The operation process of sugar material conveying involves several key steps that work in tandem to ensure seamless material movement. The process typically begins with the loading of raw sugar or intermediate products into the conveying equipment. This is followed by the activation of the conveying mechanism, which may include belt conveyors, screw conveyors, or pneumatic systems, depending on the type of sugar and the plant's configuration. As the material is transported, it moves through various stages, such as elevation changes, horizontal transport, and storage, before reaching its final destination. Each step is carefully controlled to maintain the integrity of the sugar product and prevent contamination or degradation.
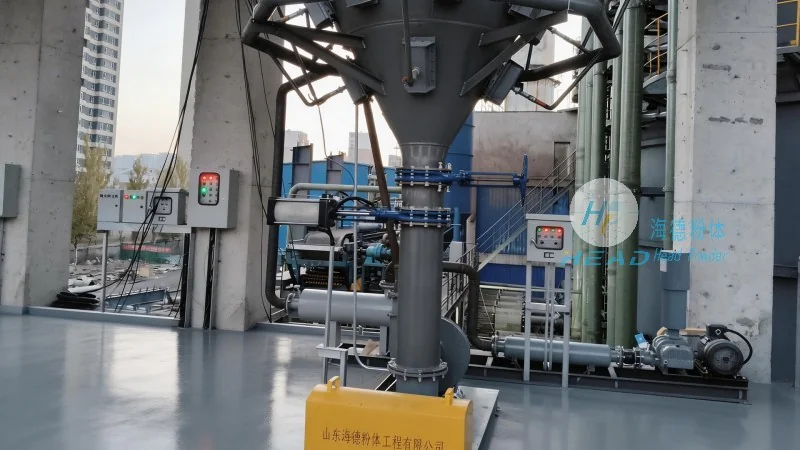
Working Principles of Sugar Material Conveying Equipment
The working principles of sugar material conveying equipment vary based on the technology used. For instance, belt conveyors utilize a continuous belt that moves over rollers or pulleys, carrying the sugar material along its path. Screw conveyors, on the other hand, use a rotating screw to push the material forward, making them suitable for vertical or inclined transport. Pneumatic conveying systems employ air pressure to move sugar particles through a pipeline, which is particularly effective for fine sugar powders. Each system operates on fundamental principles of mechanics and fluid dynamics, ensuring consistent and controlled movement of the material.
Key Components and Their Functions
Several key components are integral to the effective operation of sugar material conveying systems. These include the feed hopper, which holds the raw material and regulates its flow into the conveyor; the conveyor itself, which transports the material; the drive mechanism, which provides the necessary power to move the conveyor; and the control system, which monitors and adjusts the operation based on real-time conditions. Additionally, safety features such as emergency stop buttons, overload protection, and dust suppression systems are incorporated to ensure the safety of operators and the integrity of the product.
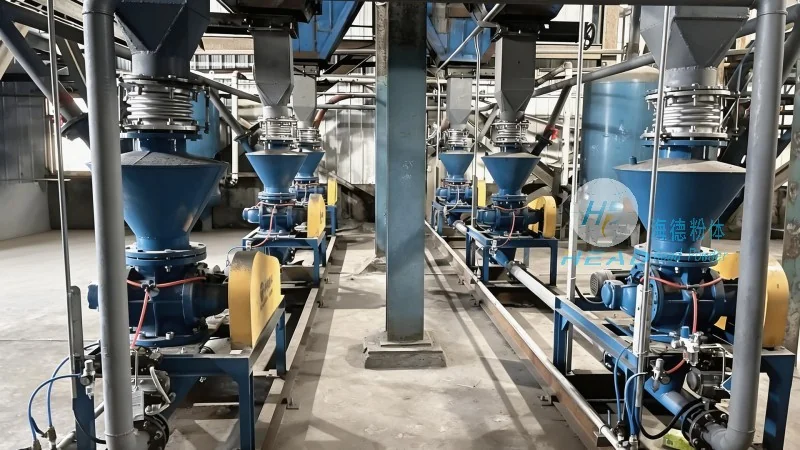
HeadPowder Engineering's Expertise in Sugar Material Conveying
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced sugar material conveying solutions. With years of experience in the sugar industry, HeadPowder specializes in designing, manufacturing, and installing customized conveying systems that meet the unique needs of sugar processing facilities. The company's team of engineers and technicians leverages cutting-edge technology and industry best practices to develop solutions that enhance efficiency, reduce downtime, and improve overall productivity. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for sugar manufacturers worldwide.
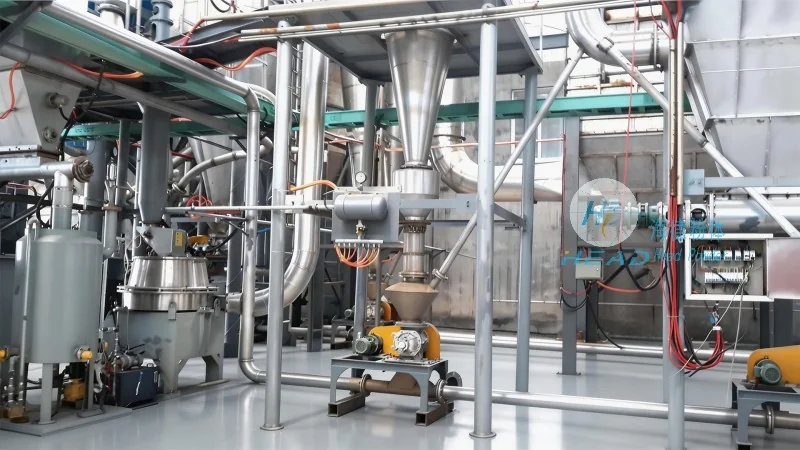
Benefits of Using Professional Conveying Systems
Implementing professional sugar material conveying systems offers numerous benefits for sugar processing plants. These systems improve operational efficiency by reducing manual handling and increasing throughput. They also enhance product quality by minimizing handling-related damage and contamination. Additionally, advanced conveying systems can help reduce energy consumption and maintenance costs over time. By investing in reliable conveying solutions, sugar manufacturers can achieve better control over their production processes and stay competitive in the global market.
Conclusion
In conclusion, the operation process and working principles of sugar material conveying systems are critical to the success of sugar processing operations. By understanding these systems and leveraging advanced technology, sugar manufacturers can optimize their production lines, improve efficiency, and ensure the quality of their products. HeadPowder Engineering, with its expertise and commitment to excellence, continues to provide top-tier conveying solutions that meet the evolving needs of the sugar industry. For those seeking reliable and efficient sugar material conveying systems, HeadPowder is a trusted partner that delivers results.




