The dust-free pneumatic conveying system represents a sophisticated industrial solution for transporting bulk materials in a controlled, contamination-free environment. This technology is indispensable across sectors like food processing, pharmaceuticals, and chemical manufacturing, where maintaining a clean and hygienic workspace is non-negotiable. The system leverages compressed air or gas to move materials through a sealed pipeline, effectively preventing dust leakage and preserving product integrity. HeadPowder, a leading manufacturer headquartered in Shandong, China, specializes in developing and supplying high-performance dust-free pneumatic conveying systems that are customized to meet diverse industry requirements.
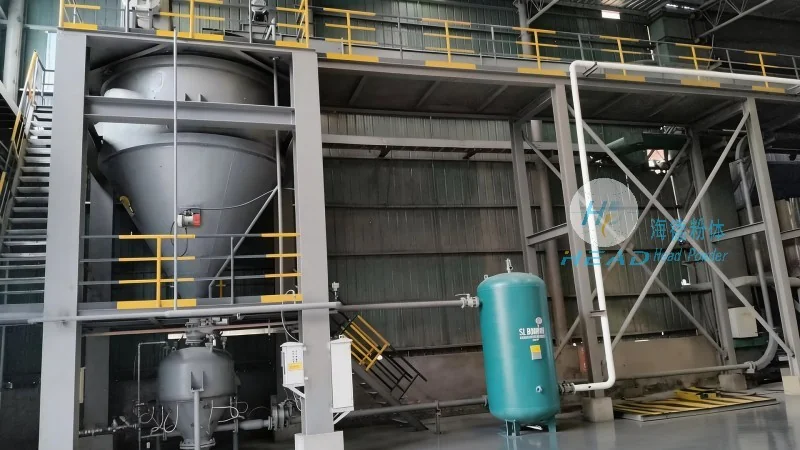
Key Components of the Dust-Free Pneumatic Conveying System
The core components of a dust-free pneumatic conveying system include the material feeder, conveying pipeline, air compressor, and material separator. The material feeder is engineered to introduce bulk materials into the system in a controlled manner, ensuring a consistent flow rate. The conveying pipeline, typically constructed from stainless steel or other corrosion-resistant materials, is designed to be airtight and prevent any dust leakage. The air compressor provides the necessary pressure and airflow to propel the materials through the pipeline. The material separator, such as a cyclone or bag filter, is crucial for separating the conveyed material from the air, ensuring that the air is clean and the material remains free of contaminants. Each component is meticulously engineered to operate in harmony, guaranteeing efficient and reliable performance of the entire system.
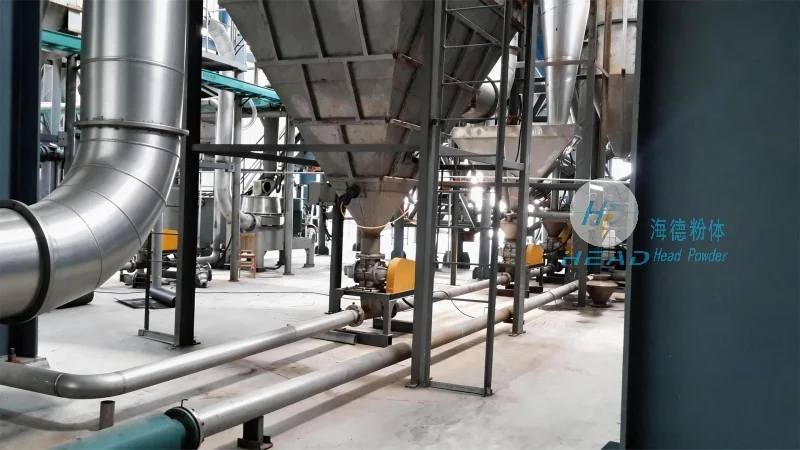
Structural Principles and Working Mechanism
The structural principle of the dust-free pneumatic conveying system is centered on creating a pressure differential using compressed air to move materials through a sealed pipeline. The system operates in two primary modes: dilute phase and dense phase. In the dilute phase, the material is suspended in the air stream and transported at relatively high speeds, suitable for handling non-delicate materials. In the dense phase, the material is conveyed in a more compact form at lower speeds, ideal for transporting sensitive or fragile materials. The working mechanism involves the material feeder releasing bulk material into the pipeline, where it is picked up by the air stream and carried to the destination. The air and material then enter the separator, where the material is separated from the air and collected in a designated container. The clean air is subsequently discharged or recycled back into the system. This continuous process can be automated to handle large volumes of material with minimal human intervention, enhancing operational efficiency.
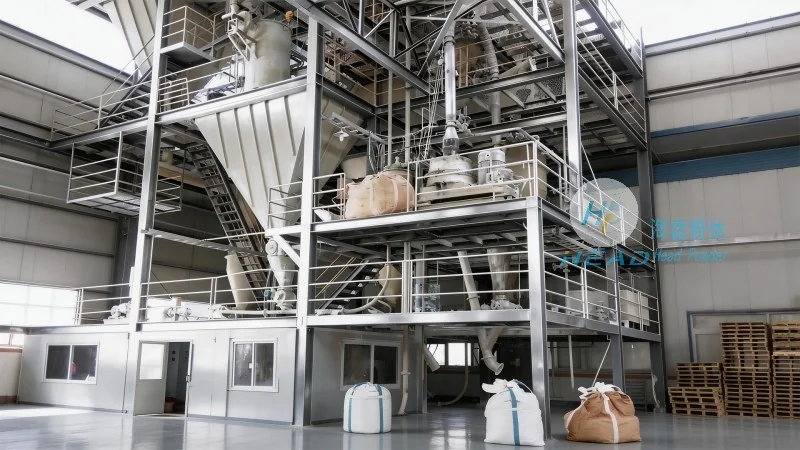
Application Scenarios and Benefits
Dust-free pneumatic conveying systems are widely adopted across various industries due to their versatility and efficiency. In the food industry, they are used to transport ingredients like flour, sugar, and spices without contaminating the product or the environment. In the pharmaceutical industry, they are employed to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring product purity and compliance with stringent hygiene standards. In the chemical industry, they are utilized to transport powders and granules, reducing the risk of dust explosions and improving workplace safety. The benefits of implementing a dust-free pneumatic conveying system include enhanced product quality, reduced labor costs, increased operational safety, and improved environmental compliance. Additionally, the system is easy to clean and maintain, which is critical in industries where hygiene is a top priority, such as food and pharmaceutical manufacturing.
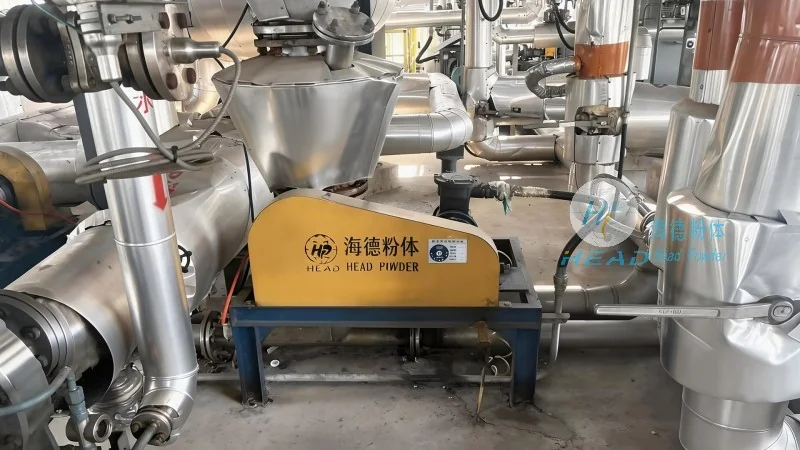
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of dust-free pneumatic conveying systems based in Shandong, China. The company has established a strong reputation for producing high-quality, reliable equipment that adheres to the strictest industry standards. With years of experience in the field, HeadPowder has developed a comprehensive range of products tailored to meet the specific needs of different industries. The company's products are designed with the latest technological advancements and engineering principles, ensuring they are efficient, durable, and easy to maintain. HeadPowder's unwavering commitment to quality and customer satisfaction has positioned it as a trusted partner for businesses seeking reliable dust-free pneumatic conveying solutions. The company's location in Shandong provides access to robust manufacturing capabilities and supply chains, further supporting its ability to deliver high-quality products to clients globally.




