For industrial applications involving the handling of powdered electrolytes, efficient and reliable material transport is crucial. Pneumatic conveying systems offer a solution that minimizes dust generation, ensures product integrity, and enhances operational safety. This article explores the working principle and key features of the powdered electrolyte pneumatic conveying equipment, highlighting its benefits and technical advantages.
Working Principle of Powdered Electrolyte Pneumatic Conveying Systems
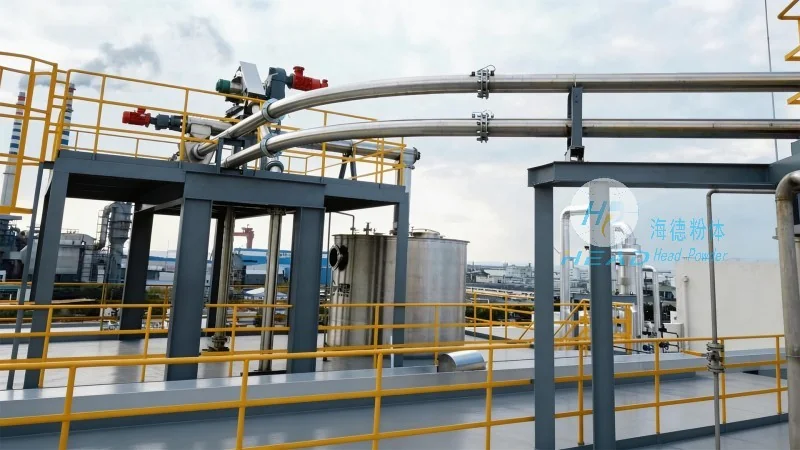
The core operation of a powdered electrolyte pneumatic conveying system involves the use of compressed air to transport material from a source to a destination. The process typically begins with the material being fed into a hopper or feeder. As air is introduced into the system, it creates a low-pressure zone that draws the powder into the conveying line. The air and powder mixture then travels through the pipeline, with the air providing the necessary force to move the material. At the receiving end, the air is separated from the powder, often through a cyclone or filter, allowing the electrolyte powder to be deposited in the desired location. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing system reliability.
Key Features and Advantages
Several distinct features make powdered electrolyte pneumatic conveying equipment an ideal choice for handling sensitive materials. First, the system is designed to minimize product contamination and degradation. The enclosed pipeline and controlled air flow prevent exposure to external elements, preserving the chemical properties of the electrolyte powder. Second, it offers high efficiency in material transport, with the ability to handle large volumes of powder over long distances with minimal energy consumption. Third, the equipment is highly flexible, allowing for easy integration into existing production lines and adaptability to different operational requirements. Additionally, the system provides excellent dust control, contributing to a safer working environment and compliance with environmental regulations. The compact design of the equipment also saves space in industrial facilities, making it suitable for both new installations and retrofit applications.
Technical Specifications and Performance
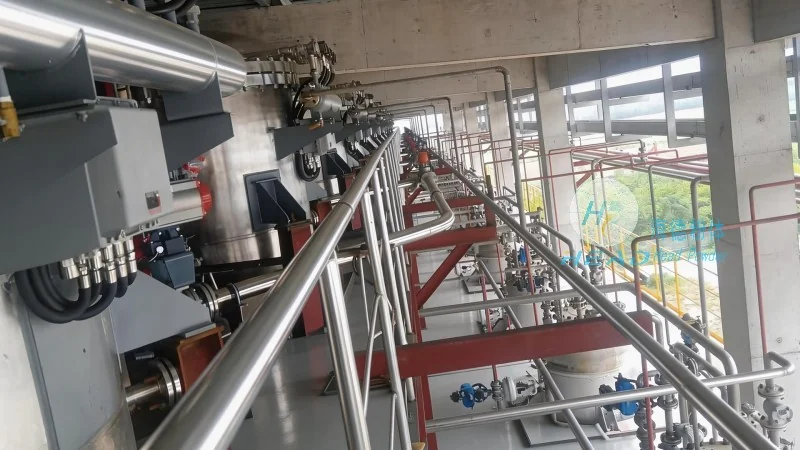
When evaluating powdered electrolyte pneumatic conveying systems, several technical aspects are critical. The system's capacity, measured in terms of material flow rate, is determined by factors such as air pressure, pipeline diameter, and the specific characteristics of the powder (e.g., particle size, density). The headpowder system, as a leading manufacturer in this field, offers customizable solutions tailored to the unique needs of each client. For instance, the equipment can be configured with different hopper sizes, air pressure ranges, and conveying distances to optimize performance. The use of high-quality materials, such as stainless steel for the conveying lines and components, ensures durability and resistance to corrosion, which is essential when handling electrolyte powders that may be acidic or caustic. Furthermore, the system incorporates advanced control mechanisms that allow for precise regulation of air flow and material feed, enhancing operational stability and reducing waste.
Applications and Industries
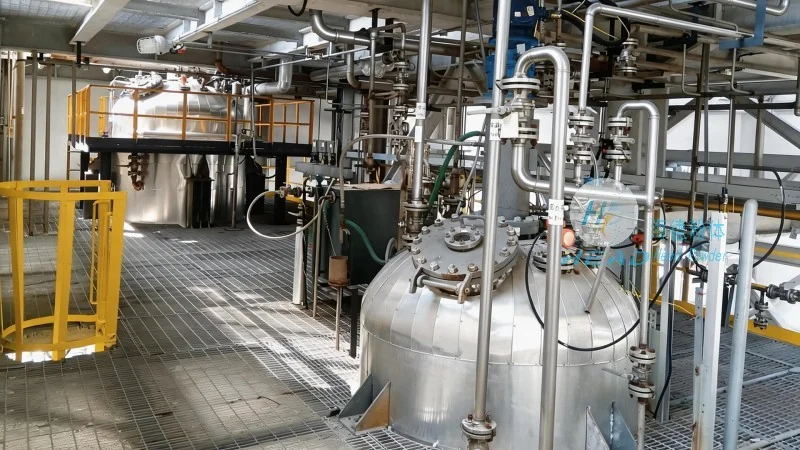
Powdered electrolyte pneumatic conveying equipment finds applications across various industries where electrolyte powders are used. In the battery manufacturing sector, these systems are vital for transporting lithium, cobalt, and other electrolyte components to production lines, ensuring consistent quality and efficiency. The chemical industry also relies on such equipment for handling caustic or corrosive electrolyte powders, where dust control and material integrity are paramount. Additionally, in the pharmaceutical and food processing industries, the system's ability to maintain product purity and prevent contamination makes it suitable for handling sensitive electrolyte formulations. The versatility of the equipment allows it to be adapted to a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Conclusion and Company Overview
In conclusion, the powdered electrolyte pneumatic conveying equipment is a sophisticated solution for the efficient and safe transport of electrolyte powders. Its working principle, based on pneumatic technology, offers numerous advantages over traditional mechanical conveying methods. The key features, including minimal contamination, high efficiency, and flexible design, make it a preferred choice for industries requiring reliable material handling. As a company dedicated to engineering excellence, Shandong HeadPowder Engineering Co., Ltd. (headpowder) specializes in designing and manufacturing these systems, leveraging years of experience to deliver customized solutions that meet the specific demands of each client. With operations based in China, the company is committed to providing high-quality equipment that enhances operational performance and ensures compliance with industry standards. The equipment's ability to handle a variety of electrolyte powders, combined with its robust construction and advanced control systems, positions it as a leading solution in the market for material transport in industrial applications.




