Positive pressure dilute phase pneumatic conveying systems are advanced industrial solutions designed to efficiently transport bulk materials over long distances with minimal pressure loss and high reliability. This technology is widely used in various industries, including food, pharmaceuticals, chemicals, and minerals, where maintaining product integrity and ensuring a clean, dust-free environment is critical. The system operates by injecting compressed air into the material stream, creating a dilute suspension that moves through the pipeline. Understanding the equipment and structural principles is essential for optimizing performance and ensuring long-term operational efficiency. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to meet the diverse needs of industrial clients.
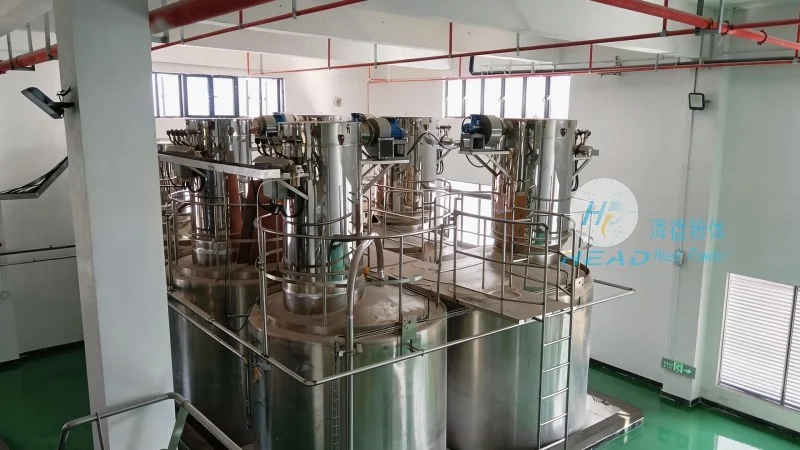
Overview of Key Components in Positive Pressure Dilute Phase Pneumatic Conveying Systems
The core components of a positive pressure dilute phase pneumatic conveying system include the material feeder, air compressor, conveying pipeline, and control system. The material feeder is responsible for introducing the bulk material into the system at a consistent rate, ensuring a stable flow. The air compressor provides the necessary pressure to create the material-air suspension. The conveying pipeline transports the mixture, while the control system monitors and adjusts parameters such as pressure, flow rate, and material feed to maintain optimal performance. Each component plays a crucial role in the overall functionality of the system, and proper integration is vital for efficient operation.
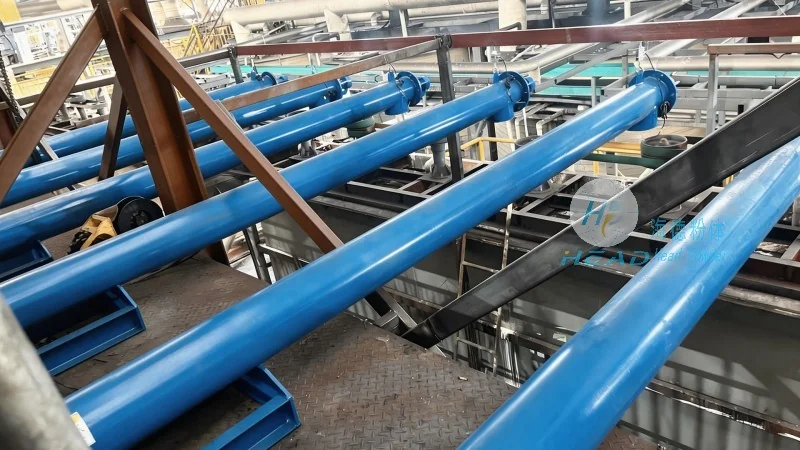
Structural Principles of the Conveying Pipeline and Air Compressor
The conveying pipeline is typically made of durable materials like stainless steel or plastic, designed to withstand the pressure and abrasion from the material-air mixture. The pipeline layout is carefully planned to minimize pressure drop and ensure smooth material flow. The air compressor, often a positive displacement type, generates the required pressure to move the material. It is equipped with features such as pressure regulation and safety valves to prevent over-pressurization and ensure safe operation. The structural design of both the pipeline and compressor is optimized to handle the specific characteristics of the conveyed material, such as particle size, density, and moisture content.
Material Feeder and Control System Integration
The material feeder, which can be a rotary valve, screw feeder, or other type, ensures that the bulk material is introduced into the system at a controlled rate. This consistency is crucial for maintaining a stable material-air ratio, which directly impacts the conveying efficiency. The control system, often integrated with sensors and automation technology, monitors key parameters like pressure, flow rate, and material level. It adjusts the feeder speed or compressor output to compensate for variations in material feed or pipeline conditions, ensuring consistent performance. The integration of these components allows for real-time monitoring and adjustment, enhancing the system's adaptability and reliability.
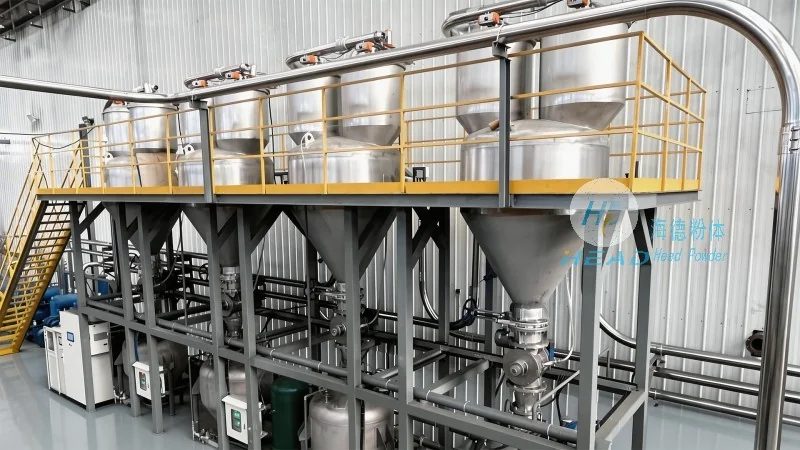
Operational Advantages and Applications
Positive pressure dilute phase pneumatic conveying systems offer several advantages over other material handling methods. These include the ability to transport materials over long distances, handle a wide range of particle sizes, and maintain product cleanliness and integrity. The system is also relatively compact and can be easily integrated into existing industrial facilities. In applications such as food processing, where hygiene is paramount, the system's ability to prevent contamination and maintain product quality is a significant benefit. Similarly, in chemical and pharmaceutical industries, the system's ability to handle sensitive materials without degradation is critical. The versatility of the system makes it suitable for various industries, from bulk material transport to specialized applications requiring precise control over material flow. With years of expertise in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide customized solutions that enhance operational efficiency and product quality for its clients.




