Efficient and reliable material handling is crucial in the coffee processing industry, particularly when dealing with dry coffee powders. The dry coffee powder pneumatic conveying machine, a specialized equipment designed for transporting bulk dry powders like coffee grounds or instant coffee, plays a vital role in optimizing production workflows. This article explores the working principle and key features of such a machine, providing insights into its functionality and benefits for coffee manufacturers.
Understanding the Working Principle of a Dry Coffee Powder Pneumatic Conveying Machine
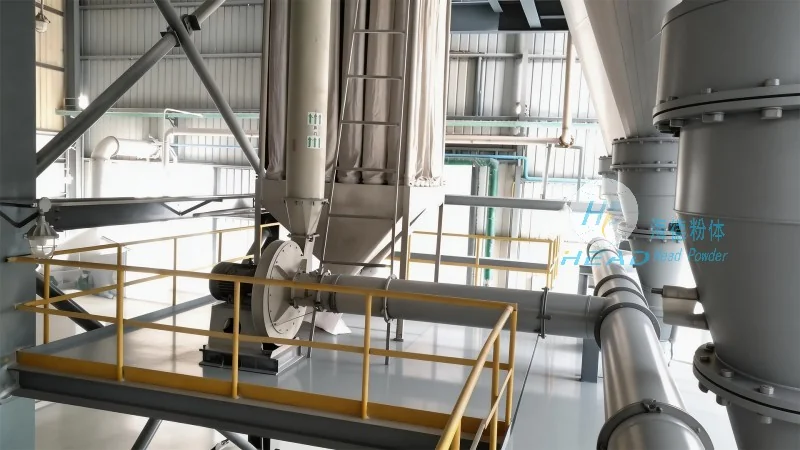
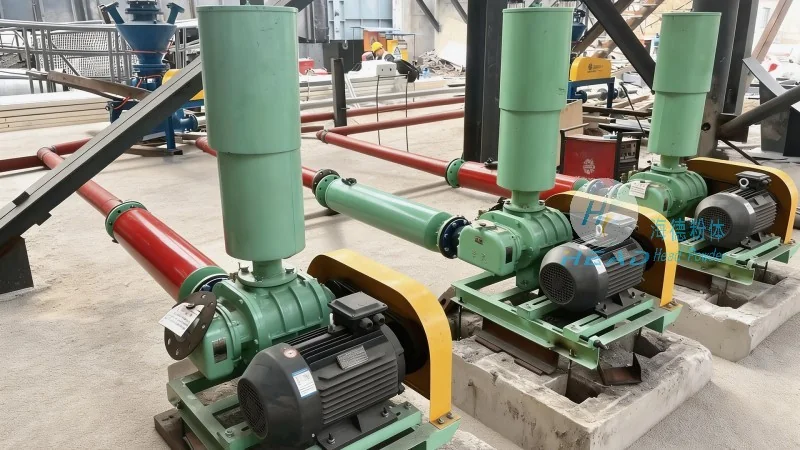
The core mechanism of a dry coffee powder pneumatic conveying machine relies on the principles of fluidization and air movement. At its essence, the machine uses compressed air to create a flow that transports the coffee powder from the source to the destination. The process typically involves several key components working in tandem: a hopper for material storage, a blower or air compressor to generate the necessary air pressure, a pipeline system to direct the air and powder mixture, and a receiver or discharge unit for the final product collection. The coffee powder is fed into the hopper, and as the compressed air is introduced into the pipeline, it creates a low-pressure zone that draws the powder particles into the air stream. This mixture, often referred to as a "pneumatic slurry," is then propelled through the pipeline to the receiving vessel. The air pressure and velocity are carefully controlled to ensure the powder is conveyed without degradation, clogging, or excessive wear on the system components. The working principle is based on the concept of "air lift" or "air transport," where the air acts as the medium to move the solid particles, leveraging the differential pressure between the inlet and outlet of the system. This method allows for a continuous, closed-loop operation that minimizes material exposure to external contaminants and reduces the risk of dust emissions compared to traditional bulk handling methods.
Key Features of a Dry Coffee Powder Pneumatic Conveying Machine
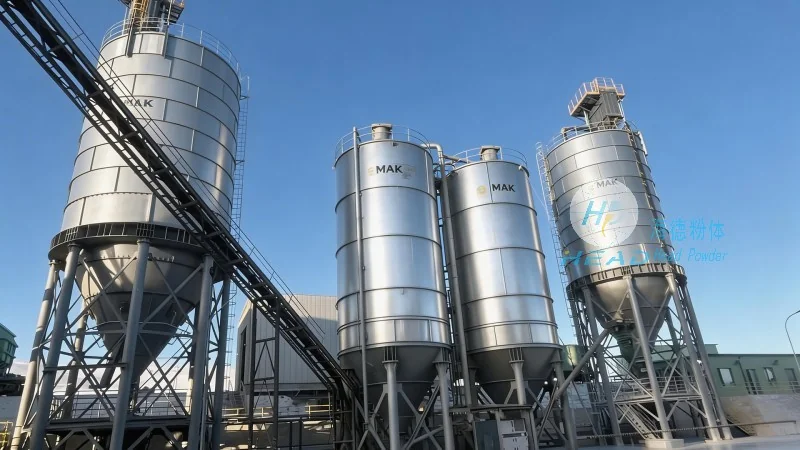
When evaluating a dry coffee powder pneumatic conveying machine, several critical features stand out as essential for optimal performance in coffee processing applications. Firstly, the machine is designed with a focus on maintaining product integrity. The use of gentle air pressure and controlled flow rates prevents the coffee powder from being crushed or agglomerated, preserving its flavor, aroma, and quality. This is particularly important for specialty coffees where the sensory attributes are paramount. Secondly, the system offers high efficiency in terms of material throughput. The continuous operation and low friction in the pipeline allow for rapid transport of large quantities of coffee powder, reducing downtime and increasing overall production capacity. Thirdly, the machine provides excellent dust control and environmental safety. By operating in a closed system, it minimizes the release of fine coffee particles into the air, adhering to occupational health and safety standards and reducing the risk of product contamination from external sources. Additionally, the design incorporates features such as adjustable air pressure and flow control, enabling operators to customize the conveying parameters based on the specific characteristics of the coffee powder being handled—such as particle size, moisture content, or density. This adaptability ensures that the machine can handle a wide range of coffee products, from fine instant coffee powders to coarser ground coffee. Another notable feature is the durability and corrosion resistance of the components, especially the pipelines and valves, which are often made from materials like stainless steel or food-grade plastics to withstand the abrasive nature of coffee powder and prevent contamination. The system also includes safety features such as pressure relief valves and overcurrent protection to ensure safe operation and prevent equipment damage. Overall, these features combine to make the dry coffee powder pneumatic conveying machine a versatile and reliable solution for coffee manufacturers seeking to enhance their material handling processes.
About Shandong HeadPowder Engineering Co., Ltd.
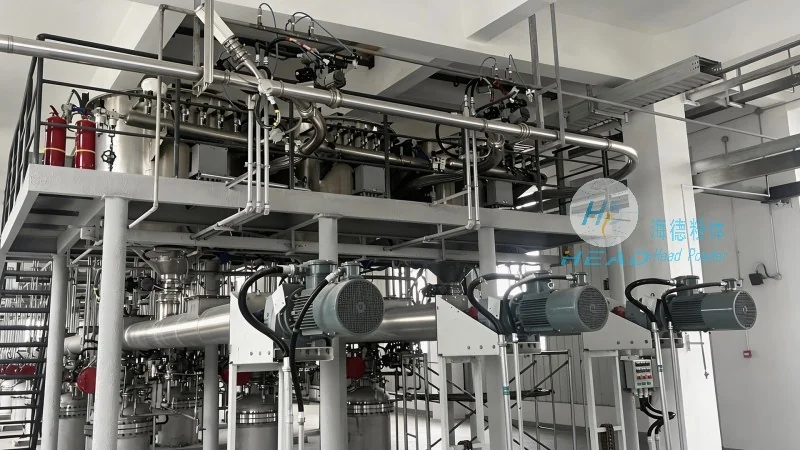
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in the design, development, and production of pneumatic conveying systems for various industries, including food and beverage processing. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses requiring efficient and safe material handling solutions. HeadPowder's expertise lies in creating customized pneumatic conveying machines tailored to the specific needs of each client, ensuring optimal performance and compliance with industry standards. The company's facilities are located in Shandong, China, where advanced manufacturing processes and rigorous quality control measures are employed to produce high-performance equipment. By leveraging years of experience in the field, HeadPowder continues to deliver reliable and durable solutions that meet the evolving demands of the coffee processing industry and other sectors. The company's dedication to customer satisfaction and product excellence has earned it a reputation for delivering top-tier pneumatic conveying systems that enhance operational efficiency and product quality.




