For industrial applications requiring efficient and reliable transport of cement clinker powder, pneumatic conveying systems have emerged as a preferred solution. This article delves into the working principle and key features of cement clinker powder pneumatic conveying equipment, highlighting how it addresses the unique challenges of handling such materials.
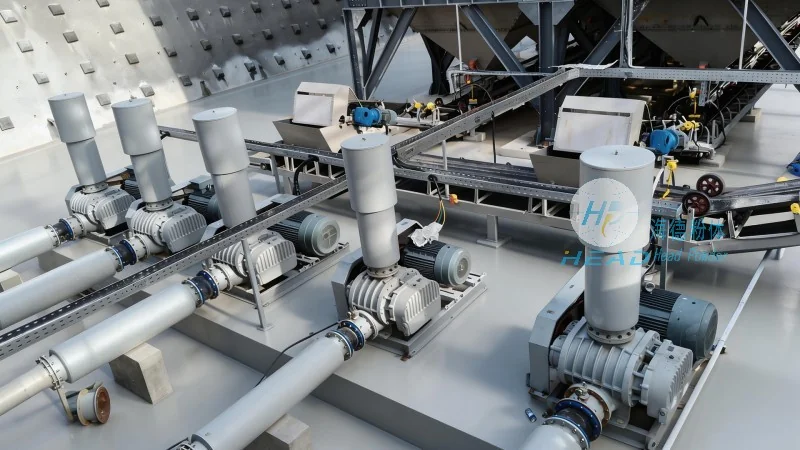
Understanding the Working Principle of Cement Clinker Powder Pneumatic Conveying Systems
The core mechanism of cement clinker powder pneumatic conveying involves the use of air or gas to transport dry powder materials through a pipeline network. In this system, a blower or compressor generates a flow of air that draws the cement clinker powder from the source hopper into the conveying line. The powder is then suspended in the air stream and propelled to the destination point, such as a storage silo or processing unit. The process typically operates under negative pressure (suction) or positive pressure (blowing), depending on the system design and application requirements. The air flow rate is carefully controlled to ensure optimal particle suspension and minimal particle degradation, which is crucial for maintaining the quality of cement clinker powder.
Key Features of Cement Clinker Powder Pneumatic Conveying Equipment
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, offers advanced cement clinker powder pneumatic conveying systems with several distinct features that enhance performance and reliability. These features include:
1. High Efficiency and Low Energy Consumption: The equipment is designed to minimize energy usage while maximizing conveying capacity. Advanced blower technology and optimized air flow management contribute to energy savings without compromising material transport efficiency.
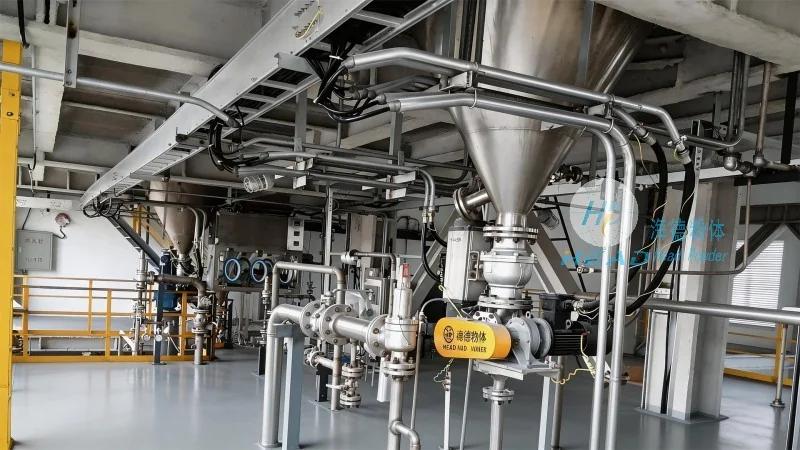
2. Low Maintenance Requirements: Constructed with durable materials and robust components, the system reduces the need for frequent maintenance, lowering operational costs and downtime for industrial facilities.
3. Adaptability to Various Particle Sizes and Properties: The conveying equipment can handle a wide range of cement clinker powder characteristics, including different particle sizes, moisture content, and flowability. This adaptability makes it suitable for diverse industrial applications, from cement production to material handling in chemical plants.
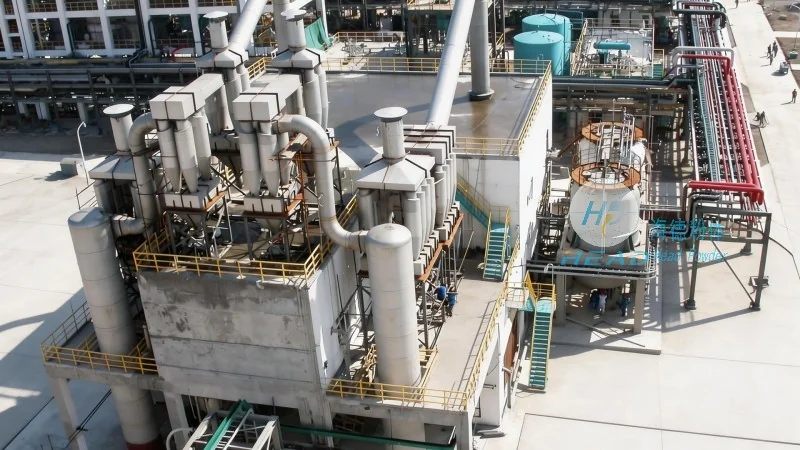
4. Minimal Material Loss and Contamination: The sealed pipeline system prevents dust emissions and cross-contamination, ensuring that the cement clinker powder remains clean and free from external contaminants. This is particularly important for applications where material purity is critical.
5. Easy Integration with Existing Infrastructure: The modular design of the pneumatic conveying equipment allows for seamless integration with existing industrial setups, reducing installation time and complexity. This feature is beneficial for facilities looking to upgrade or expand their material handling capabilities.
Conclusion and Company Overview
As a reputable company in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality cement clinker powder pneumatic conveying solutions tailored to the specific needs of industrial clients. By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its equipment meets the highest standards of performance, reliability, and efficiency. With a focus on customer satisfaction and long-term partnerships, the company continues to be a trusted provider of pneumatic conveying systems for the cement and related industries.




