Pharmaceutical granule material conveying is a critical process in the pharmaceutical manufacturing industry, ensuring the efficient and safe transportation of active pharmaceutical ingredients (APIs) and excipients from one stage of production to another. The proper operation of conveying systems is essential for maintaining product quality, adhering to regulatory standards, and optimizing production efficiency. This article provides an in-depth look at the operation process and working principles of pharmaceutical granule material conveying, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading company in the field.
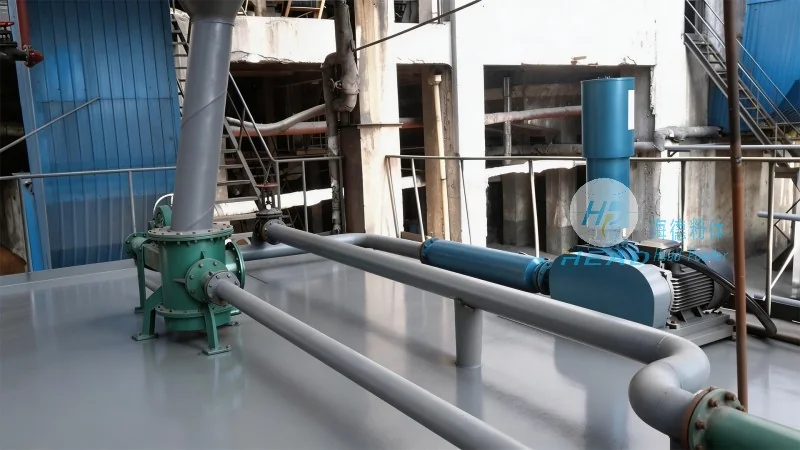
HeadPowder: Your Trusted Partner in Pharmaceutical Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of advanced conveying systems tailored for the pharmaceutical industry. With a strong presence in China, particularly in Shandong province, HeadPowder has established itself as a reliable partner for pharmaceutical companies seeking to enhance their material handling capabilities. The company’s headquarters and primary operations are located in Shandong, China, where it leverages local expertise and resources to deliver high-quality, customized solutions that meet the stringent requirements of the pharmaceutical sector.
The Core Components and Operation Process of Pharmaceutical Granule Conveying Systems
Pharmaceutical granule material conveying systems typically consist of several key components, each playing a vital role in the overall operation. These components include feeders, conveyors (such as screw conveyors, belt conveyors, or pneumatic systems), control systems, and safety features. The operation process begins with the loading of granules into the feeder, which regulates the flow rate to ensure a consistent and controlled supply to the conveyor. The conveyor then transports the granules through the system, often under controlled temperature and humidity conditions to prevent degradation or contamination. Advanced systems may incorporate sensors and monitoring devices to track the material flow and detect any anomalies in real-time.
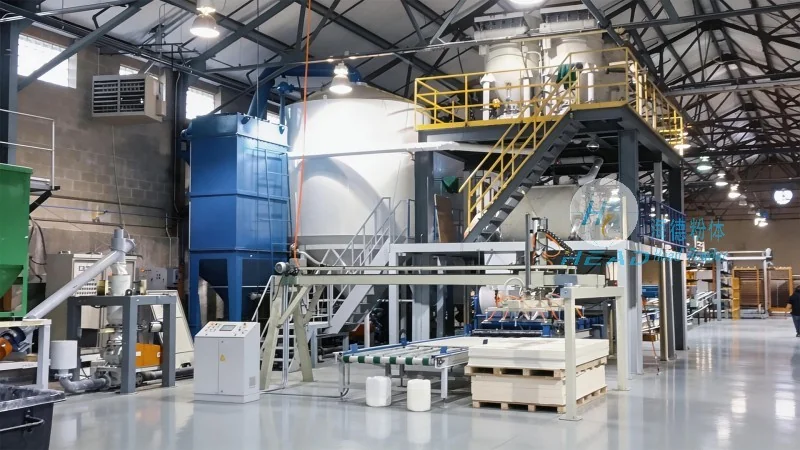
Working Principles of Pharmaceutical Granule Conveying Systems
The working principle of pharmaceutical granule material conveying systems revolves around the transfer of bulk materials through mechanical or pneumatic means. Mechanical conveyors, such as screw conveyors, utilize rotating screws to move granules along a tube or trough. The rotation of the screw creates a pushing force that propels the material forward, while the design of the screw (e.g., pitch, diameter) can be adjusted to control the flow rate and prevent material degradation. Belt conveyors, on the other hand, use a continuous belt to transport granules, often with idlers and pulleys to maintain tension and direction. Pneumatic conveying systems employ air or gas to transport granules through a pipeline, using pressure differentials to move the material. Each type of conveyor has its advantages and is selected based on factors such as material characteristics, required throughput, and space constraints.
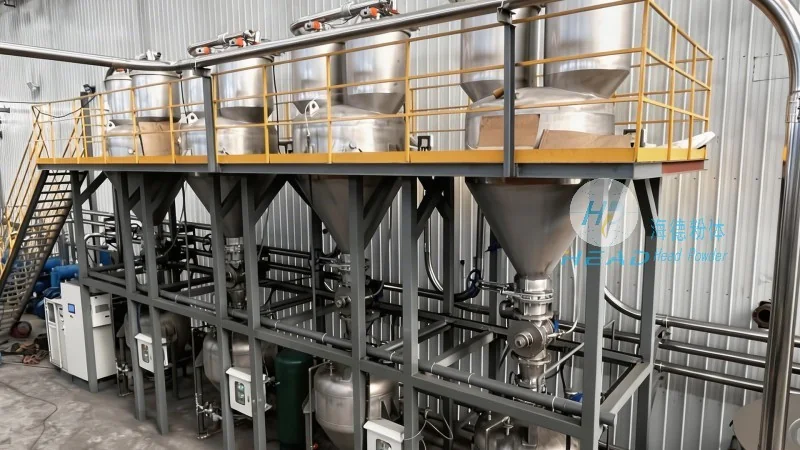
Key Considerations for Efficient and Safe Pharmaceutical Granule Conveying
Efficient and safe operation of pharmaceutical granule conveying systems requires careful consideration of several factors. First, the materials used in the construction of the conveying equipment must be compatible with pharmaceutical products and meet regulatory standards for cleanliness and sterility. Stainless steel is commonly used due to its corrosion resistance and ease of cleaning. Second, the system must be designed to prevent cross-contamination between different batches of materials. This includes features such as sealed connections, air filtration systems, and proper cleaning protocols. Third, the control system must be user-friendly and capable of monitoring and adjusting the conveying process in real-time. This includes sensors for flow rate, temperature, and pressure, as well as alarms for any deviations from normal operation. Finally, regular maintenance and inspection are crucial to ensure the longevity and reliability of the conveying system. HeadPowder emphasizes these considerations in its design and manufacturing processes, ensuring that its conveying systems meet the highest standards of quality and safety.
Conclusion: Enhancing Pharmaceutical Manufacturing with Advanced Conveying Solutions
Pharmaceutical granule material conveying is a complex but essential process in modern pharmaceutical manufacturing. The proper operation of conveying systems directly impacts product quality, regulatory compliance, and overall production efficiency. Shandong HeadPowder Engineering Co., Ltd. plays a vital role in this field by providing advanced, customized conveying solutions that meet the unique needs of pharmaceutical companies. By understanding the operation process and working principles of these systems, manufacturers can optimize their material handling processes and achieve greater efficiency and safety. As the pharmaceutical industry continues to evolve, the importance of reliable conveying systems will only increase, making companies like HeadPowder indispensable partners in the pursuit of high-quality pharmaceutical products.




