HeadPowder, a leading provider in the field of powder handling technology, specializes in inert gas circulation powder pneumatic conveying systems. This article delves into the fundamental working principles and distinctive features of this advanced method for transporting bulk powders, offering insights into its operational mechanisms and practical advantages.
Working Principles of Inert Gas Circulation Powder Pneumatic Conveying
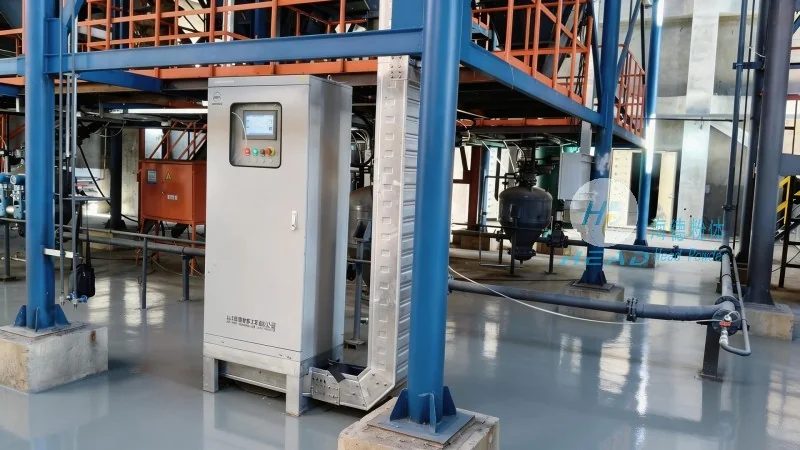
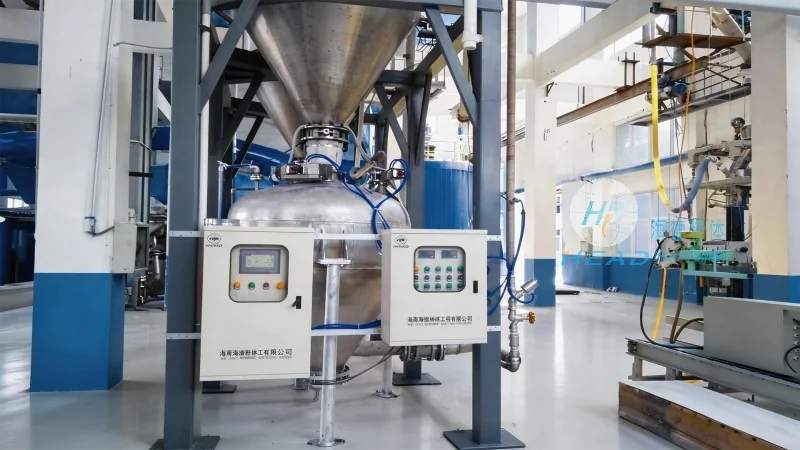
The inert gas circulation powder pneumatic conveying system operates by utilizing a closed-loop system where an inert gas, typically nitrogen or carbon dioxide, is continuously circulated to create a controlled environment. This approach ensures that the powder is conveyed without exposure to atmospheric air, which is crucial for maintaining product integrity, especially for sensitive materials such as pharmaceuticals, food additives, or chemicals that are prone to oxidation or contamination. The system comprises several key components, including a material feed hopper, a conveying pipeline, a gas circulation unit, and a dust collection or filtration system. The process begins with the powder being fed from the hopper into the pipeline. Simultaneously, the inert gas is introduced into the system, creating a flow that propels the powder particles through the pipeline. The gas acts as a carrier, maintaining the powder in a suspended state and preventing it from settling or agglomerating. The closed-loop design ensures that the gas is continuously recycled, minimizing waste and energy consumption. The conveying velocity and pressure are carefully controlled to optimize the transport efficiency while preserving the quality of the conveyed material. The system may also incorporate features such as pressure regulation, temperature control, and particle size monitoring to further enhance performance and product safety.
Key Features of Inert Gas Circulation Powder Pneumatic Conveying
HeadPowder's inert gas circulation powder pneumatic conveying systems offer several unique advantages that set them apart from traditional pneumatic conveying methods. One of the most significant features is the ability to maintain a completely inert atmosphere throughout the conveying process. This is achieved by continuously circulating a dry, filtered inert gas, which effectively isolates the powder from moisture and oxygen in the ambient air. The result is a system that is highly effective in preventing product degradation, cross-contamination, and the formation of dust explosions, making it ideal for handling hazardous or sensitive materials. Another key feature is the energy efficiency of the closed-loop system. By recycling the conveying gas, the system reduces energy consumption compared to open-loop systems that require constant replenishment of fresh air. This not only lowers operational costs but also contributes to a more sustainable and environmentally friendly operation. The system also provides excellent control over the conveying parameters, allowing for precise adjustment of flow rates, pressure, and velocity to match the specific requirements of different powder types and application scenarios. This flexibility makes the system suitable for a wide range of industries, including pharmaceuticals, food processing, chemical manufacturing, and aerospace. Additionally, the inert gas circulation design offers superior dust control and filtration capabilities. The closed system prevents dust from escaping into the environment, reducing the risk of inhalation hazards and ensuring compliance with environmental regulations. The integrated filtration system captures any fine particles, ensuring that the conveyed powder remains clean and free from contaminants. This feature is particularly important for applications where product purity is paramount, such as in the production of high-value pharmaceuticals or specialty chemicals. The system's reliability and durability are further enhanced by the use of high-quality materials and robust construction. HeadPowder employs advanced engineering techniques to design components that can withstand the pressures and temperatures associated with inert gas conveying, ensuring long-term performance and minimal maintenance requirements. The result is a system that delivers consistent, reliable performance with minimal downtime, making it a cost-effective solution for bulk powder handling needs.




