

What is an Intelligent Material Pneumatic Conveying System? And What Are Its Design Principles?
Intelligent material pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of bulk materials in industrial settings. These systems utilize air or gas as the primary medium to move powders, granules, and other particulate materials from one location to another, offering advantages such as reduced contamination, improved safety, and enhanced process control. Understanding the core concepts and design principles behind these systems is crucial for industries seeking to optimize material handling operations.
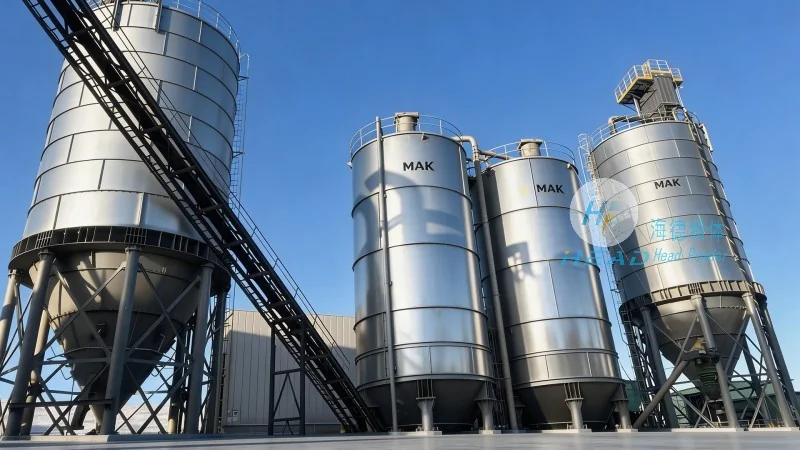
Introduction to Intelligent Material Pneumatic Conveying Systems
At the heart of modern material handling technology lies the intelligent material pneumatic conveying system. Unlike traditional methods that rely on mechanical components like belts or buckets, pneumatic systems employ a pressurized or vacuum environment to transport materials. This approach not only minimizes the risk of product contamination but also allows for the integration of advanced control systems that enable real-time monitoring and adjustment of conveying parameters. The result is a more flexible and adaptable material handling solution suitable for a wide range of applications, from pharmaceuticals and food processing to chemical manufacturing and mining.
About HeadPowder: A Leading Provider of Pneumatic Conveying Solutions
HeadPowder, a prominent player in the material handling industry, specializes in the design, manufacturing, and implementation of intelligent pneumatic conveying systems. With a strong presence in Shandong, China, HeadPowder Engineering Co., Ltd. has built a reputation for delivering high-quality, customized solutions tailored to the unique needs of each client. The company's commitment to innovation and customer satisfaction has positioned it as a trusted partner for businesses seeking to enhance their material handling processes. By leveraging advanced engineering and cutting-edge technology, HeadPowder ensures that its systems meet the highest standards of performance, reliability, and efficiency.
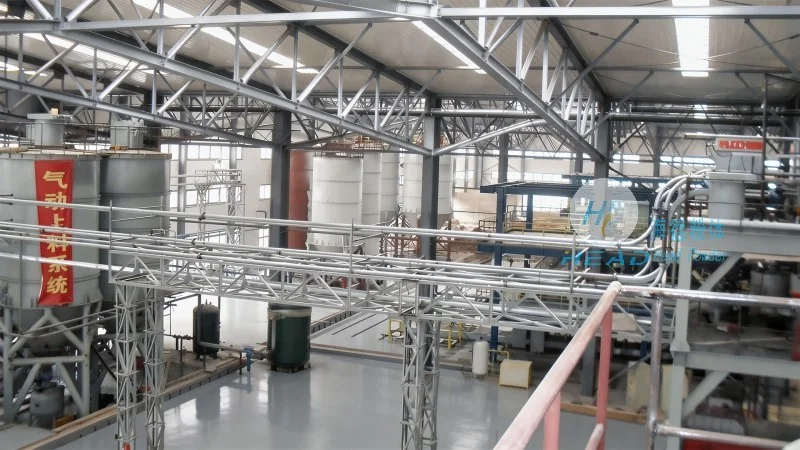
Key Design Principles of Intelligent Pneumatic Conveying Systems
The design of an intelligent material pneumatic conveying system is governed by several critical principles that ensure optimal performance and longevity. These principles include the selection of appropriate air velocity and pressure, the proper sizing of ductwork and components, and the integration of advanced control mechanisms. The system's design must also account for the physical properties of the material being conveyed, such as particle size, density, and moisture content, to ensure efficient transport without causing degradation or blockages. Additionally, the incorporation of features like automatic cleaning and maintenance reminders contributes to the system's overall reliability and ease of operation.
Technical Components and Their Functions
Intelligent material pneumatic conveying systems consist of several key components, each playing a vital role in the overall operation. The primary components include the air compressor or vacuum pump, which generates the necessary pressure or vacuum to move the material; the conveying ducts, which serve as the pathway for the material and air; and the control valves and sensors, which regulate the flow and monitor system performance. Other essential components may include cyclone separators, filters, and material feeders, which help to separate the conveyed material from the air and control the feed rate. The integration of these components into a cohesive system requires careful engineering to ensure smooth operation and minimal downtime.
Benefits of Implementing an Intelligent Pneumatic Conveying System
Adopting an intelligent material pneumatic conveying system offers numerous benefits for industrial operations. These systems significantly reduce labor costs by automating the material handling process, allowing workers to focus on other critical tasks. They also minimize product loss and contamination, which is particularly important in industries where product purity is paramount, such as pharmaceuticals and food processing. Furthermore, the ability to monitor and adjust conveying parameters in real time enhances process control and reduces the risk of material blockages or system failures. The energy efficiency of modern pneumatic systems, combined with their compact design, makes them an attractive solution for facilities with limited space or high energy consumption concerns.
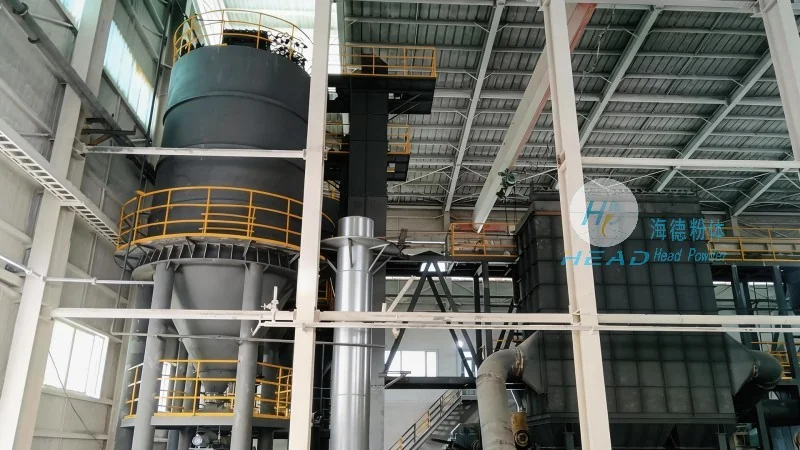
Application Examples and Industry Use Cases
The versatility of intelligent material pneumatic conveying systems makes them suitable for a wide range of applications across various industries. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring strict contamination control and compliance with regulatory standards. In the food processing sector, they are employed to handle powders like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. The chemical manufacturing industry utilizes pneumatic conveying systems to transport raw materials and finished products, while the mining and mineral processing sectors benefit from their ability to handle abrasive and heavy materials. Regardless of the industry, the consistent and reliable performance of these systems contributes to improved productivity and operational efficiency.
Conclusion and Future Outlook
Intelligent material pneumatic conveying systems represent a significant advancement in material handling technology, offering industries a reliable and efficient solution for transporting bulk materials. With the integration of advanced control systems and customized design, these systems continue to evolve, meeting the growing demands of modern industrial operations. As businesses seek to optimize their processes and enhance productivity, the adoption of intelligent pneumatic conveying systems remains a strategic investment. HeadPowder Engineering Co., Ltd., with its expertise and commitment to quality, stands ready to provide tailored solutions that address the unique challenges of each client, ensuring long-term success and operational excellence.