Ammonia fertilizer is a crucial component in modern agricultural practices, providing essential nutrients to crops and enhancing soil fertility. The efficient transportation of ammonia fertilizer from production facilities to storage or application sites is critical for maintaining supply chain integrity and ensuring timely delivery to farmers. This is where specialized equipment like the ammonia fertilizer material conveying line plays a pivotal role. In this article, we will explore the fundamental aspects of such systems, including their design principles and the key components that enable their operation.
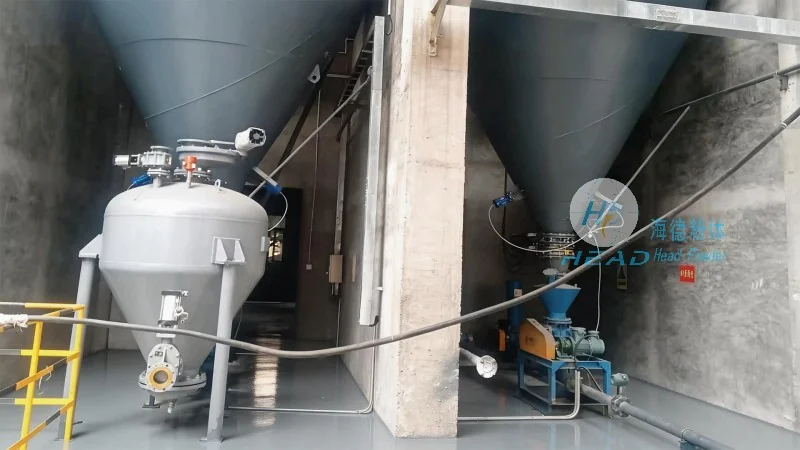
Understanding the Ammonia Fertilizer Material Conveying Line
The ammonia fertilizer material conveying line is a sophisticated system engineered to handle the unique properties of ammonia-based fertilizers. These materials are often in liquid or slurry form, requiring specialized equipment to transport them safely and efficiently. The primary goal of this line is to move ammonia fertilizer from its point of production to storage tanks, distribution centers, or directly to agricultural fields. The design of such a system must account for factors like the corrosive nature of ammonia, the need for precise temperature control, and the requirement for minimal product loss during transit.
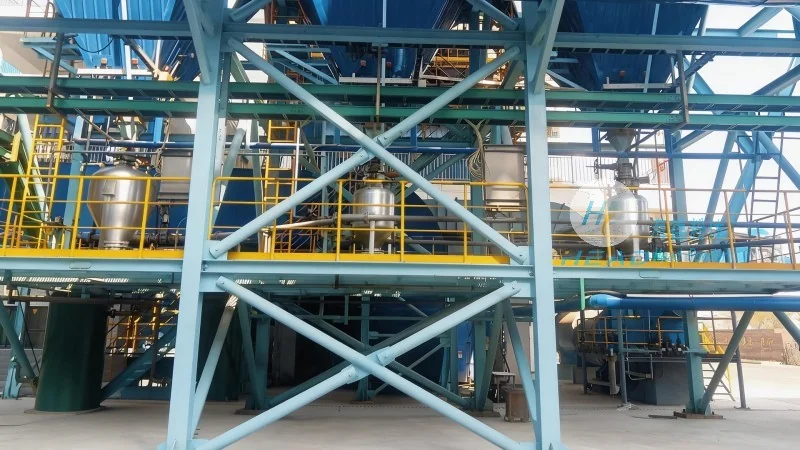
Key Design Principles for Efficient Conveying
Several critical design principles underpin the effectiveness of an ammonia fertilizer material conveying line. First, the system must be constructed from materials that are resistant to corrosion, as ammonia is highly corrosive and can degrade many common metals over time. Stainless steel, special alloys, or coated components are typically used to ensure durability and longevity. Second, temperature control is paramount. Ammonia fertilizer often requires specific temperature ranges to maintain its stability and prevent degradation. The conveying line must incorporate heating or cooling elements as needed to maintain optimal conditions throughout the process. Third, the system must be designed for minimal pressure drop and energy efficiency. This involves selecting appropriate pump types, pipe diameters, and flow control mechanisms to minimize energy consumption while maximizing throughput. Fourth, safety is a top priority. Given the hazardous nature of ammonia, the conveying line must include safety features such as pressure relief valves, leak detection systems, and emergency shutdown protocols to protect personnel and the environment.
Core Components of the Conveying Line
The ammonia fertilizer material conveying line consists of several interconnected components that work in harmony to achieve the desired results. The primary components include a pump system, which is responsible for moving the ammonia fertilizer through the pipeline. Depending on the specific application, this may be a centrifugal pump, a positive displacement pump, or a combination of both. The pump is typically equipped with a motor that provides the necessary power to drive the flow. Next, the pipeline itself, often made of corrosion-resistant materials like stainless steel or polyethylene, forms the main conduit for the material. The pipeline is usually equipped with valves to control flow direction and pressure, and may include fittings such as elbows, tees, and reducers to facilitate changes in direction or size. Additionally, the system may include storage tanks or silos to hold the ammonia fertilizer before or after processing. These tanks are designed to maintain the material's temperature and pressure within safe operating limits. Finally, the conveying line may include monitoring and control systems, such as flow meters, pressure gauges, and temperature sensors, to provide real-time data on the system's performance and enable operators to make adjustments as needed.
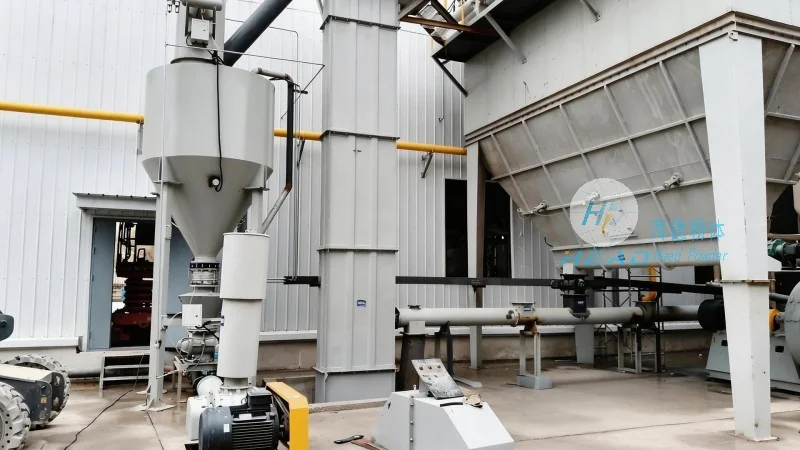
HeadPowder Engineering: A Leader in Ammonia Fertilizer Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. is a prominent manufacturer and supplier of ammonia fertilizer material conveying lines, with a strong reputation for quality and reliability. Based in Shandong, China, the company has extensive experience in designing and manufacturing equipment tailored to the unique needs of the fertilizer industry. HeadPowder's expertise lies in creating customized conveying solutions that meet the specific requirements of each client, whether it's for large-scale industrial production or smaller agricultural operations. The company's products are known for their durability, efficiency, and adherence to international safety standards. By leveraging advanced engineering techniques and a deep understanding of ammonia fertilizer properties, HeadPowder ensures that its conveying lines deliver optimal performance and longevity. The company's commitment to customer satisfaction and technical excellence has made it a trusted partner for businesses in the agricultural and fertilizer sectors worldwide.




