HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth materials. These systems are crucial in industries where efficient and reliable material transport is essential, ensuring optimal performance and safety in material processing operations.
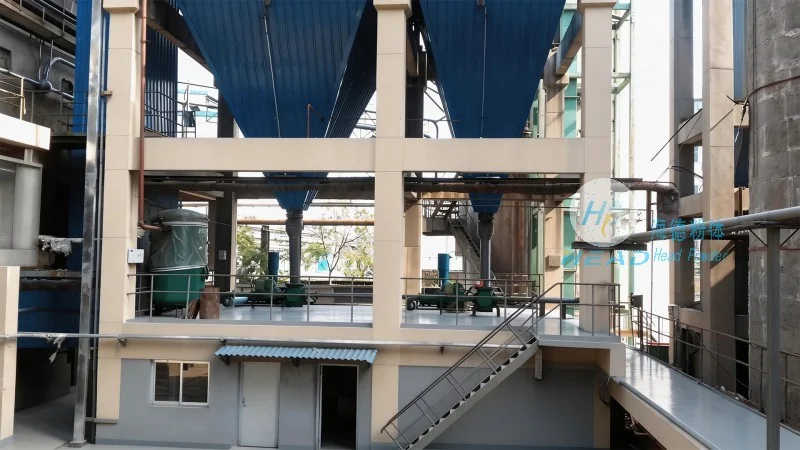
Classification of Rare Earth Pneumatic Conveying Systems
There are primarily two main categories of pneumatic conveying systems used for rare earth materials: dilute phase and dense phase systems. Dilute phase systems operate by transporting material in a low concentration of particles suspended in a gas stream, typically at high velocities. This method is suitable for long-distance transport and is commonly used in applications where the material is non-abrasive and requires minimal pressure. Dense phase systems, on the other hand, transport material in a higher concentration, often at lower velocities and higher pressure, which is ideal for handling abrasive or sensitive materials that require gentle handling to prevent degradation or damage.
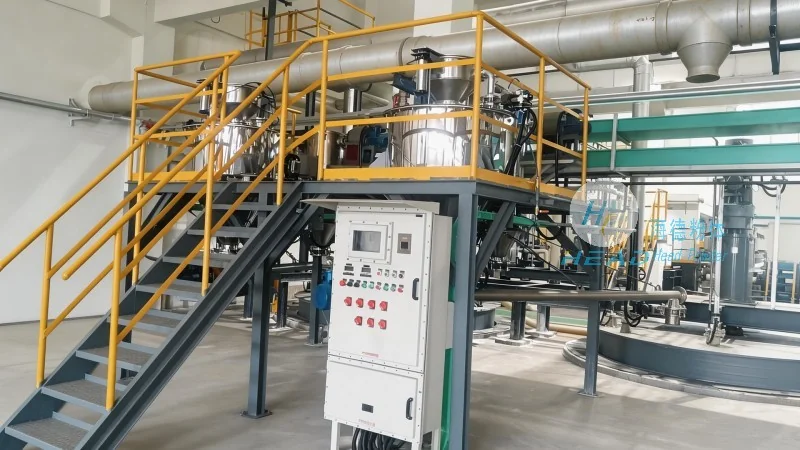
Key Components of Rare Earth Pneumatic Conveying Systems
The core components of a rare earth pneumatic conveying system include the material feed hopper, the conveying pipeline, the air supply system (including blowers or compressors), and the control system. The feed hopper is designed to store and meter the rare earth material into the system, ensuring a consistent flow rate. The conveying pipeline is constructed from materials resistant to corrosion and wear, such as stainless steel or special alloys, to withstand the abrasive nature of rare earth powders. The air supply system provides the necessary pressure and volume of air to move the material through the pipeline. The control system monitors and regulates the flow of material and air, ensuring smooth operation and preventing system failures.
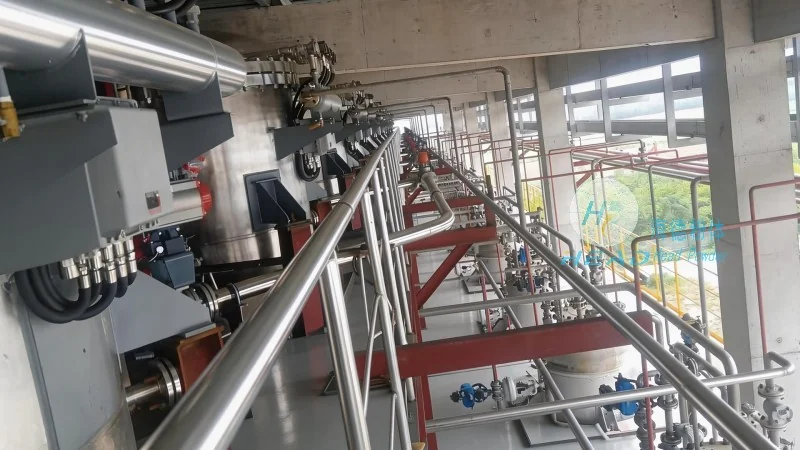
Application and Benefits in Rare Earth Processing
These systems are widely utilized in the rare earth processing industry for tasks such as material transfer from storage silos to processing units, transportation between different stages of production, and handling of raw materials or finished products. The benefits of using pneumatic conveying systems include improved safety by eliminating manual handling of hazardous materials, increased efficiency through automated operation, and reduced maintenance costs due to the absence of mechanical parts in direct contact with the material. Additionally, these systems offer flexibility in layout, allowing for easy integration into existing production facilities without significant structural modifications.
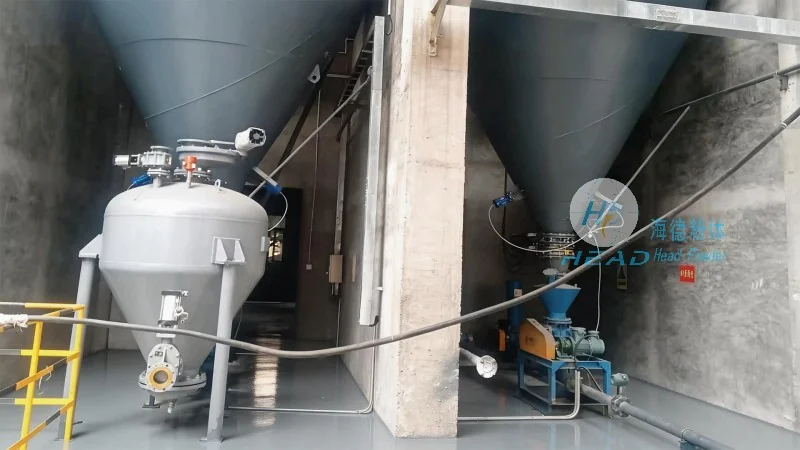
Customization and Technical Support from HeadPowder
HeadPowder Engineering Co., Ltd. offers customized solutions tailored to the specific needs of clients in the rare earth industry. With a team of experienced engineers and technicians, the company provides comprehensive technical support, from system design and installation to ongoing maintenance and troubleshooting. The company's expertise ensures that the pneumatic conveying systems are optimized for the unique characteristics of rare earth materials, such as their density, particle size, and chemical properties, to achieve maximum efficiency and reliability.




