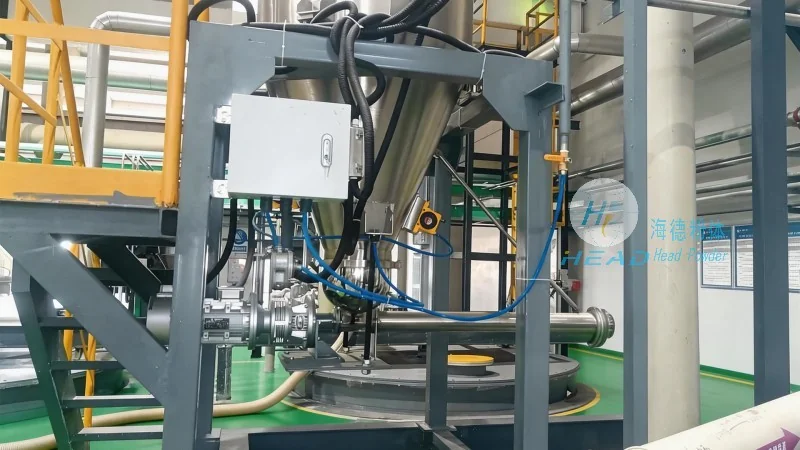
For industrial facilities dealing with bulk materials, efficient and safe material handling is paramount. A tonne bag dust-free loading station equipped with a pneumatic conveying system represents a sophisticated solution designed to streamline the process of receiving and transferring bulk materials while maintaining a clean, controlled environment. This system integrates several key components to achieve its objectives, including a dust-free enclosure, material handling equipment, and a pneumatic conveying network. The primary goal is to minimize dust emissions, enhance safety, and improve operational efficiency in material handling operations.
About HeadPowder: A Leader in Material Handling Solutions
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a prominent provider of advanced material handling equipment and systems. With a focus on innovation and customer-centric solutions, HeadPowder specializes in designing and manufacturing equipment that meets the stringent requirements of modern industrial applications. The company’s expertise lies in developing systems that ensure safety, efficiency, and compliance with environmental standards, making them a trusted partner for businesses seeking reliable material handling solutions.
Design Principles of Tonne Bag Dust-Free Loading Stations with Pneumatic Conveying
The design of a tonne bag dust-free loading station with a pneumatic conveying system is based on several critical principles aimed at optimizing performance and safety. The primary design principle is to create a sealed environment that prevents dust from escaping into the surrounding area, thereby maintaining a clean and safe working environment. This is achieved through the use of a robust dust enclosure that houses the material handling equipment and the pneumatic conveying components.
Another key design principle is the efficient transfer of bulk materials from the tonne bag to the pneumatic conveying system. The system typically includes a hopper or a loading mechanism that can open the tonne bag and discharge the material into the conveying line. This process is often automated to minimize manual handling and reduce the risk of dust exposure. The design also considers the material properties, such as particle size, moisture content, and flowability, to ensure that the conveying system can handle the specific characteristics of the bulk material without clogging or loss of efficiency.
The pneumatic conveying system itself is a critical component of the design. It uses air to transport the bulk material from the loading station to the processing or storage areas. The system can be either positive pressure or negative pressure, depending on the application and material characteristics. Positive pressure systems blow air through the conveying line, while negative pressure systems draw air and material through the line. The design of the conveying system includes considerations such as the air velocity, the diameter of the conveying line, and the length of the line to ensure that the material is transported efficiently and without degradation.
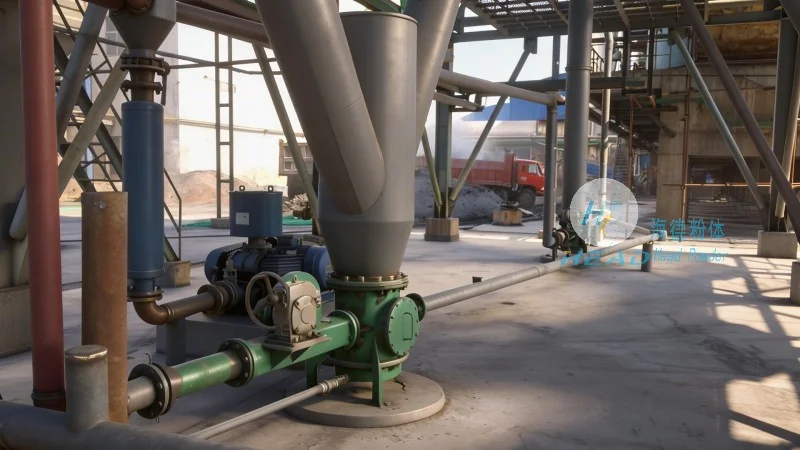
Additionally, the design incorporates safety features to protect operators and the environment. This includes dust collection systems, such as filters or cyclones, that capture any dust that may escape from the loading station. The system may also include sensors and controls to monitor the operation and alert operators in case of any issues, such as blockages or excessive dust levels. The overall design aims to balance efficiency with safety and environmental compliance, ensuring that the system operates reliably and meets the requirements of modern industrial standards.
Key Components and Their Functions
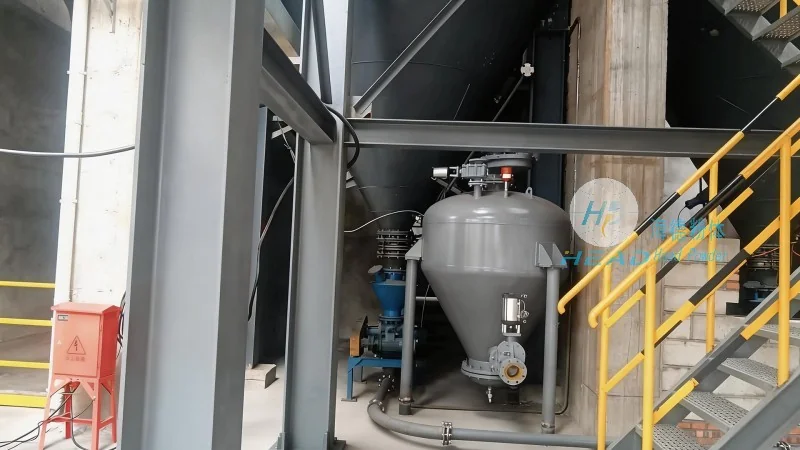
A tonne bag dust-free loading station with a pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. The dust enclosure is the primary component, providing a sealed environment that contains dust and prevents it from dispersing into the workplace. This enclosure is typically made of durable materials, such as stainless steel or high-quality plastic, to withstand the demands of industrial use and resist corrosion.
Inside the enclosure, the material handling equipment includes a tonne bag opening mechanism, often a hydraulic or mechanical system that safely opens the bag and discharges the material into a hopper. The hopper then feeds the material into the pneumatic conveying system. The conveying system comprises a blower or compressor, which generates the air pressure needed to move the material, and a series of pipes or ducts that transport the material to the destination. The system may also include a dust filter or cyclone to capture any particles that escape during the conveying process, ensuring that the air released back into the environment is clean.
The control system is another essential component, which manages the operation of the entire station. It includes sensors to monitor the level of material in the hopper, the pressure in the conveying line, and the status of the dust collection system. The control system can be automated to adjust the operation based on real-time conditions, such as changes in material flow or pressure drops, ensuring optimal performance and preventing issues like blockages or overloading.
Benefits and Applications
The implementation of a tonne bag dust-free loading station with a pneumatic conveying system offers numerous benefits for industrial operations. One of the most significant advantages is the reduction of dust exposure, which not only improves the health and safety of workers but also helps in maintaining a clean and organized workplace. This is particularly important for materials that are known to be hazardous or cause respiratory issues if inhaled.
Another benefit is the improvement in operational efficiency. The automated nature of the system reduces the need for manual handling, which can be time-consuming and labor-intensive. This leads to faster material transfer and increased productivity. Additionally, the system can handle a wide range of bulk materials, from powders to granules, making it versatile for various industrial applications.
The system is widely used in industries such as pharmaceuticals, food processing, chemicals, and mining. In pharmaceutical manufacturing, for example, the dust-free environment is crucial to maintain product purity and comply with regulatory standards. In food processing, the system ensures that the materials are handled hygienically, preventing contamination and ensuring food safety. In chemical and mining industries, the system helps in safely transferring hazardous or abrasive materials, reducing the risk of accidents and environmental contamination.
Conclusion
A tonne bag dust-free loading station with a pneumatic conveying system is a highly effective solution for bulk material handling, combining efficiency, safety, and environmental responsibility. The design principles behind such systems focus on creating a sealed environment, efficient material transfer, and reliable operation, all while minimizing dust emissions and ensuring compliance with safety and environmental standards. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement these systems to enhance their material handling processes and achieve better operational outcomes.




