The sulfur tablet material conveying line is a specialized system designed for the efficient transportation of sulfur tablets within industrial settings. As a key component in the production and processing of sulfur-based products, this line ensures smooth material flow from one processing stage to another, enhancing overall operational efficiency and product quality. The system integrates various mechanical and control components to achieve precise and reliable movement of the tablets, catering to the specific requirements of sulfur tablet manufacturing processes.
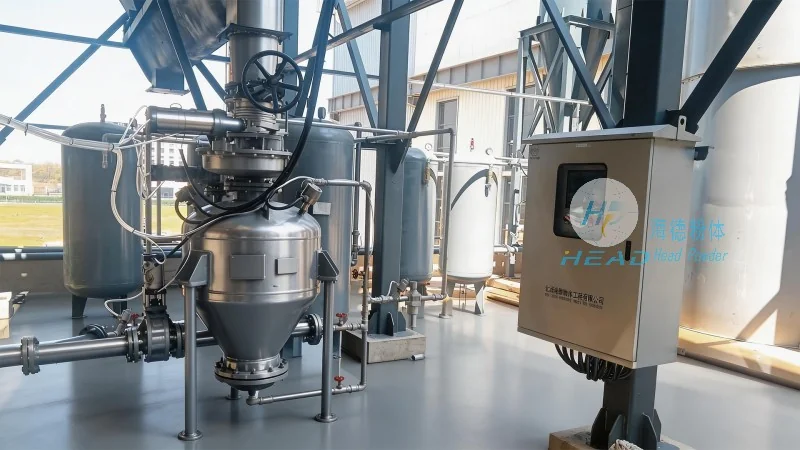
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the manufacturer of this advanced conveying line, is a leading enterprise based in Shandong, China. With a strong commitment to technological innovation and quality assurance, the company specializes in the design, development, and implementation of industrial material handling solutions. The company's facilities and expertise are dedicated to delivering high-performance equipment tailored to the needs of the chemical and pharmaceutical industries, ensuring that clients receive reliable and efficient systems for their material processing requirements.
Key Components and Structure of the Conveying Line
The sulfur tablet material conveying line typically consists of several interconnected components that work in harmony to facilitate material movement. These components include feed hoppers, conveyor belts or rollers, control systems, and discharge mechanisms. The feed hopper is responsible for receiving the sulfur tablets from the production line, ensuring a consistent supply of material. The conveyor system, which may feature adjustable speed and direction controls, transports the tablets through the line, while the control system monitors and regulates the entire process to maintain optimal performance. The discharge mechanism then delivers the tablets to the next processing stage or storage area, completing the material handling cycle.
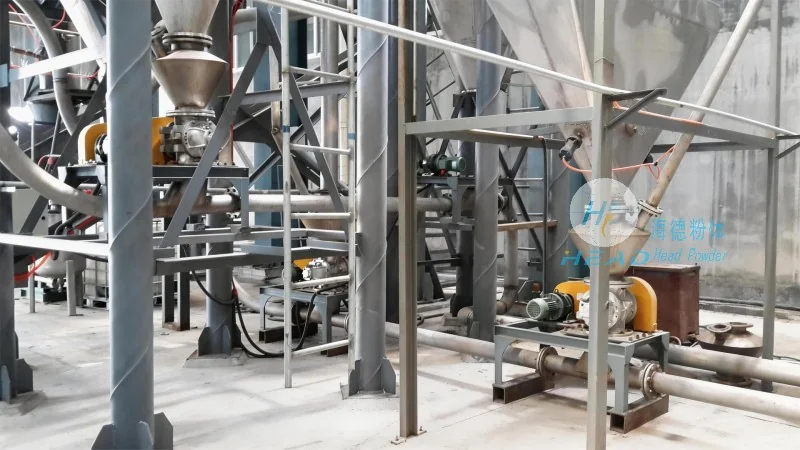
Operation Process of the Conveying Line
The operation of the sulfur tablet material conveying line begins with the loading of sulfur tablets into the feed hopper. The hopper is designed to hold a sufficient quantity of tablets, preventing interruptions in the material flow. Once loaded, the tablets are released into the conveyor system, where they are transported along the designated path. The conveyor speed is controlled by the system's control unit, which adjusts based on real-time operational parameters such as tablet quantity and processing requirements. As the tablets move through the line, they may undergo additional processing steps, such as sorting or inspection, before reaching the discharge point. The control system continuously monitors the line's performance, ensuring that any deviations from the set parameters are immediately addressed to maintain consistent operation.
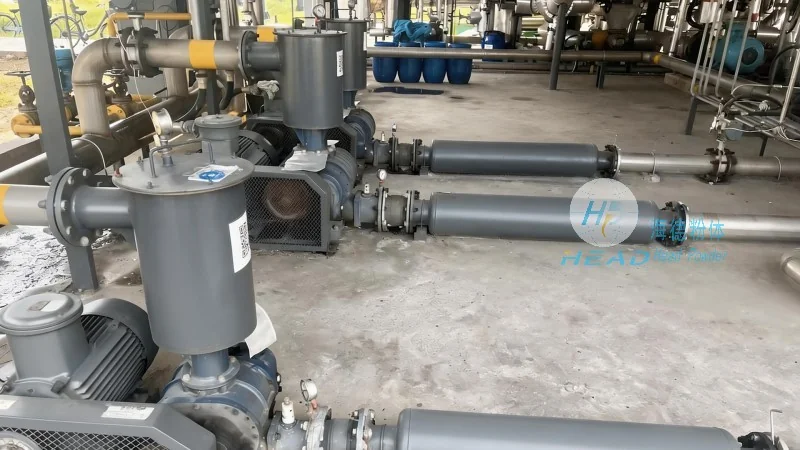
Working Principle of the Conveying Line
The working principle of the sulfur tablet material conveying line is based on mechanical energy transfer and precise control mechanisms. The system utilizes motor-driven components to power the conveyor, which moves the tablets through the line via friction or gravity, depending on the design. The control system, often equipped with sensors and feedback loops, ensures that the conveyor operates at the optimal speed and direction, preventing overloading or bottlenecks. The sensors detect the presence and position of the tablets, providing real-time data to the control unit, which adjusts the system's performance accordingly. This closed-loop control system enhances the line's efficiency and reliability, minimizing downtime and maximizing productivity. Additionally, the line is designed with safety features to protect operators and equipment, ensuring compliance with industrial safety standards.
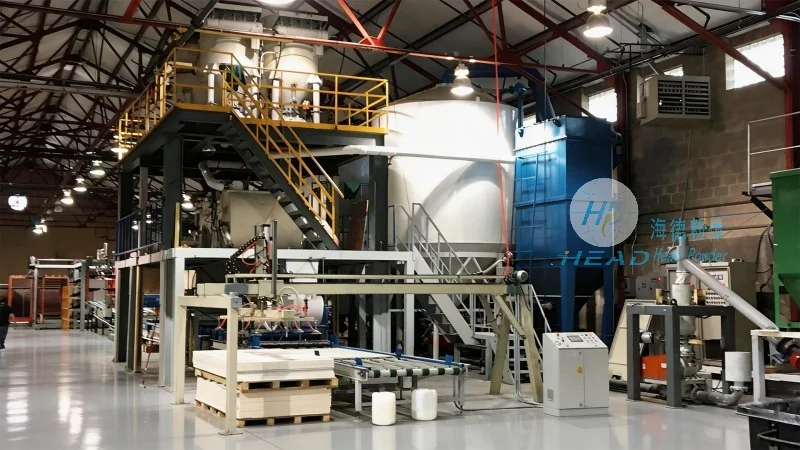
Advantages and Applications of the Conveying Line
The sulfur tablet material conveying line offers several advantages that make it an ideal solution for industrial applications. Its ability to handle a high volume of tablets with minimal human intervention reduces labor costs and improves operational efficiency. The system's design allows for easy integration with existing production lines, enabling seamless material flow and process optimization. Additionally, the line's durability and low maintenance requirements contribute to long-term cost savings for the end-user. The applications of this conveying line are widespread, including in the chemical industry for sulfur-based product processing, pharmaceutical manufacturing for tablet handling, and other industries where bulk material transportation is required. The system's adaptability to different tablet sizes and shapes further enhances its versatility, making it suitable for a variety of industrial settings.
Conclusion
In conclusion, the sulfur tablet material conveying line is a sophisticated and efficient system that plays a crucial role in the production and processing of sulfur tablets. Developed by Shandong HeadPowder Engineering Co., Ltd., this line combines advanced technology and robust design to ensure reliable material handling. The operation process and working principle of the line are carefully engineered to meet the demands of modern industrial operations, providing a solution that enhances productivity, reduces costs, and improves product quality. As a key component in the supply chain of sulfur-based products, this conveying line is essential for maintaining smooth and efficient operations in various industrial applications.




