Urea granule material handling systems are critical components in the agricultural and chemical industries, designed to efficiently transport and manage urea granules from production sites to storage or distribution points. These systems ensure smooth and reliable operation, minimizing downtime and optimizing material flow. As a key player in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing and implementing advanced solutions tailored to the unique demands of urea granule handling.
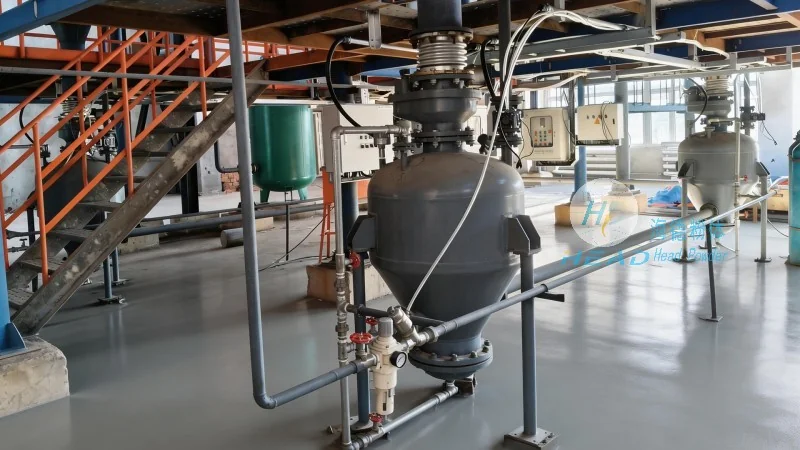
Key Components of the Urea Granule Material Handling System
The urea granule material handling system typically consists of several essential components that work in tandem to achieve efficient material transport. These components include feeders, conveyors, storage silos, and control systems. Each component plays a vital role in the overall operation, ensuring that urea granules are moved safely and effectively. The system is engineered to handle the specific characteristics of urea granules, such as their size, density, and flowability, which are crucial for maintaining system performance.
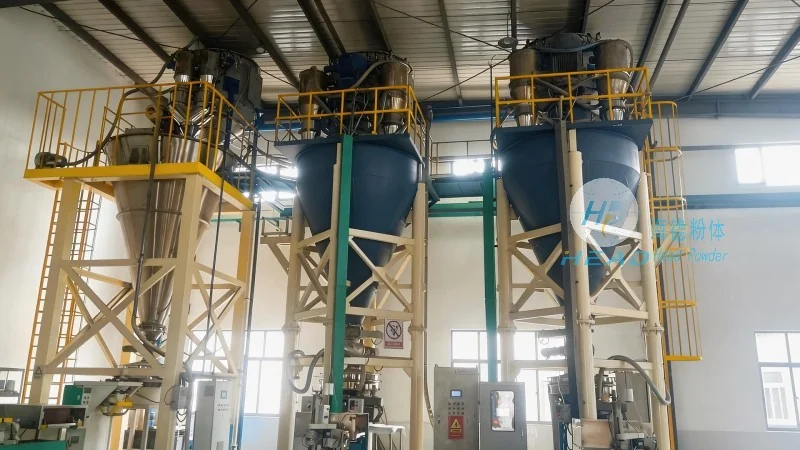
Operation Process of the Urea Granule Material Handling System
The operation process of the urea granule material handling system begins with the loading of urea granules into the storage silo. From there, the material is fed into the conveyor system through a feeder, which regulates the flow rate to match the system's requirements. The conveyor then transports the urea granules to the desired destination, such as a loading dock or a storage container. The control system monitors the entire process, adjusting parameters like speed and flow rate as needed to maintain optimal performance. This integrated approach ensures that the system operates smoothly and efficiently, minimizing the risk of material blockages or other operational issues.
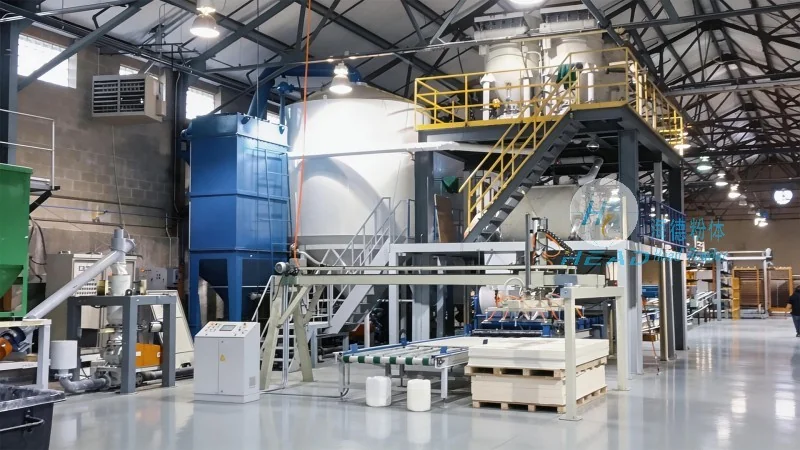
Working Principle of the Urea Granule Material Handling System
The working principle of the urea granule material handling system is based on mechanical and hydraulic systems that work together to move the granules. The feeder uses a rotating mechanism to discharge the urea granules into the conveyor, which then transports them via a series of rollers or belts. The storage silo provides a buffer to regulate the flow of material, ensuring a consistent supply to the conveyor. The control system uses sensors and feedback mechanisms to adjust the feeder speed and conveyor speed, maintaining the desired flow rate. This closed-loop control system ensures that the system operates at peak efficiency, adapting to changes in material volume or system conditions.
Advantages of the Urea Granule Material Handling System
Implementing a urea granule material handling system offers several advantages for industrial operations. Firstly, it enhances operational efficiency by reducing manual handling and minimizing downtime. The automated system ensures consistent material flow, which improves overall productivity. Secondly, it improves safety by eliminating the need for manual handling of heavy or potentially hazardous materials. The system also reduces the risk of material loss or contamination, maintaining product quality. Additionally, the system's modular design allows for easy expansion or modification to accommodate changing production needs. These benefits make the urea granule material handling system a valuable investment for companies in the agricultural and chemical sectors.
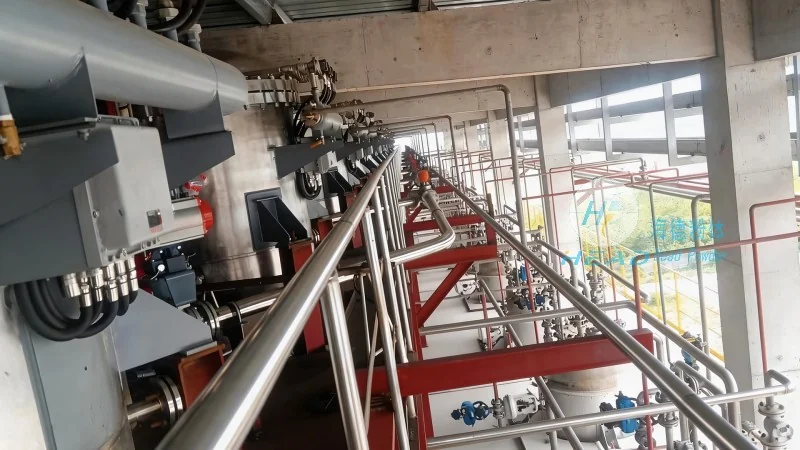
Conclusion
Urea granule material handling systems are essential for efficient and reliable transport of urea granules in industrial settings. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions that incorporate advanced technology and robust design to meet the specific needs of urea granule handling. By understanding the operation process and working principle of these systems, industries can optimize their material handling operations, improve productivity, and ensure safety. The integration of feeders, conveyors, and control systems in a coordinated manner ensures that urea granules are moved efficiently from production to storage or distribution, supporting the smooth operation of agricultural and chemical processes.




