Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer specializing in pneumatic conveying equipment for bulk materials like stone, coal powder, and other powders. Headquartered in Shandong, China, the company serves industries such as mining, power generation, and chemical processing. This article explores the fundamental principles behind stone, coal powder, and bulk material pneumatic conveying machines, as well as the key characteristics of their working environments.
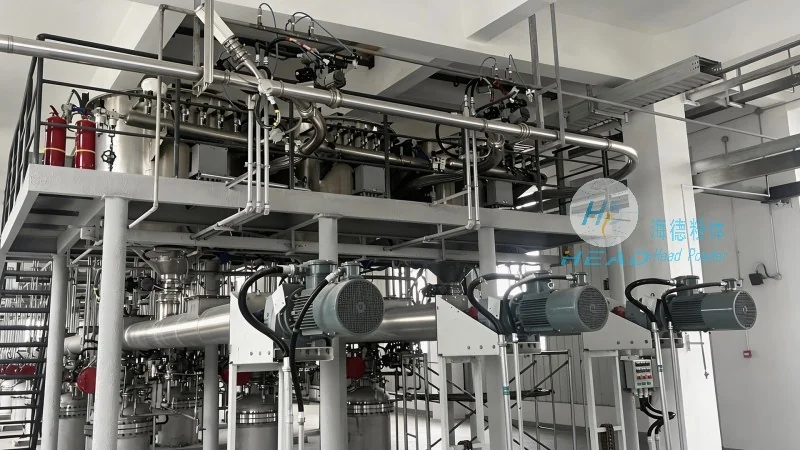
Overview of Pneumatic Conveying Systems for Bulk Materials
Pneumatic conveying machines are essential for efficiently transporting dry, granular, or powdery materials over short to medium distances. These systems utilize air pressure to move materials through a pipeline network, eliminating the need for mechanical components like belts or buckets. The primary goal is to achieve a seamless, continuous flow of material while minimizing downtime and operational costs. For applications involving stone, coal powder, and other bulk materials, specialized designs are required to handle the unique physical properties of each material, such as particle size, density, and moisture content.
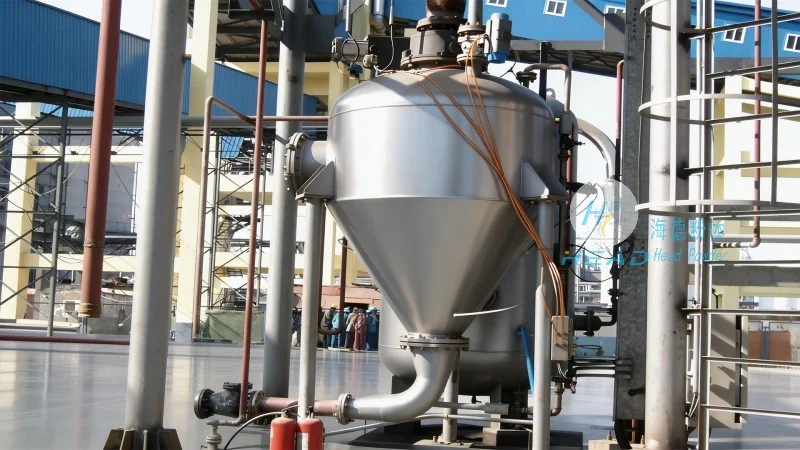
The Working Principle of Pneumatic Conveying Machines
The core principle of pneumatic conveying is the use of air as a medium to transport solid materials. There are two main types of pneumatic conveying systems: suction (or vacuum) and pressure systems. Suction systems draw material into the pipeline using a vacuum created by a fan or blower, while pressure systems push material through the pipeline using compressed air. In the case of stone and coal powder, a combination of both suction and pressure may be employed to optimize material transport efficiency. The machine typically consists of a hopper, a conveying line, a fan or blower, and a discharge outlet. The material is first loaded into the hopper, where it is then drawn or pushed into the conveying line by the air flow. The air velocity within the pipeline must be sufficient to keep the material suspended and prevent it from settling or clogging the system.
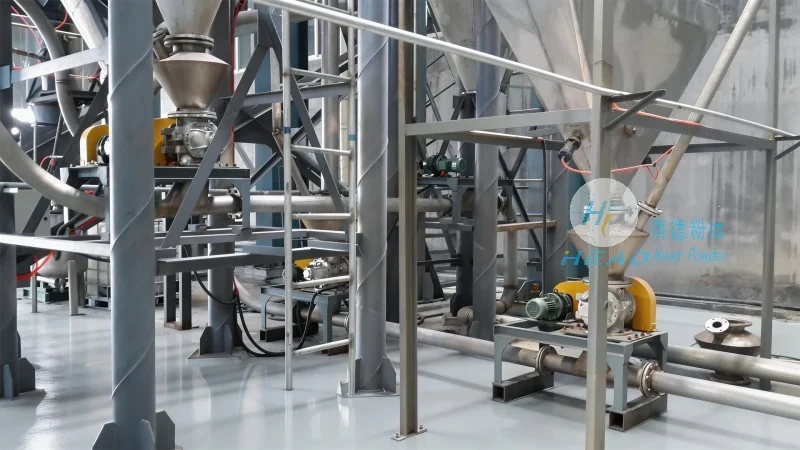
Key Features and Advantages of Stone, Coal Powder, and Bulk Material Pneumatic Conveying Machines
When handling stone, coal powder, and other bulk materials, pneumatic conveying machines offer several advantages over traditional methods. One of the most significant benefits is the ability to transport materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important in industries like mining and power generation, where dust can pose health risks and environmental concerns. Additionally, pneumatic conveying systems are highly efficient, as they can transport large volumes of material over long distances with minimal energy consumption. The continuous operation of these machines also reduces labor costs and increases productivity compared to manual or mechanical handling methods.
Working Scene Characteristics and Applications
The working scene characteristics of pneumatic conveying machines for stone, coal powder, and bulk materials vary depending on the specific industry and application. In mining operations, these machines are commonly used to transport crushed stone or coal from storage silos to processing facilities or to transfer materials between different stages of the mining process. The harsh environmental conditions, such as high temperatures and dust, require robust construction materials and reliable components to ensure long-term operation. In power plants, pneumatic conveying systems are used to transport coal powder from storage bunkers to boilers, where it is burned to generate electricity. The high temperature and pressure in these environments demand specialized materials and design considerations to prevent corrosion and ensure safety. In chemical processing plants, these machines are used to transport powders like limestone or clay, which are essential raw materials for various chemical products. The need for precise material control and minimal contamination in chemical processes makes pneumatic conveying an ideal solution.
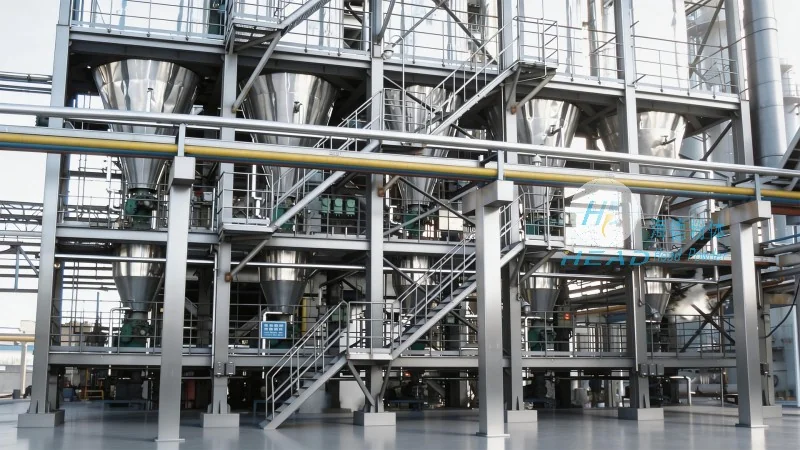
Customization and Technical Support from HeadPowder
Shandong HeadPowder Engineering Co., Ltd. understands that each industrial application has unique requirements. Therefore, the company offers customized pneumatic conveying solutions tailored to the specific needs of clients. Whether it's a suction system for handling fine coal powder or a pressure system for transporting large stone particles, headpowder's engineering team works closely with clients to design and manufacture equipment that meets their exact specifications. The company also provides comprehensive technical support, including installation, maintenance, and troubleshooting services, to ensure that the pneumatic conveying machines operate at peak efficiency. With a commitment to quality and customer satisfaction, headpowder has established itself as a trusted partner in the bulk material handling industry.




