HeadPowder, a leading enterprise in the field of material handling technology, specializes in the design, manufacturing, and integration of advanced systems for transporting and processing ash materials. The purified ash material handling system equipment developed by the company is engineered to meet the stringent requirements of modern industrial applications, ensuring efficient, safe, and reliable operation in various working environments.
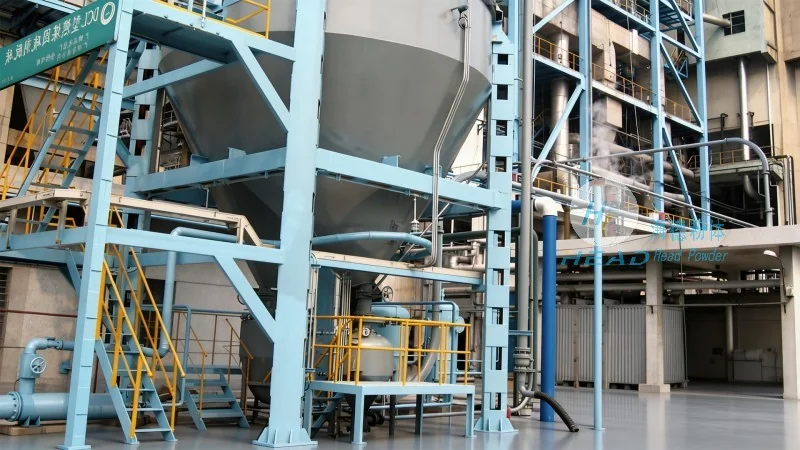
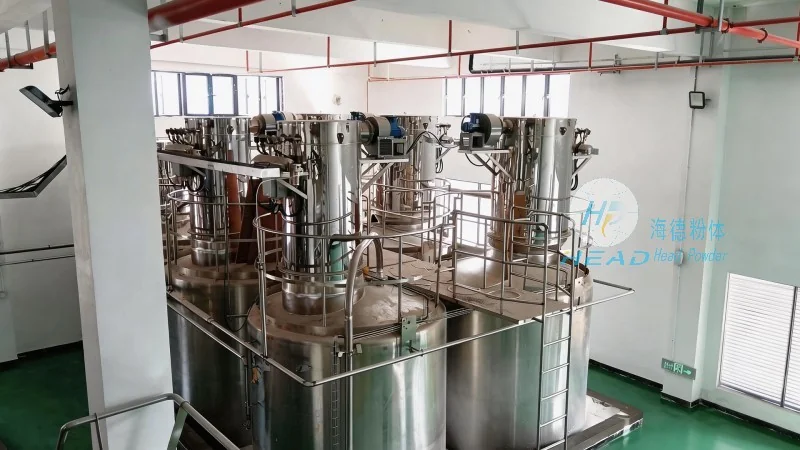
Principles of the Purified Ash Material Handling System
The core principle of the purified ash material handling system lies in its integrated approach to material transport, filtration, and control. The system employs advanced pneumatic or mechanical conveying technologies to move ash materials from source points to designated processing or disposal locations. A key component is the air purification and filtration unit, which ensures that the material is handled in a clean, dust-free environment, reducing health risks and environmental contamination. The system also incorporates intelligent control mechanisms, such as PLC (Programmable Logic Controller) systems, that monitor and adjust operational parameters in real-time, optimizing performance and energy efficiency. Additionally, the design incorporates corrosion-resistant materials and robust construction to withstand the harsh conditions associated with ash handling, including high temperatures, moisture, and abrasive particles.
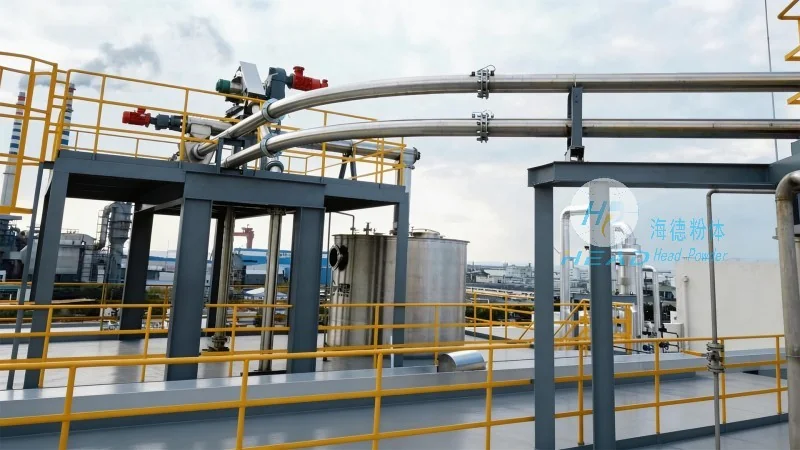
Working Scene Characteristics of the System
The purified ash material handling system is tailored to operate in diverse industrial settings, each with unique challenges and requirements. In power plants, for instance, the system is used to transport fly ash and bottom ash from boilers to storage silos or waste treatment facilities. The working scene is characterized by high material volumes, continuous operation, and the need for precise control to maintain plant efficiency. The system’s ability to handle large quantities of ash while maintaining low dust emissions is critical in these environments, as it directly impacts air quality and regulatory compliance. In cement and construction material production facilities, the system is employed to convey raw ash materials to grinding mills or mixing stations. Here, the working scene involves processing ash as a secondary raw material, requiring the system to be compatible with existing production lines and capable of handling varying ash compositions. The system’s modular design allows for easy integration into existing infrastructure, minimizing downtime and operational disruptions. Furthermore, in waste management and recycling facilities, the purified ash system is used to transport ash from incineration processes to recycling or disposal sites. The working scene in this context emphasizes safety, as ash materials may contain hazardous components, and the system’s enclosed conveying and filtration features are essential to prevent exposure and contamination. The system’s adaptability to different working scenarios is a key advantage, enabling it to be deployed in both new construction projects and retrofit applications across various industries.
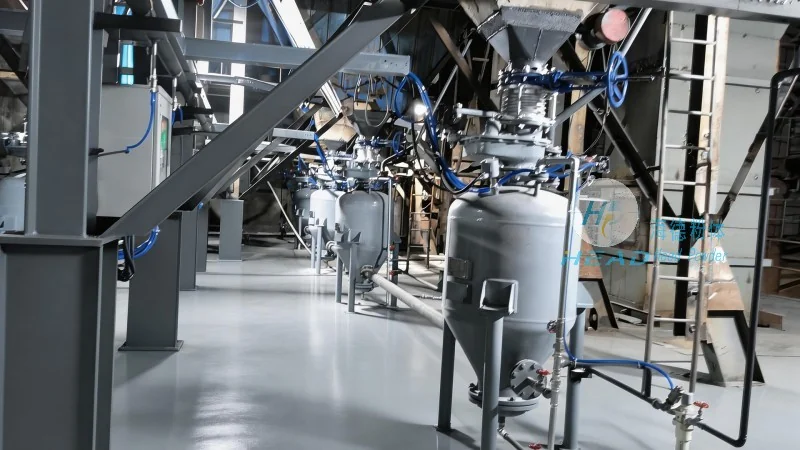
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, has established itself as a trusted provider of specialized material handling solutions. With a strong focus on research and development, the company invests in cutting-edge technologies to enhance the performance and reliability of its equipment. The company’s team of engineers and technicians brings extensive experience in industrial material handling, ensuring that each system is customized to meet the specific needs of clients. HeadPowder’s commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, which guarantee the durability and efficiency of its products. The company’s operational base in Shandong, China, provides a strategic advantage in terms of access to raw materials, manufacturing capabilities, and logistics, enabling it to deliver high-quality products to clients worldwide. By combining technical expertise with a customer-centric approach, HeadPowder continues to lead the industry in providing innovative and effective solutions for ash material handling challenges.




