Principle and Working Scene Characteristics of Water-Containing Powder Material Handling System Equi
Release time:2026-09-19 14:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
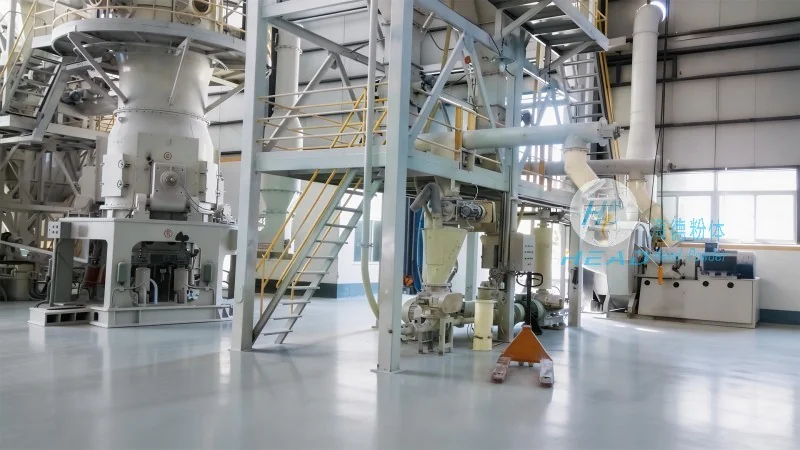
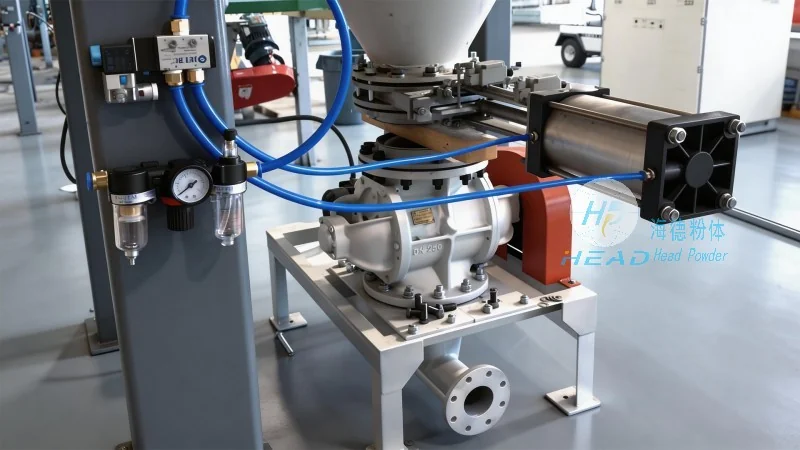
The water-containing powder material handling system, also known as a water-based powder conveying system, is a specialized equipment designed for the efficient and safe transportation of powder materials that are prone to dust or require moisture control. This system integrates water and powder in a controlled manner to ensure stable and reliable material flow, making it widely used in various industrial applications where traditional dry powder conveying methods may face challenges such as dust explosion risks or material agglomeration.
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the professional manufacturer of this advanced material handling system, is a leading company based in Shandong, China. With years of experience in engineering and manufacturing, Headpowder specializes in providing customized solutions for powder processing industries. The company's commitment to quality and innovation has enabled it to deliver high-performance equipment that meets the stringent requirements of modern industrial operations.
Principle of the Water-Containing Powder Conveying System
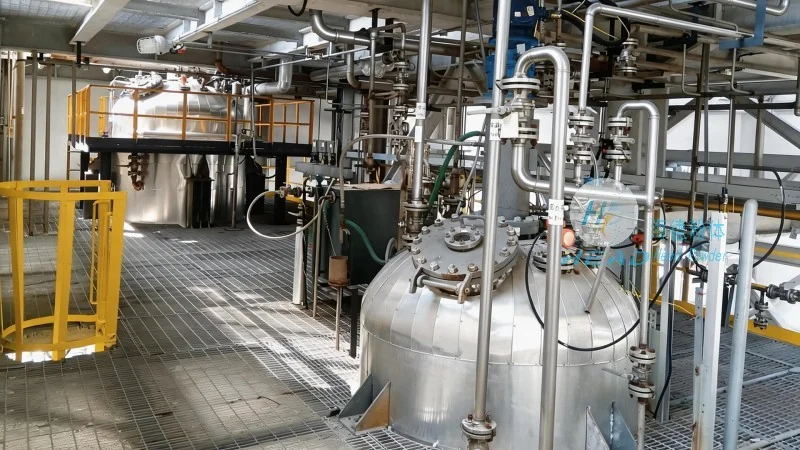
The core principle of the water-containing powder material handling system lies in the formation of a slurry or wet mixture by combining powder with a controlled amount of water. This slurry is then transported through a pipeline using pumps or other conveying mechanisms. The water acts as a carrier, reducing the dust generation and ensuring smooth flow. The system typically includes components such as a powder feeder, water injection device, pipeline, and a separation unit at the end. The powder is mixed with water in the feeder, creating a homogeneous slurry that is then pumped through the pipeline to the destination point. At the receiving end, the water is separated from the powder, allowing the powder to be collected while the water is recycled or disposed of appropriately.
Key Working Scene Characteristics
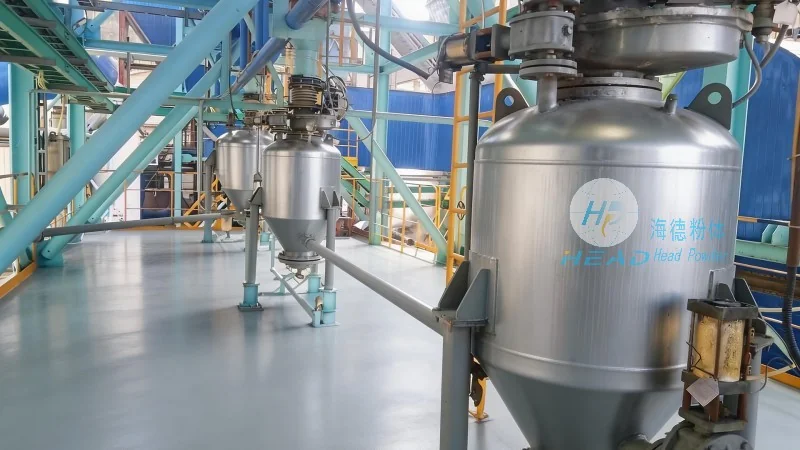
The water-containing powder material handling system is particularly suitable for working scenes where traditional dry conveying methods are not feasible. These include industries dealing with explosive powders, where dust control is critical to prevent accidents. It is also ideal for applications involving fine powders that tend to agglomerate or clog pipelines, as the water helps maintain a consistent flow. Additionally, the system is beneficial in environments where environmental regulations require strict dust suppression measures. The working scene characteristics also include the ability to handle a wide range of powder types, from inorganic powders like cement and limestone to organic powders such as food additives or pharmaceutical powders. The system's flexibility allows it to adapt to different production scales and operational conditions, making it a versatile solution for various industrial needs.




