Seasoning powder conveying machines are essential equipment in the food processing industry, designed to efficiently transport various powdered seasonings with precision and reliability. This article explores the fundamental principles behind these machines and highlights key application scenarios where they excel in operational efficiency and product quality maintenance.
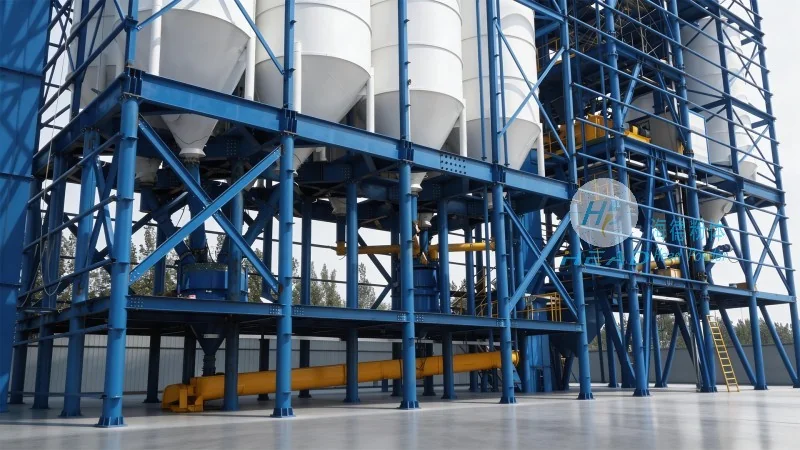
Introduction to Seasoning Powder Conveying Machines
HeadPowder, a leading manufacturer based in Shandong, China, specializes in developing advanced powder handling solutions tailored for the demanding needs of the food sector. The company's expertise lies in creating equipment that ensures seamless, hygienic, and efficient movement of seasonings like spices, herbs, and flavor enhancers. These machines are engineered to handle delicate powders without degradation, preserving the integrity of the ingredients while maintaining strict sanitary standards.
Core Working Principles of Seasoning Powder Conveying Systems
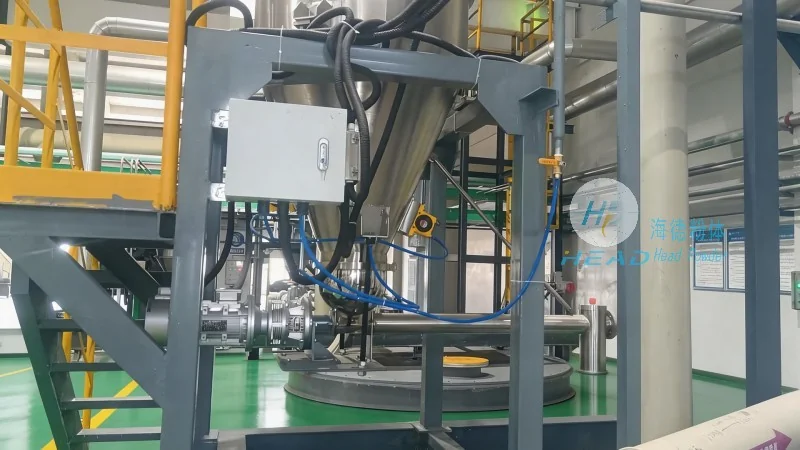
The operation of seasoning powder conveying machines typically revolves around a combination of mechanical and pneumatic components. The primary mechanism involves the use of air pressure or vacuum to draw or push powder particles through a sealed system. For example, some models employ a positive displacement blower to generate consistent airflow, ensuring uniform conveying of fine powders. The system often includes a hopper to store the seasoning, a control valve to regulate the flow rate, and a discharge outlet connected to the processing line. This setup minimizes product exposure to air and contaminants, which is critical for maintaining the flavor and freshness of the seasonings.
Key Features Enhancing Performance and Hygiene
Modern seasoning powder conveying machines from HeadPowder are equipped with several features that enhance their functionality and compliance with industry standards. One notable feature is the use of stainless steel construction, which is non-corrosive and easy to clean, reducing the risk of cross-contamination. The design also incorporates CIP (Clean-In-Place) capabilities, allowing for thorough sanitation without disassembling the equipment. Additionally, the machines often include adjustable speed controls and flow meters to monitor and adjust the conveying rate in real-time, ensuring optimal performance under varying production loads.
Application Scenarios in Food Processing
Seasoning powder conveying machines find extensive applications across various stages of food production. In the initial ingredient handling phase, these machines efficiently transfer raw spices from storage to mixing units, ensuring consistent ingredient distribution. During the production of ready-to-eat meals or sauces, they maintain a steady supply of flavor enhancers to the mixing line, preventing bottlenecks and maintaining product uniformity. Furthermore, in the packaging stage, the machines can precisely dispense seasonings into containers, reducing waste and improving packaging accuracy. The versatility of these systems makes them suitable for both large-scale industrial operations and smaller-scale food processing facilities.
Benefits of Choosing Seasoning Powder Conveying Machines from HeadPowder
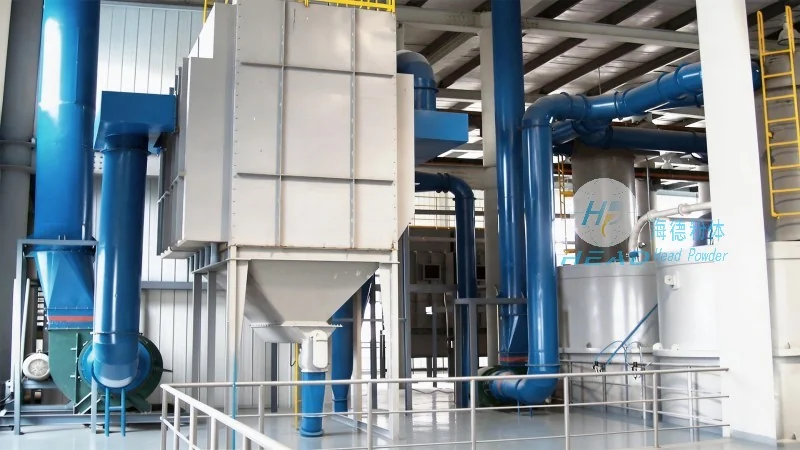
Companies operating in the food industry benefit significantly from adopting seasoning powder conveying machines from HeadPowder. The primary advantage is the improved operational efficiency, as these machines reduce labor costs by automating the powder handling process. They also enhance product quality by minimizing powder degradation and contamination, which is crucial for maintaining consumer trust and regulatory compliance. Another key benefit is the enhanced safety features, such as enclosed systems that prevent dust explosions and reduce exposure to airborne particles for operators. The durability and low maintenance requirements of these machines also contribute to long-term cost savings for businesses.
Conclusion and Industry Impact
Seasoning powder conveying machines are indispensable tools for modern food processing operations, offering a reliable solution for the efficient and hygienic handling of powdered seasonings. HeadPowder's commitment to innovation and quality ensures that their equipment meets the evolving demands of the industry, providing businesses with a competitive edge in product consistency and operational efficiency. As the food industry continues to prioritize safety, quality, and efficiency, these machines will remain a vital component in maintaining high standards of production.




