The intelligent tonne bag feeding station material conveying line is a specialized system designed for efficient handling and transportation of bulk materials from large tonne bags. This system integrates advanced automation technologies and robust mechanical components to ensure reliable and high-performance material transfer in industrial settings. The core principle revolves around the seamless integration of feeding, conveying, and processing stages, optimizing material flow from the point of receipt to the subsequent production or storage stages.
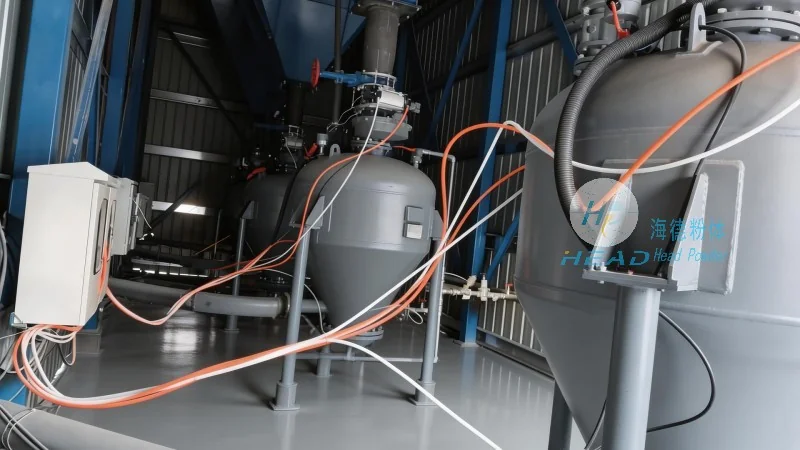
Key Components and Working Principle
At the heart of the system lies a series of interconnected components that work in harmony to achieve efficient material handling. The process typically begins with the unloading of tonne bags, where a mechanical unloader or lifting mechanism extracts the material from the bag. This is followed by a series of conveyors, such as belt conveyors or screw conveyors, which transport the material to the processing or storage areas. The system may also incorporate sensors and control systems to monitor the material flow, ensuring consistent and safe operation. The working principle emphasizes automation, reducing manual intervention and enhancing operational efficiency.
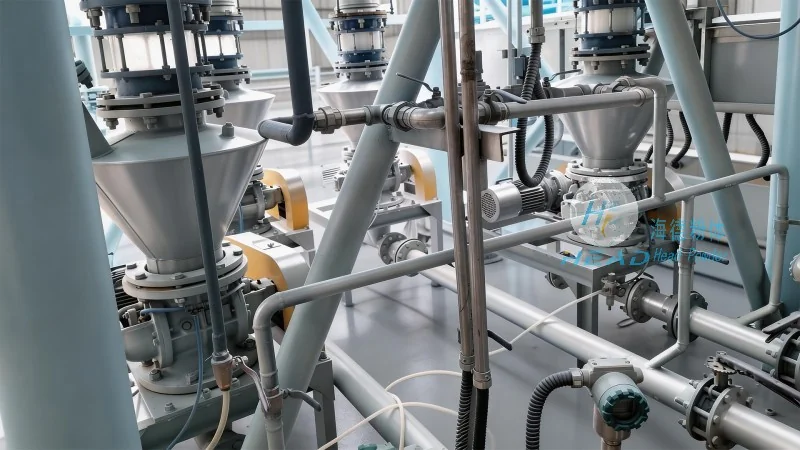
Working Scene Characteristics and Applications
The intelligent tonne bag feeding station material conveying line is particularly suited for industrial environments where large volumes of bulk materials are processed, such as in chemical, food, and mining industries. The system's design allows for flexibility in handling various material types, including powders, granules, and bulk solids. The working scene characteristics include high throughput capacity, minimal downtime, and the ability to integrate with existing production lines. This makes it an ideal solution for facilities that require reliable and continuous material supply, ensuring smooth production operations without interruptions.
Advantages and Benefits in Industrial Operations
Implementing the intelligent tonne bag feeding station material conveying line offers several advantages that enhance overall operational performance. Firstly, it significantly reduces labor costs by automating the material handling process, minimizing the need for manual labor in tasks like bag unloading and material transport. Secondly, the system ensures consistent material quality and flow, reducing the risk of material contamination or loss. Additionally, the advanced control systems provide real-time monitoring and data collection, enabling better process management and decision-making. The robust construction and durability of the components also contribute to long-term reliability, minimizing maintenance and replacement costs over the system's lifespan.
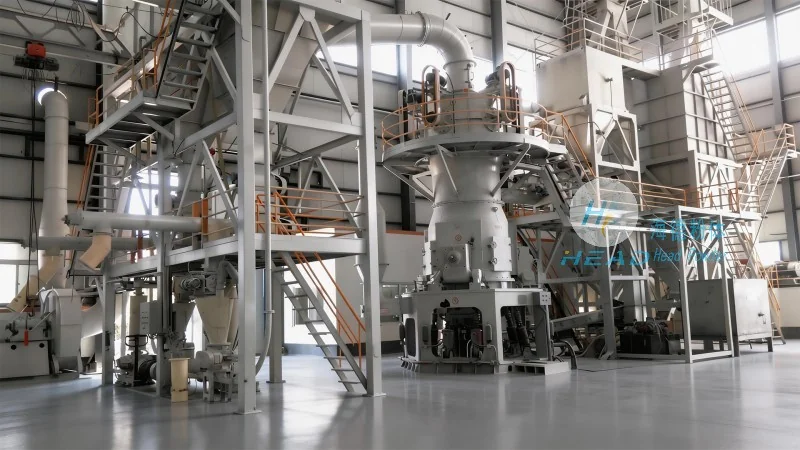
Company Information and Contact Details
HeadPowder, a leading provider of engineering solutions, specializes in designing and manufacturing advanced material handling systems. With headquarters in Shandong, China, HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for industries seeking efficient and reliable material processing solutions. The company's commitment to innovation and quality ensures that its products meet the highest standards of performance and durability, catering to the diverse needs of modern industrial operations.




