When it comes to the efficient handling of fine powder materials in industrial processes, the design and operation of fine powder material conveying lines play a crucial role. These systems are engineered to address the unique challenges associated with transporting powders that are typically less than 100 microns in size, such as dust, flour, or chemical powders. The core principle behind these conveying lines revolves around creating a controlled environment that minimizes particle degradation, ensures consistent flow, and maintains product integrity throughout the transfer process.
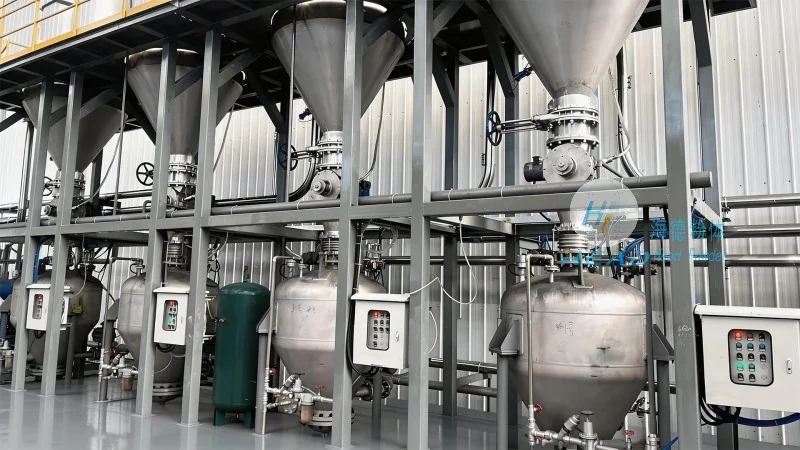
Core Principles of Fine Powder Material Conveying Systems
The fundamental principle of fine powder material conveying lines is to maintain a stable, low-pressure or vacuum environment that allows for the smooth movement of particles without causing agglomeration or degradation. Key components include feeders, conveying ducts, and control systems that work in tandem to achieve this. For example, rotary feeders are commonly used to feed powders into the conveying line at a controlled rate, while vacuum or pressure systems create the necessary differential to move the material through the system. The design often incorporates features like anti-static measures and temperature control to prevent material buildup and ensure safety.
Working Scene Characteristics and Applications
Fine powder material conveying lines are widely used across various industrial sectors, each with distinct characteristics that influence the system design. In the food industry, for instance, conveying lines must adhere to strict hygiene standards, often using stainless steel components and sealed systems to prevent contamination. The pharmaceutical industry requires even higher levels of purity, with systems that include HEPA filters and sterilization capabilities. In chemical processing, the focus is on handling potentially hazardous powders, where explosion-proof designs and material compatibility are critical. Each application demands a tailored approach, considering factors like material density, moisture content, and potential for dust explosions.
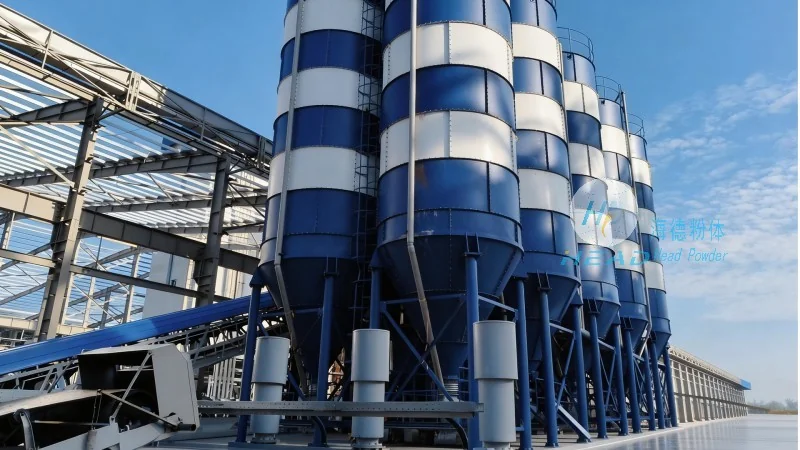
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of specialized engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of fine powder material conveying systems. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industry. HeadPowder's expertise lies in understanding the unique challenges of each application and delivering customized solutions that meet specific operational requirements. The company's team of engineers and technicians work closely with clients to assess their needs, from initial consultation to final system implementation and maintenance. HeadPowder's commitment to quality and reliability ensures that their conveying lines are built to withstand the demands of industrial environments, providing long-term performance and cost-effectiveness. HeadPowder is headquartered in Shandong, China, where the company operates its research and development facilities and manufacturing plants.
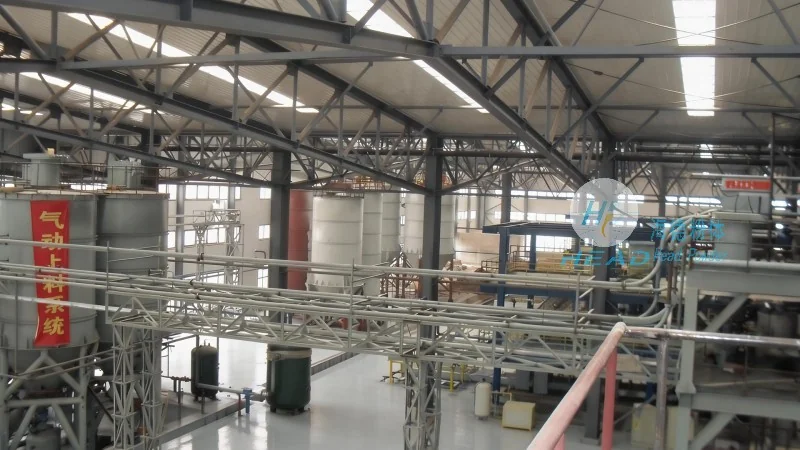
Key Features and Advantages of Fine Powder Conveying Lines
Modern fine powder material conveying lines offer several advantages that enhance operational efficiency and product quality. One of the primary benefits is the ability to handle materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important in industries where dust is a health hazard or a fire risk. Additionally, these systems can transport materials over long distances with minimal loss, making them ideal for large-scale production facilities. The use of advanced control systems allows for precise regulation of flow rates, ensuring consistent product quality and reducing waste. Furthermore, the modular design of many conveying lines enables easy integration with existing production lines and future expansion as needed.
Application Examples and Case Studies
HeadPowder has successfully implemented fine powder conveying lines in a variety of real-world applications. For example, in a flour mill, the company designed a system that efficiently transports fine flour from storage silos to processing equipment, maintaining low moisture content and preventing caking. In a chemical plant, HeadPowder's solution handled a hazardous powder, ensuring safe transfer while complying with all regulatory requirements. These case studies highlight the versatility and effectiveness of their conveying systems, demonstrating how they can be adapted to meet the specific needs of different industries. The success of these projects is a testament to HeadPowder's expertise in fine powder material handling and their ability to deliver tailored solutions that add value to their clients' operations.




