When it comes to the efficient handling of bulk materials in industrial settings, specialized equipment plays a crucial role. Among these, cement ash and mine powder material conveying equipment stands out as a vital component in many production processes. This equipment is specifically designed to transport materials such as cement ash, mine powders, and other fine particulate substances with precision and reliability. Understanding its functionality and design principles is essential for optimizing material flow in various industrial applications.
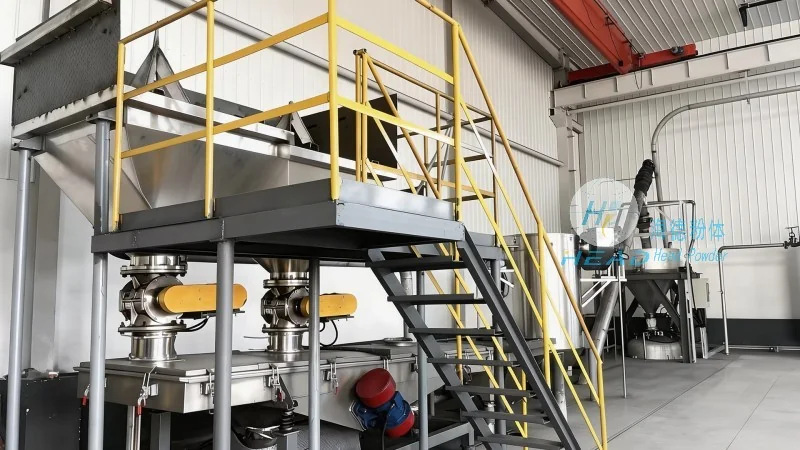
Overview of Cement Ash and Mine Powder Material Conveying Equipment
Cement ash and mine powder material conveying equipment is a type of machinery used to transport bulk materials from one location to another within industrial facilities. These systems are engineered to handle materials with specific characteristics, including fine particle sizes, high moisture content, or abrasive properties. The primary goal of such equipment is to ensure smooth, continuous, and safe material transfer, minimizing downtime and operational costs. The equipment typically consists of components like hoppers, feeders, conveyor belts, or pneumatic systems, depending on the material's properties and the required conveying distance.
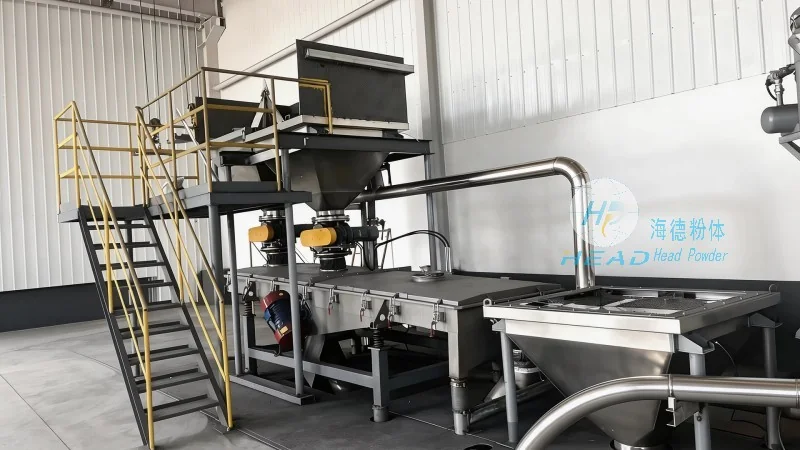
Key Design Principles for Efficient Material Conveying
The design of cement ash and mine powder conveying equipment is guided by several key principles to ensure optimal performance. First, the equipment must be able to handle the specific physical and chemical properties of the materials being transported. This includes considerations such as particle size distribution, moisture content, and abrasiveness, as these factors can impact the equipment's wear rate and overall efficiency. Second, the design emphasizes durability and reliability. Given the often harsh operating conditions in industrial environments, the equipment is constructed from high-quality materials that can withstand continuous use and resist corrosion or wear. Third, the design prioritizes energy efficiency and operational cost-effectiveness. Advanced engineering techniques are employed to minimize energy consumption while maximizing material throughput, which is critical for maintaining profitability in industrial operations. Additionally, the design incorporates safety features to protect operators and prevent material spills or blockages, ensuring a secure working environment.
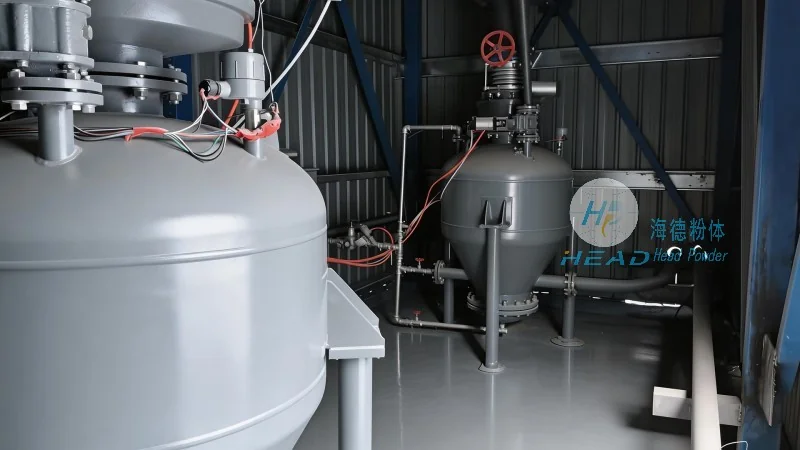
Components and Functionalities of the Equipment
The cement ash and mine powder material conveying equipment typically includes several key components that work together to achieve efficient material transport. The first component is the hopper or feeder, which is responsible for receiving and storing the material before it is conveyed. This component is designed to handle the material's bulk density and flow characteristics, ensuring a consistent feed rate to the conveyor system. The feeder may include features like vibration or screw mechanisms to control the material flow and prevent blockages. The second component is the conveyor itself, which can be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the application. Belt conveyors are commonly used for horizontal or slightly inclined transport, while screw conveyors are suitable for vertical or inclined transport of fine powders. Pneumatic conveyors, on the other hand, use air pressure to transport materials, which is ideal for handling dust or fine powders that are sensitive to mechanical contact. The conveyor system is equipped with appropriate drive mechanisms, such as electric motors or gearboxes, to provide the necessary power for material movement. Additionally, the equipment may include control systems that monitor the conveyor's operation, such as sensors for detecting blockages or overloads, and control panels for adjusting the feed rate or speed.
Applications and Benefits in Industrial Settings
Cement ash and mine powder material conveying equipment is widely used in various industrial sectors, including cement production, mining, and chemical processing. In cement plants, for example, this equipment is used to transport cement ash from storage silos to mixing or packaging areas, ensuring a steady supply of raw materials for production. In mining operations, it is used to convey mine powders from processing facilities to storage or transport vehicles, facilitating the efficient extraction and distribution of minerals. The benefits of using such equipment in these applications are significant. By automating the material handling process, industries can reduce labor costs and improve operational efficiency. The equipment's ability to handle large volumes of material at a consistent rate minimizes bottlenecks and ensures smooth production flow. Additionally, the equipment's design minimizes material loss and contamination, which is crucial for maintaining product quality and meeting regulatory standards. The use of advanced materials and engineering in the equipment's construction also extends its lifespan, reducing maintenance and replacement costs over time.
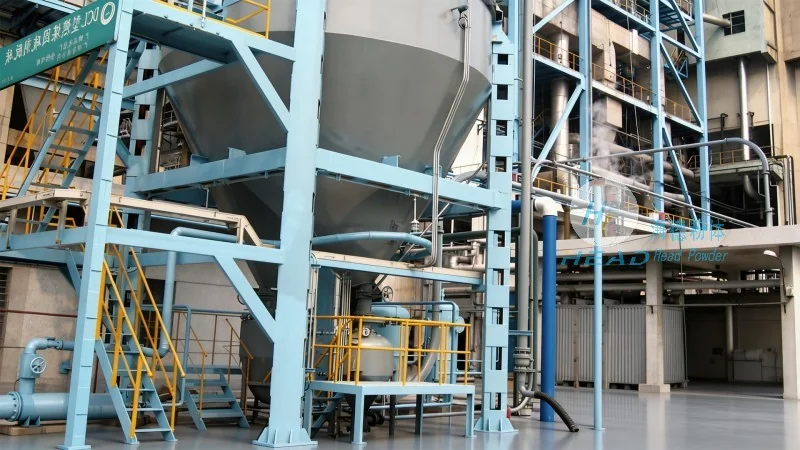
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of specialized material handling equipment, including cement ash and mine powder conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient material transport solutions. HeadPowder's team of engineers and technicians is dedicated to developing customized equipment that meets the specific needs of each client, ensuring optimal performance and durability. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced production equipment and quality control systems. HeadPowder's commitment to customer satisfaction and technical excellence has earned it a reputation as a leading provider of material handling solutions in the industry.




