HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The company's expertise lies in creating efficient and reliable systems for transporting bulk materials, with a particular focus on the food processing industry. This article introduces the design of a negative pressure pneumatic conveying system specifically tailored for wheat flour, highlighting the technical aspects, operational benefits, and practical applications of such a system.
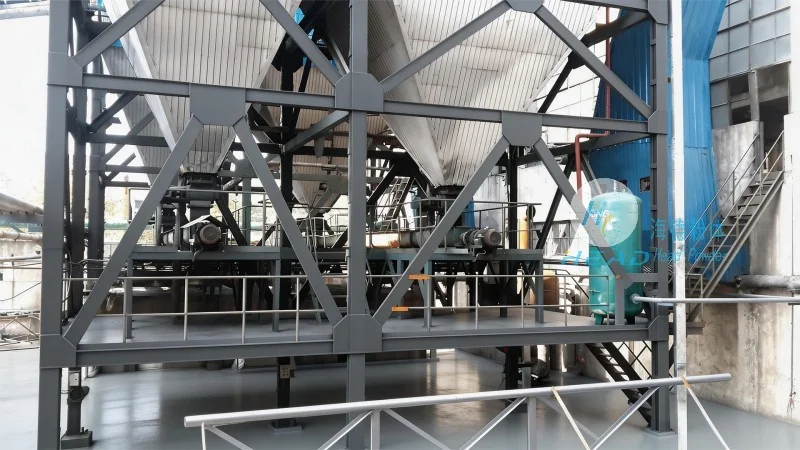
Overview of the Negative Pressure Pneumatic Conveying System
A negative pressure pneumatic conveying system is a method of transporting dry bulk materials, such as wheat flour, using air as the conveying medium. Unlike positive pressure systems that force air and material through a pipeline, negative pressure systems draw material into the system using a vacuum or suction. This approach offers several advantages, including reduced product contamination, lower energy consumption, and improved safety for operators. The system typically consists of a hopper, a vacuum pump, a filter, and a series of pipelines that guide the material from the source to the destination.
Key Components and Their Functions
The design of the wheat flour negative pressure conveying system incorporates several critical components, each playing a vital role in the overall operation. The hopper serves as the initial storage and feeding unit, where wheat flour is collected and prepared for transport. The hopper is equipped with a feeder, which controls the flow rate of the material into the system, ensuring a consistent and controlled discharge. The vacuum pump is the heart of the system, generating the necessary suction to draw the flour and air mixture through the pipelines. This pump is typically a rotary vane or roots-type pump, chosen for its efficiency and ability to handle fine powders without clogging. The filter is an essential component that separates the flour from the air, preventing dust and particles from being released into the environment. The filtered air is then discharged safely, while the collected flour is directed to the receiving container.
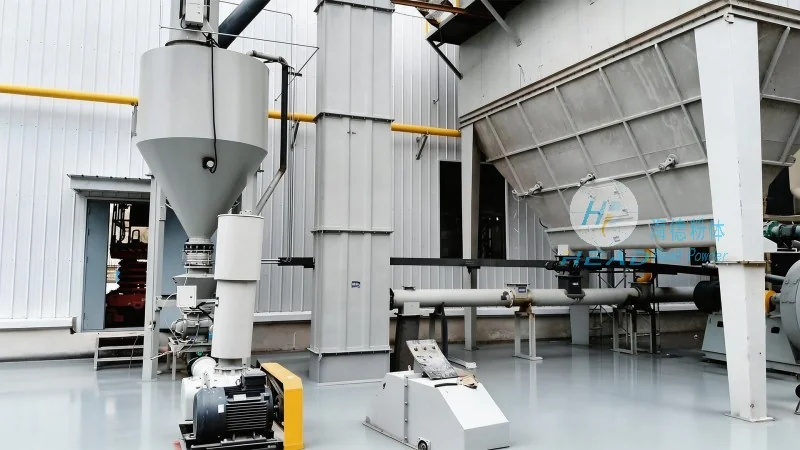
Technical Specifications and Performance Parameters
The negative pressure pneumatic conveying system for wheat flour is engineered to meet specific performance requirements, ensuring optimal efficiency and reliability. The system is designed to handle capacities ranging from low to medium volumes, making it suitable for various production scales. The conveying distance can vary depending on the layout of the facility, with typical ranges from 50 to 200 meters. The system operates at a vacuum level of approximately 50 to 70 kPa, which is sufficient to maintain a stable flow of wheat flour through the pipelines. The air velocity within the system is maintained at a level that prevents material settling or clogging, typically around 20 to 30 m/s. The energy consumption of the system is relatively low compared to other conveying methods, as the vacuum pump operates at a moderate pressure, reducing overall operational costs.
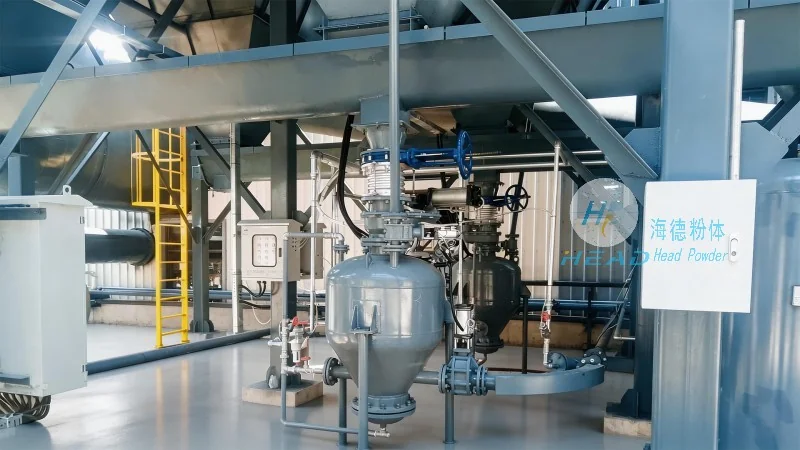
Operational Benefits and Advantages
Implementing a negative pressure pneumatic conveying system for wheat flour offers numerous benefits for food processing facilities. One of the primary advantages is the reduction of product contamination, as the system is enclosed and sealed, preventing exposure to external elements or contaminants. This is particularly important for wheat flour, which is a critical ingredient in many food products and requires strict hygiene standards. Additionally, the system minimizes dust generation, improving workplace safety and reducing the risk of respiratory issues for operators. The enclosed design also helps in maintaining a clean and organized production environment, which is essential for compliance with food safety regulations. Furthermore, the system's ability to handle fine powders without clogging ensures consistent and reliable operation, reducing downtime and maintenance costs.
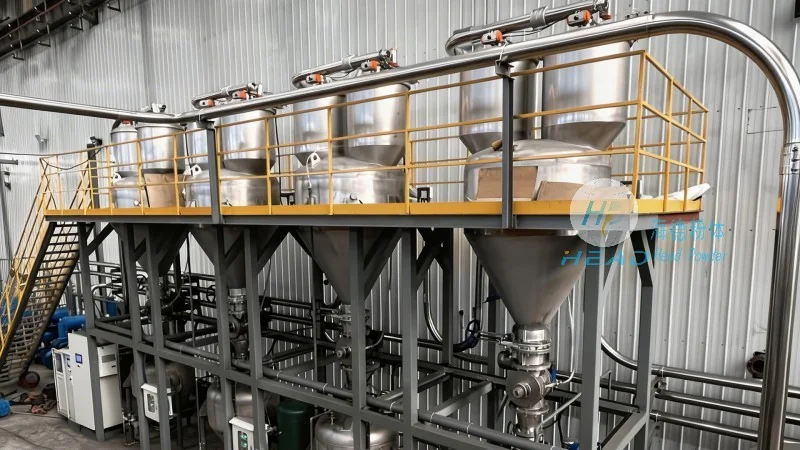
Application Scenarios and Industry Use Cases
The negative pressure pneumatic conveying system designed by HeadPowder is widely applicable in the food processing industry, particularly in wheat flour milling and bakery operations. It is commonly used to transport wheat flour from storage silos to mixing rooms, or from production lines to packaging areas. The system can also be integrated into larger material handling networks, connecting multiple production units and ensuring a seamless flow of materials throughout the facility. In addition to wheat flour, the system can be adapted for other fine powders, such as sugar, starch, or other food ingredients, making it a versatile solution for various bulk material transport needs.
Engineering and Customization Capabilities of HeadPowder
HeadPowder, with its headquarters in Shandong, China, offers comprehensive engineering and customization services to meet the specific needs of each client. The company's team of experienced engineers works closely with clients to understand their operational requirements, production volumes, and space constraints. Based on this information, they design a tailored negative pressure pneumatic conveying system that maximizes efficiency and minimizes costs. The engineering process includes detailed calculations of material flow rates, pipeline dimensions, and vacuum levels, ensuring that the system operates within optimal parameters. HeadPowder also provides installation and commissioning services, ensuring that the system is set up correctly and functions as intended. The company's commitment to quality and customer satisfaction has made it a trusted partner for many food processing companies in China and beyond.




