The Ammonium Bicarbonate Pneumatic Conveying System is a specialized industrial equipment designed for the efficient handling and transportation of ammonium bicarbonate, a critical chemical widely used in various industries such as food processing, pharmaceuticals, and chemical manufacturing. This system leverages pneumatic technology to move the material from one location to another without the need for mechanical components like belts or buckets, offering advantages in terms of hygiene, speed, and reduced contamination risks. As a key component in material handling, this equipment plays a vital role in ensuring smooth production workflows and maintaining product quality.
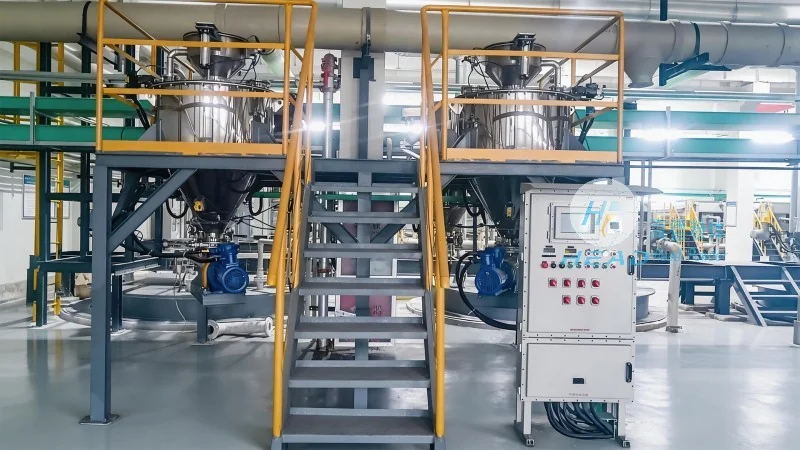
Overview of the Equipment and Its Core Components
The system typically consists of several essential parts, including a hopper for material storage, a blower or air compressor to generate the necessary air pressure, a pipeline network for conveying the material, and a receiver or discharge unit for the final delivery. The hopper is designed to hold the ammonium bicarbonate, ensuring a consistent feed to the system. The blower provides the motive force, creating a flow of air that carries the material particles through the pipeline. The pipeline, often made of durable materials like stainless steel or plastic, is engineered to withstand the chemical properties of ammonium bicarbonate and maintain structural integrity under operational pressures. The receiver unit collects the material at the destination, allowing for controlled discharge into storage or processing equipment. Each component works in tandem to create a seamless conveying process.
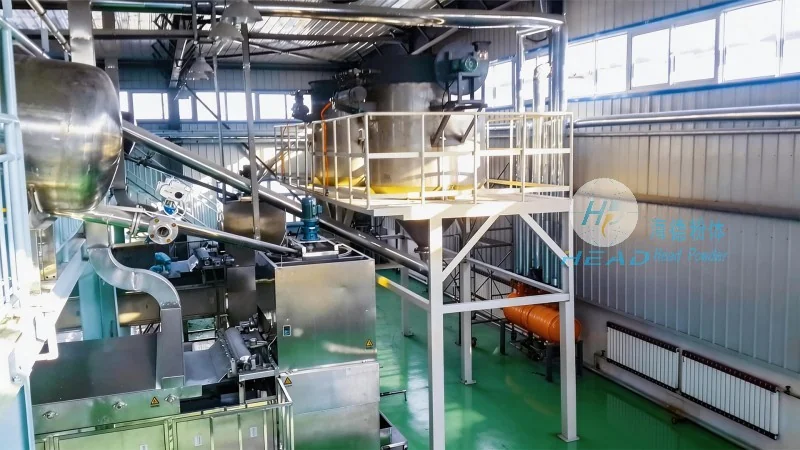
Design Principles Underlying the System
The design of the Ammonium Bicarbonate Pneumatic Conveying System is guided by several fundamental principles aimed at optimizing performance and safety. One primary principle is the use of positive pressure or negative pressure systems, where positive pressure involves blowing air into the pipeline to push the material, and negative pressure involves creating a vacuum to pull the material. For ammonium bicarbonate, positive pressure is commonly preferred due to the material's tendency to clog or agglomerate, as it helps maintain a consistent flow and prevents blockages. Another key principle is the consideration of material properties, such as particle size, density, and moisture content, which influence the air velocity required for effective conveying. The system is designed to operate at an air velocity that is sufficient to keep the material suspended but not so high as to cause excessive wear on the components or energy waste. Additionally, the design incorporates features like air filtration and moisture control to prevent contamination and ensure the material remains in optimal condition during transport.
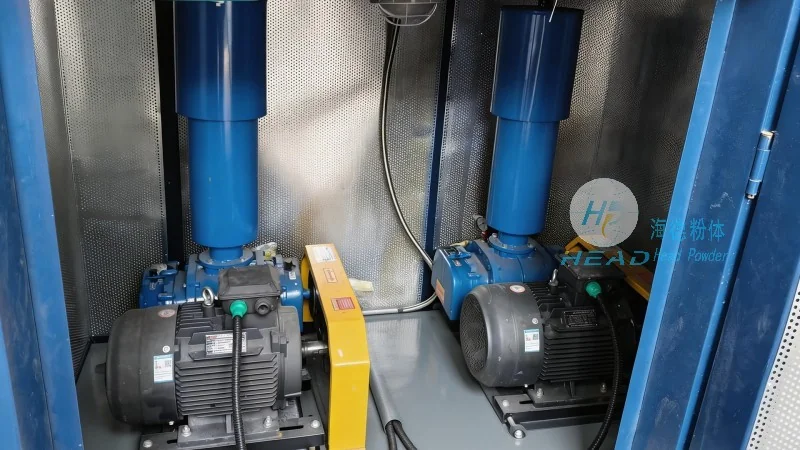
Key Features and Technical Specifications
The Ammonium Bicarbonate Pneumatic Conveying System from Shandong HeadPowder Engineering Co., Ltd. offers several key features that enhance its functionality and reliability. The system is equipped with advanced control systems that allow for precise regulation of air pressure and flow rates, ensuring consistent material delivery. It also includes safety features such as pressure relief valves and overcurrent protection to prevent equipment damage and ensure operator safety. The equipment is constructed using high-quality materials, such as stainless steel, which are resistant to corrosion and chemical reactions with ammonium bicarbonate, extending the system's lifespan and reducing maintenance costs. Technical specifications include a conveying capacity ranging from 1 to 50 tons per hour, depending on the specific configuration, and air pressure capabilities from 0.5 to 1.5 bar. The pipeline diameter can be customized to suit different material volumes and flow rates, with options for both straight and curved sections to accommodate complex layouts. These features make the system versatile and adaptable to various industrial applications.
Application Scenarios and Operational Benefits
The Ammonium Bicarbonate Pneumatic Conveying System is widely used in industries where the handling of ammonium bicarbonate is critical. In food processing, it is used to transport the chemical to production lines for use in baking and other food products, ensuring a hygienic and efficient process. In pharmaceutical manufacturing, the system helps move the material to mixing and packaging equipment, maintaining the purity and quality of the final products. In chemical manufacturing, it is employed in the production of fertilizers and other chemical compounds, where consistent material flow is essential for batch processing. The operational benefits of this system include increased efficiency in material handling, reduced labor costs due to automated transport, and improved product quality through minimized contamination and handling errors. Additionally, the system's ability to handle the material in a closed environment helps prevent dust emissions and environmental contamination, aligning with modern industrial standards for safety and sustainability.
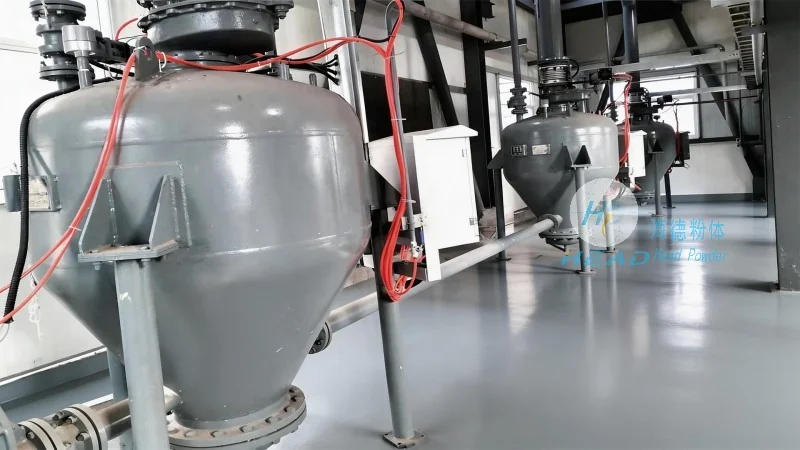
Company Information and Contact Details
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of material handling equipment, specializes in designing and producing high-quality Ammonium Bicarbonate Pneumatic Conveying Systems. The company is headquartered in Shandong, China, and has a strong reputation for delivering reliable and efficient solutions tailored to the needs of various industries. With years of experience in the field, HeadPowder has developed a deep understanding of material properties and operational requirements, enabling them to create systems that meet the highest standards of performance and safety. The company's commitment to quality is reflected in its use of advanced manufacturing processes and rigorous testing protocols, ensuring that each system is built to last and perform optimally. For inquiries or further information about the Ammonium Bicarbonate Pneumatic Conveying System, please contact the company at its headquarters in Shandong, China.




