At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and implementation of advanced material handling solutions tailored to the unique demands of the quartz powder industry. Our focus is on developing efficient, reliable, and cost-effective negative pressure pneumatic conveying systems that ensure the safe and precise transport of quartz powder from various sources to processing or storage locations. This document outlines the key design considerations, technical specifications, and operational benefits of our quartz powder negative pressure pneumatic conveying system, highlighting how it addresses the specific challenges faced by quartz powder manufacturers.
Key Design Features and Technical Specifications
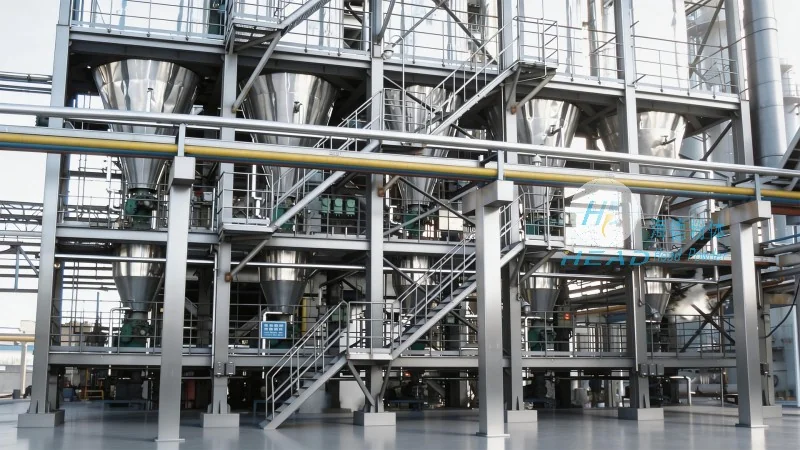
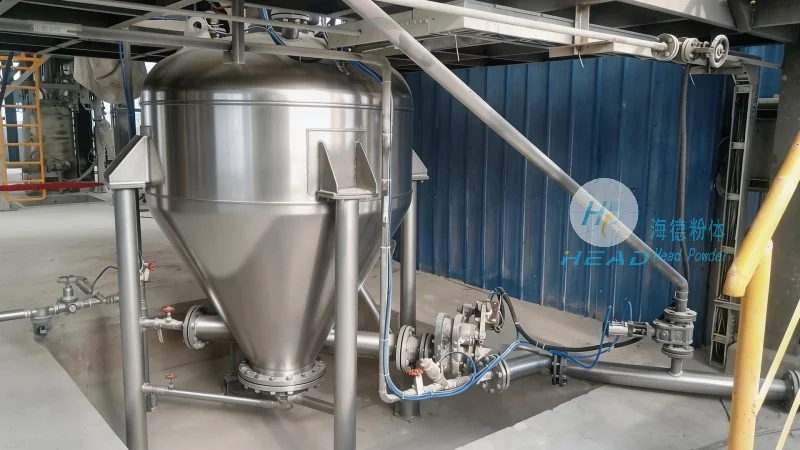
The quartz powder negative pressure pneumatic conveying system is engineered with a comprehensive set of features to optimize performance and durability. The system incorporates high-efficiency vacuum pumps capable of maintaining consistent negative pressure levels, ensuring stable material flow and preventing dust emissions. The pipeline network is constructed from corrosion-resistant materials, such as stainless steel or specialized plastic composites, to withstand the abrasive nature of quartz powder and resist chemical degradation. The design includes multiple inlets and outlets, allowing for flexible integration with existing production lines or new installations. Additionally, the system features advanced filtration and dust collection mechanisms to comply with environmental regulations and maintain air quality in the processing environment. The control system is equipped with user-friendly interfaces and real-time monitoring capabilities, enabling operators to adjust parameters and troubleshoot issues efficiently. The overall design emphasizes energy efficiency, with optimized pump sizing and pipeline layout to minimize operational costs while maximizing conveying capacity.
Operational Benefits and Performance Metrics
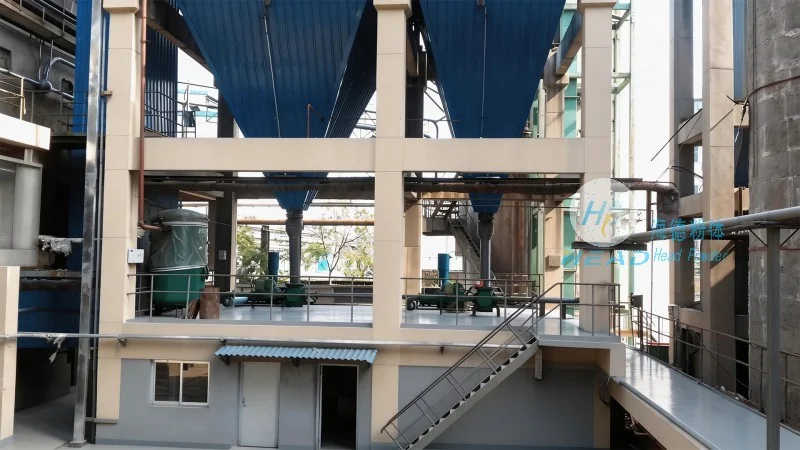
Implementing our quartz powder negative pressure pneumatic conveying system offers numerous advantages for quartz powder producers. The system significantly reduces material handling time and labor costs by automating the transport process, allowing for continuous operation without manual intervention. The negative pressure design minimizes dust dispersion, creating a cleaner working environment and reducing the risk of respiratory issues for personnel. This also helps in maintaining product purity, as the enclosed system prevents contamination from external sources. From a production efficiency standpoint, the system can handle high volumes of quartz powder with consistent flow rates, ensuring that downstream processes receive a steady supply of material. The reliability of the system is enhanced by its robust construction and redundant components, minimizing downtime and maintenance requirements. Performance metrics indicate that the system can achieve conveying distances of up to 100 meters with a capacity of up to 10 tons per hour, depending on the specific application and material characteristics. The energy consumption is optimized through variable frequency drives and efficient pump designs, contributing to lower operational expenses over the system's lifespan.
Customization and Integration Capabilities
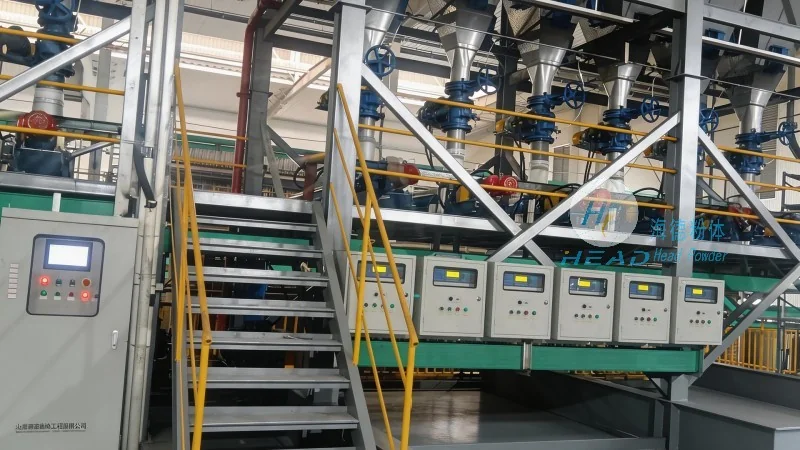
Recognizing that each quartz powder facility has unique operational requirements, our company provides comprehensive customization options for the negative pressure pneumatic conveying system. We work closely with clients to assess their specific needs, including material type, flow rates, and installation constraints, to develop a tailored solution. The system can be integrated with existing equipment, such as hoppers, silos, and processing machinery, through standardized interfaces or custom adapters. For facilities with multiple production lines or varying material handling demands, modular designs are available, allowing for easy expansion or reconfiguration as production scales. The control system can be adapted to existing SCADA or DCS platforms, ensuring seamless integration with the plant's overall automation infrastructure. Additionally, we offer post-installation support services, including training for operators, routine maintenance plans, and technical assistance for troubleshooting, to ensure the system operates at peak performance throughout its service life.
Conclusion and Contact Information
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality, reliable quartz powder negative pressure pneumatic conveying systems that meet the evolving needs of the quartz powder industry. Our expertise in material handling technology, combined with a customer-centric approach, ensures that each system is designed to enhance operational efficiency, reduce costs, and improve workplace safety. For businesses seeking to upgrade their material transport processes, our quartz powder negative pressure pneumatic conveying system represents a superior solution. Contact us today to learn more about how our tailored solutions can benefit your quartz powder production facility.




