Gravity dust removal powder pneumatic conveying equipment is a critical system in industrial material handling, engineered to efficiently transport fine powders while simultaneously capturing and removing airborne dust particles. This equipment is essential for maintaining air quality and ensuring the smooth operation of production lines across various industries, including chemical, pharmaceutical, and food processing.
Working Principle of the Equipment
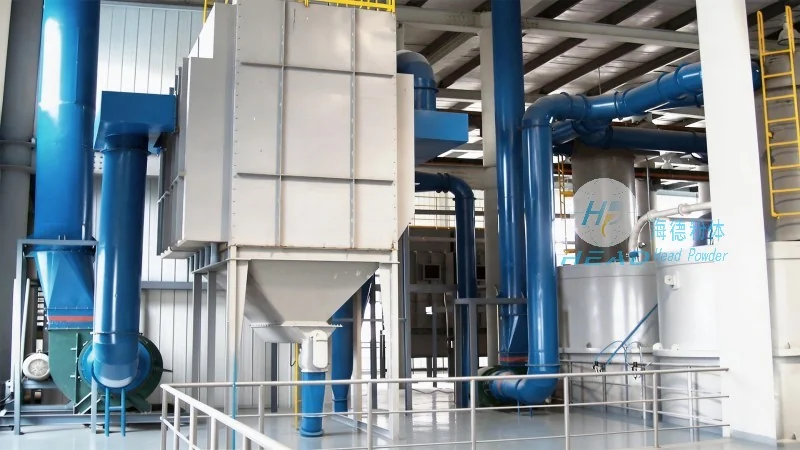
The core of the gravity dust removal powder pneumatic conveying system is its integrated approach to material transport and dust control. The system typically comprises a dust collector, a conveying pipeline, and a material feed mechanism. As powders are introduced into the system, they are drawn into the conveying pipeline by a negative pressure generated by the dust collector. Concurrently, the dust collector captures fine particles suspended in the air, preventing their release into the environment. This combination enables a clean and efficient material handling process.
Operation Process
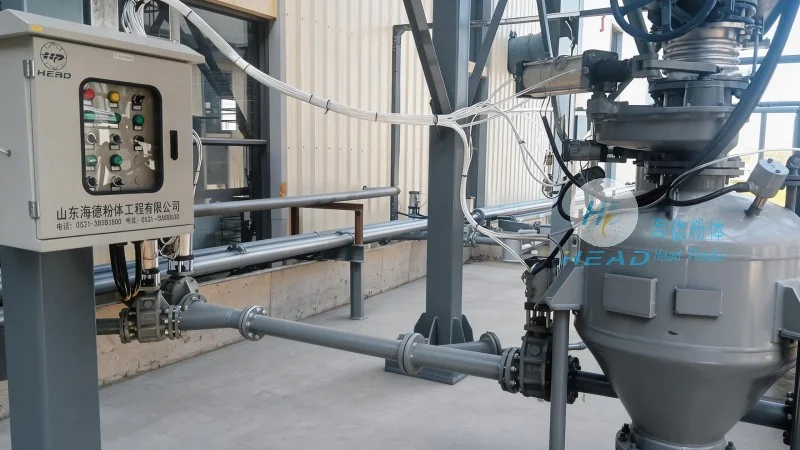
The operation of the gravity dust removal powder pneumatic conveying equipment starts with the preparation of the material to be conveyed. The powder is fed into the system via a hopper or feeder, ensuring a consistent flow rate. The dust collector then activates, creating a vacuum that pulls powder particles into the conveying pipeline. As the powder travels through the pipeline, it is transported to the desired destination, such as a storage silo or processing unit. Throughout this process, the dust collector continuously removes airborne dust, maintaining a clean and safe working environment. The system operates continuously, with the feed rate and vacuum level adjusted as needed to optimize performance and material throughput.
Key Components and Their Functions
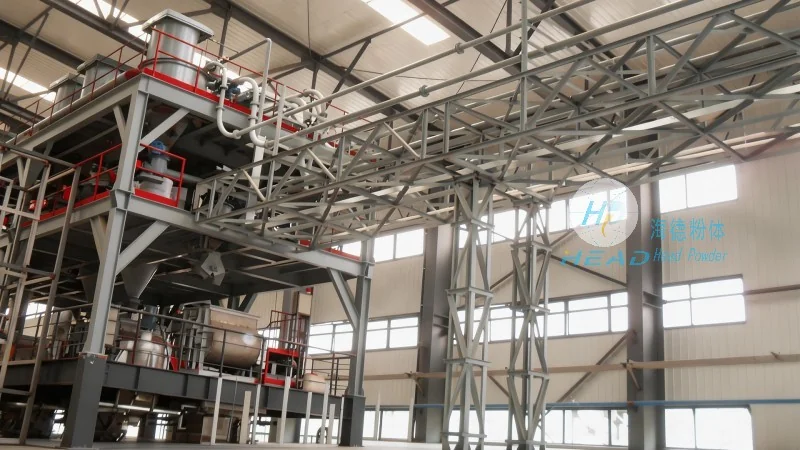
Several key components collaborate to ensure the efficient operation of the gravity dust removal powder pneumatic conveying equipment. The dust collector is the primary component responsible for capturing airborne dust particles, utilizing mechanisms like cyclones or bag filters to separate particles from the air stream. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, ensures that the powder is transported without degradation or contamination. The feed mechanism, which may include a rotary valve or screw feeder, controls the flow rate of the powder into the system, preventing blockages and ensuring a consistent feed. The control system, which monitors pressure, flow rate, and dust levels, adjusts the operation of the equipment to maintain optimal performance.
Benefits and Applications
The gravity dust removal powder pneumatic conveying equipment offers several advantages for industrial applications. It provides a clean and efficient method for transporting fine powders, reducing the risk of dust contamination and improving product quality. The integrated dust removal system helps to comply with environmental regulations and enhances workplace safety by reducing airborne dust levels. This equipment is widely used in industries where fine powders are handled, including chemical manufacturing, pharmaceutical production, food processing, and mineral processing. Its ability to handle a wide range of materials, from dry powders to granules, makes it a versatile solution for various material handling needs.
About Shandong HeadPowder Engineering Co., Ltd.
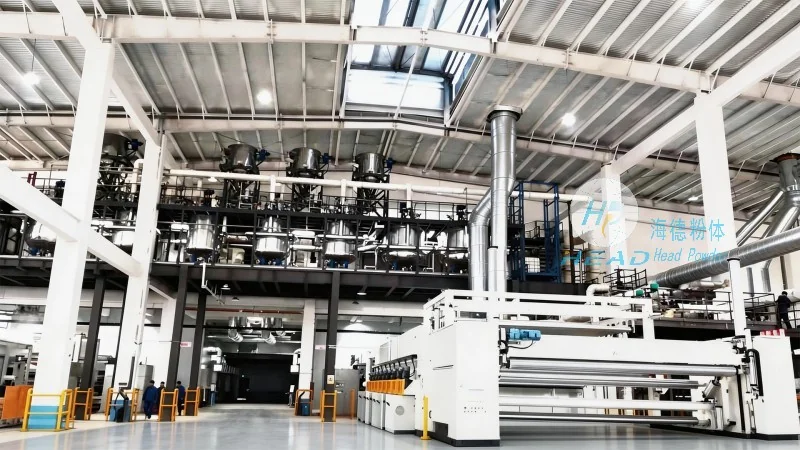
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of industrial material handling equipment. With its headquarters located in Shandong, China, the company specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems, dust removal equipment, and related components. Headpowder has a strong reputation for providing high-quality, reliable equipment that meets the specific needs of its clients. The company's commitment to innovation and customer satisfaction has made it a trusted partner in the industry, delivering solutions that enhance efficiency, safety, and environmental performance in material handling operations.




