Cereal powder conveying equipment is a specialized system designed to handle and transport cereal powders efficiently and safely. These systems are crucial in various industries, including food processing, pharmaceuticals, and chemical manufacturing, where the reliable movement of bulk powders is essential for production continuity and product quality.
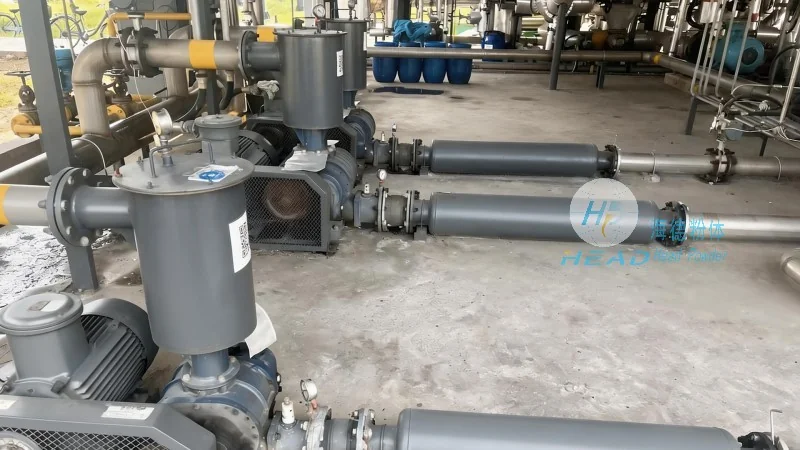
Key Components of the Conveying System
The core components of a typical cereal powder conveying system include a hopper for material storage, a conveyor mechanism (such as a screw conveyor or pneumatic conveyor), a control panel for operation, and a discharge outlet. The hopper is designed to hold the cereal powder, ensuring a consistent feed to the conveyor. The conveyor mechanism transfers the powder from the hopper to the discharge point, while the control panel allows operators to adjust parameters like speed and pressure.
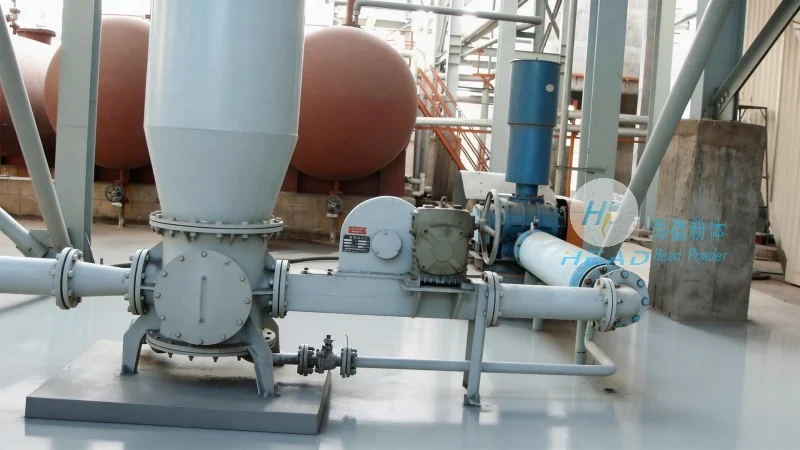
Working Principle of the Equipment
The working principle of cereal powder conveying equipment involves several key steps. First, the cereal powder is fed into the hopper from a storage silo or bulk container. The hopper then regulates the flow of powder into the conveyor. For screw conveyors, a rotating screw pushes the powder forward through a tube, using mechanical force to move the material. Pneumatic conveyors, on the other hand, use compressed air to create a flow of air and powder, transporting the material through a pipeline. The control panel monitors and adjusts the system to maintain optimal flow rates and prevent blockages.
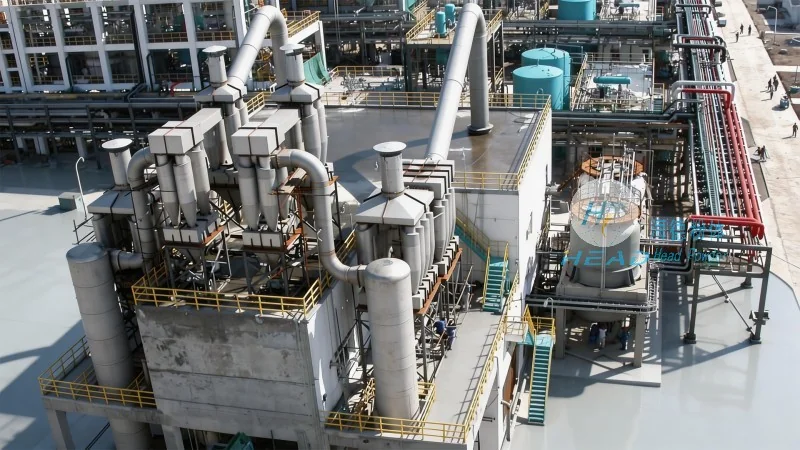
Operation Process Step-by-Step
The operation process of the conveying equipment follows a systematic sequence. Initially, the hopper is filled with the required amount of cereal powder, typically from a bulk storage silo or container. The control panel is then activated, and the conveyor mechanism is started. For screw conveyors, the rotating screw begins to move, pushing the powder forward through the enclosed tube. In pneumatic systems, compressed air is introduced into the pipeline, creating a flow that carries the powder along with it. The powder travels from the hopper to the discharge outlet, where it is collected in a designated container or transferred to the next stage of production. During operation, the control panel continuously monitors key parameters such as pressure, flow rate, and temperature. Sensors within the system detect any deviations, such as a blockage or low material level, and trigger an alert to the operator. This allows for immediate troubleshooting, preventing downtime and ensuring consistent performance. The system may also include safety features like emergency stop buttons and overload protection to enhance operational safety.
Benefits and Applications
Cereal powder conveying equipment offers several benefits, including high efficiency, low maintenance, and the ability to handle a wide range of powder types. These systems are widely used in the food industry for transporting ingredients like flour, oats, and cornmeal. In pharmaceutical applications, they ensure the safe and hygienic transfer of powders, maintaining product purity. The equipment's design also minimizes product degradation, preserving the quality and freshness of the cereal powder.
Company Information
HeadPowder, a leading manufacturer of conveying equipment, specializes in providing customized solutions for bulk material handling. With headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. combines advanced technology and engineering expertise to deliver reliable and efficient conveying systems. The company's products are designed to meet the specific needs of various industries, ensuring optimal performance and durability.




