What is Calcined Ash Material Handling? And What Are Its Design Principles?
Release time:2026-09-14 22:03:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Calcined ash material handling refers to the process of transporting calcined ash, which is a byproduct from the combustion of coal or other fuels in power plants. This material handling system is crucial for the efficient operation of thermal power stations, as it ensures the safe and reliable movement of calcined ash from the ash handling system to disposal or recycling facilities. The design of such systems involves several key principles that address the unique characteristics of calcined ash, including its density, moisture content, and potential for dust generation.
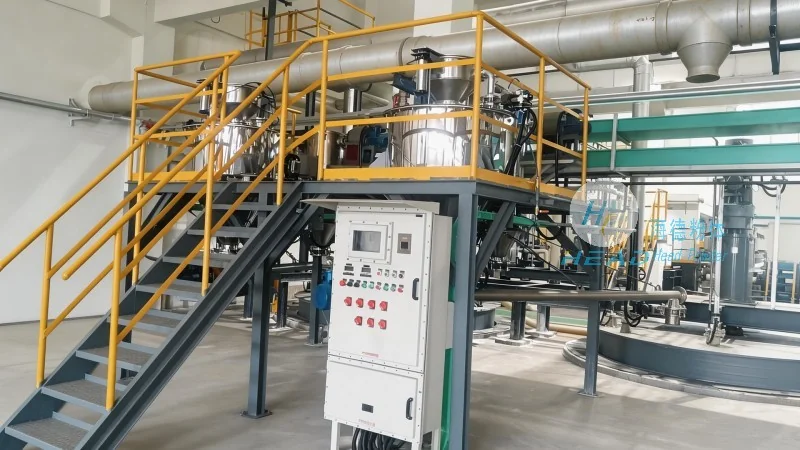
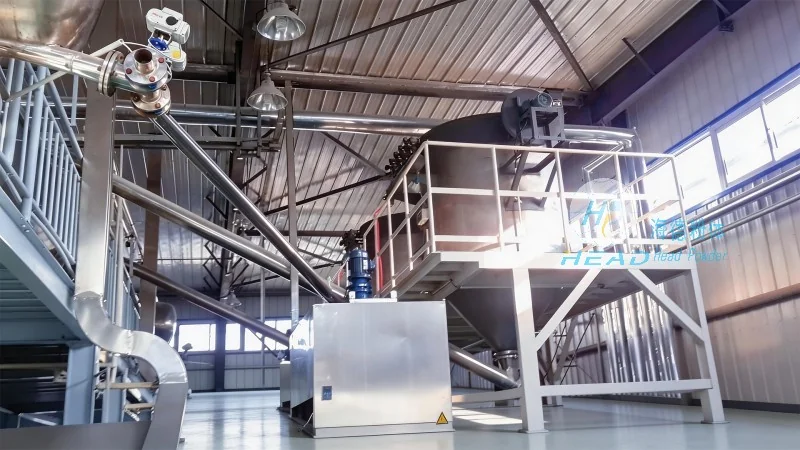
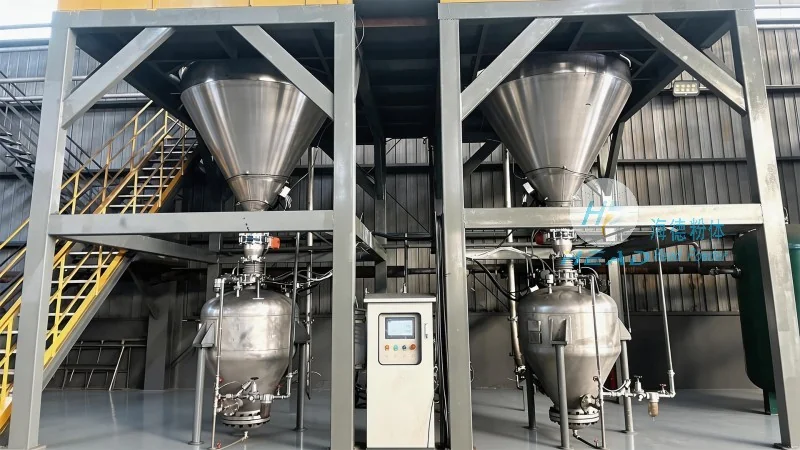
Key Design Principles for Calcined Ash Material Handling
The design of calcined ash material handling systems is based on several fundamental principles that ensure operational efficiency, safety, and environmental compliance. First, the system must be capable of handling the high volume and weight of calcined ash, which typically has a bulk density ranging from 800 to 1200 kg/m³. This requires robust equipment such as belt conveyors, screw conveyors, or pneumatic transport systems that can withstand the mechanical stress and abrasion caused by the ash particles. Second, the system must address the moisture content of the ash, as high moisture levels can lead to clogging and reduced conveyor efficiency. Designers often incorporate drying mechanisms or use materials with low friction coefficients to mitigate these issues. Third, dust control is a critical aspect, as calcined ash can generate significant airborne dust, posing health and environmental risks. Therefore, dust suppression systems, such as water sprays or enclosed conveyor designs, are integral to the overall design. Finally, the system must be designed for easy maintenance and scalability, allowing for adjustments as the power plant's output or ash generation changes over time.
Role of Shandong HeadPowder Engineering Co., Ltd. in Calcined Ash Material Handling
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling systems, specializes in designing and implementing calcined ash material handling solutions tailored to the specific needs of power plants. With headquarters in Shandong, China, the company leverages decades of experience in the power industry to deliver customized systems that meet both operational and regulatory requirements. The company's team of engineers works closely with clients to assess the characteristics of the calcined ash, including its composition, moisture content, and handling volume, and then develops a comprehensive design that incorporates the key principles outlined above. By focusing on durability, efficiency, and safety, Shandong HeadPowder Engineering Co., Ltd. ensures that its clients can achieve reliable and cost-effective calcined ash transportation, contributing to the overall sustainability and performance of thermal power generation facilities.




