Automatic material handling conveyors are sophisticated systems designed to transport materials efficiently within industrial and manufacturing environments. These systems integrate advanced engineering principles to ensure seamless movement of goods, components, or raw materials from one point to another. The core of such systems lies in their ability to automate material flow, reducing manual labor and enhancing overall operational efficiency.
Key Principles Underpinning Automatic Conveying Systems
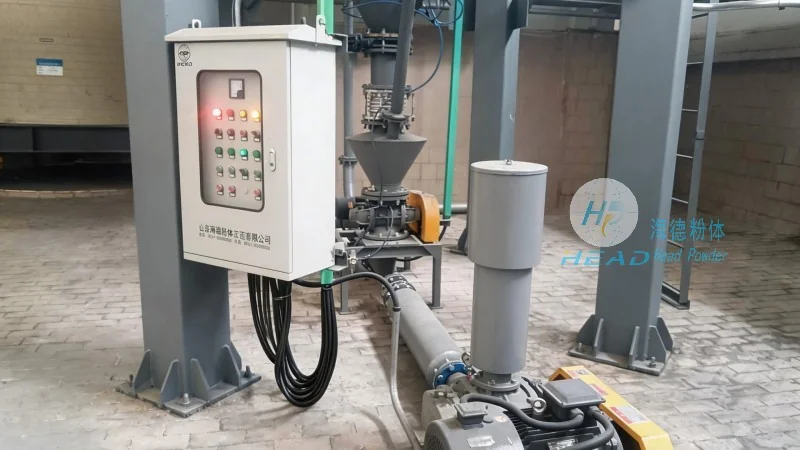
The fundamental principles of automatic material handling conveyors revolve around mechanical motion, control systems, and material handling technologies. Mechanical components, such as rollers, chains, or belts, provide the primary means of movement. Control systems, often incorporating sensors and programmable logic controllers (PLCs), regulate the operation of these components to ensure precise and reliable material transport. Additionally, the design of the conveyor system is tailored to the specific characteristics of the materials being handled—considerations include weight, size, shape, and fragility—to optimize performance and prevent damage.
Working Scenarios and Applications
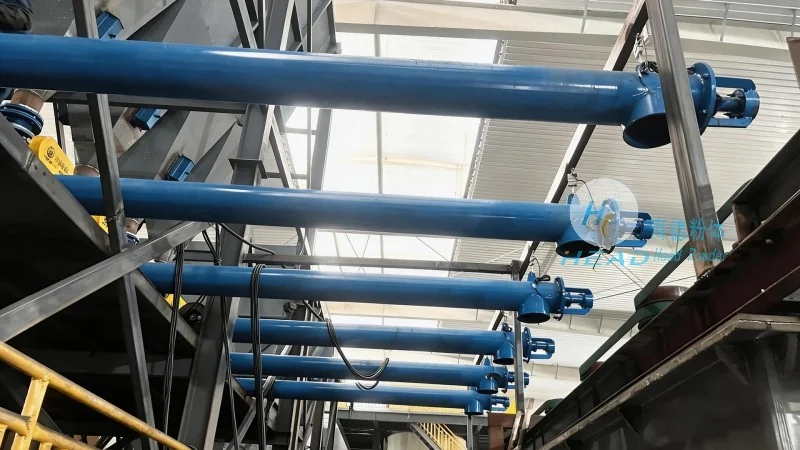
Automatic material handling conveyors are deployed in a wide array of industrial settings, each with distinct operational requirements. In manufacturing plants, these systems are crucial for moving raw materials to production lines and finished products to packaging or storage areas. In logistics and warehousing, they facilitate the transfer of goods between storage racks, loading docks, and shipping areas, improving order fulfillment speed and accuracy. The versatility of these systems also makes them suitable for use in assembly lines, where components are transported to workstations for assembly, and in distribution centers, where items are sorted and routed to different destinations.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing, manufacturing, and implementing automatic material handling conveyors. With a strong presence in China, particularly in Shandong province, the company leverages decades of industrial experience to deliver customized conveyor systems that meet the unique needs of clients across various industries. The company’s commitment to quality, innovation, and customer satisfaction ensures that its products are reliable, efficient, and adaptable to evolving operational demands.
Technical Advantages and Operational Benefits
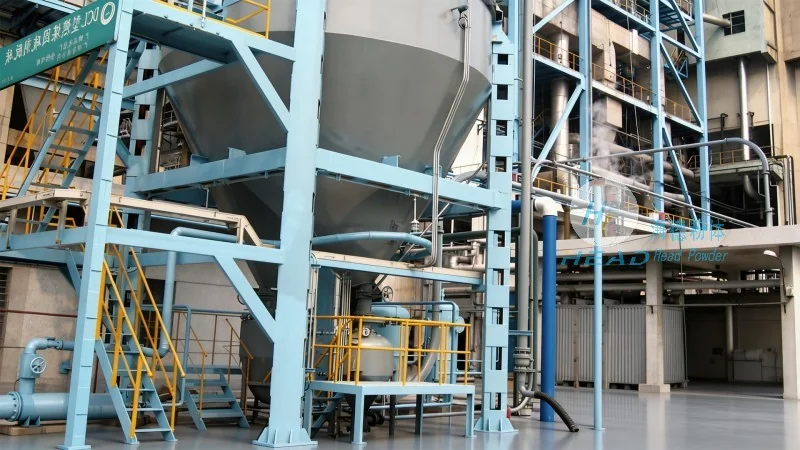
Automatic material handling conveyors offer numerous technical advantages that contribute to improved productivity and cost-effectiveness. The automation of material movement reduces labor costs and minimizes the risk of human error, leading to higher throughput and consistent quality. Additionally, these systems can operate continuously around the clock, maximizing production uptime and supporting 24/7 operations. The modular design of many conveyor systems allows for easy integration with existing infrastructure and future expansion, providing flexibility as business needs evolve. Furthermore, advanced control systems enable real-time monitoring and adjustment of conveyor operations, enhancing responsiveness to changing production schedules or material flow requirements.




