HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of dilute phase material conveying systems. These systems are engineered to efficiently transport bulk materials through pipelines using a low concentration of material suspended in a gas stream, typically air or other gases. The core principle of dilute phase conveying involves creating a pneumatic transport system where the material particles are dispersed in the gas, allowing for high-speed and long-distance transportation with minimal friction and energy loss compared to traditional methods like belt conveyors or bucket elevators.
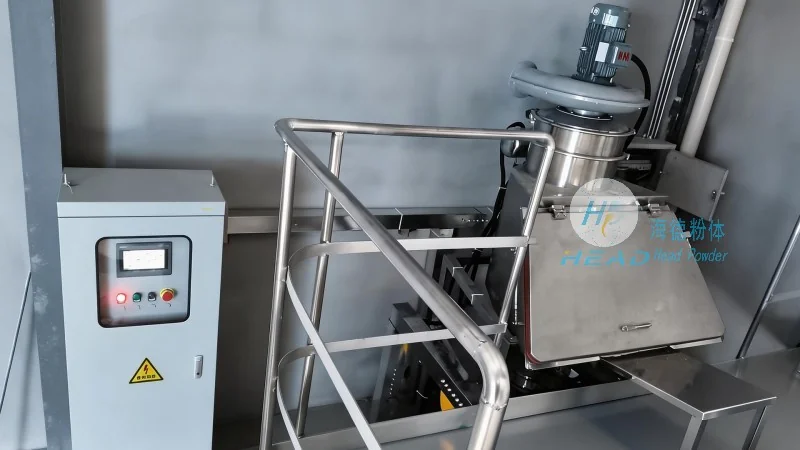
The operational principle of a dilute phase material conveying system centers on the balance between the gas velocity and the material's particle size and density. When the gas velocity exceeds the terminal velocity of the material particles, the particles are lifted and carried along the pipeline. This process ensures that the material remains in a suspended state throughout the conveying path, reducing the risk of blockages and wear on the system components. The system typically includes key components such as a material feeder, a gas compressor or blower, a pipeline network, and a discharge unit. The feeder ensures a consistent material feed, while the compressor provides the necessary pressure and velocity to move the material through the pipeline. The pipeline network may include bends, vertical sections, and horizontal runs, all designed to maintain the material's suspended state and minimize pressure drop.
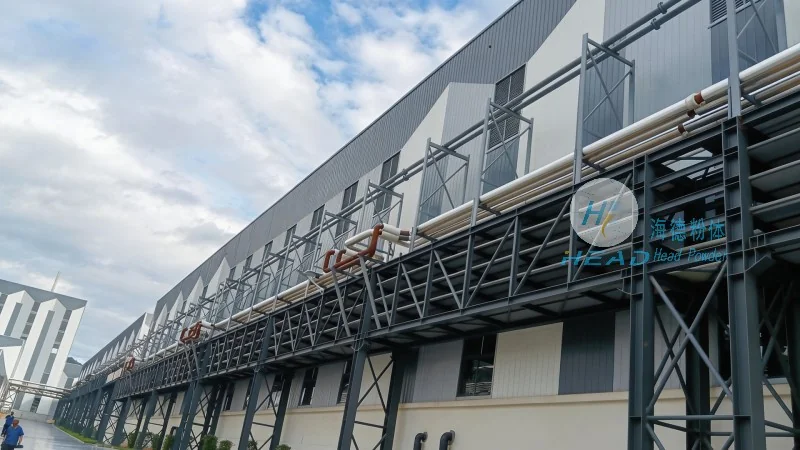
One of the primary advantages of dilute phase material conveying is its ability to handle a wide range of materials, including powders, granules, and fine particles. This versatility makes it suitable for various industrial applications across different sectors. For instance, in the chemical industry, dilute phase systems are used to transport raw materials like powders and granules from storage silos to processing units. In the food industry, these systems are employed to convey ingredients such as flour, sugar, and spices with high hygiene standards, ensuring minimal contamination and product quality maintenance. The pharmaceutical industry also benefits from dilute phase conveying, as it allows for the safe and efficient transport of active pharmaceutical ingredients (APIs) and other sensitive materials, adhering to stringent regulatory requirements.
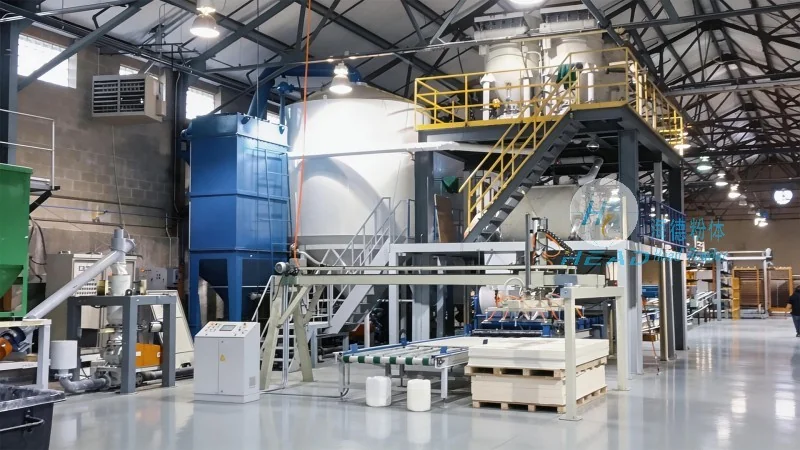
In the mining and mineral processing sector, dilute phase material conveying is crucial for transporting ore and concentrates from mining sites to processing plants. The system's ability to handle abrasive materials and high volumes makes it ideal for long-distance transport, reducing the need for multiple transfer points and associated equipment. Similarly, in the cement industry, these systems are used to convey raw materials like limestone and clinker, as well as finished cement products, ensuring efficient supply chain management and reduced operational costs.
The working scenarios of dilute phase material conveying systems are diverse and tailored to specific industrial needs. For example, in the power generation industry, these systems are used to transport coal or biomass fuel from storage to the boiler, optimizing fuel delivery and combustion efficiency. In the agricultural sector, dilute phase conveying is employed to transport grain and other agricultural products from fields to processing facilities or storage silos, enhancing productivity and reducing manual labor. The flexibility of dilute phase systems also allows for integration with existing infrastructure, making them a cost-effective solution for upgrading or expanding material handling capabilities.
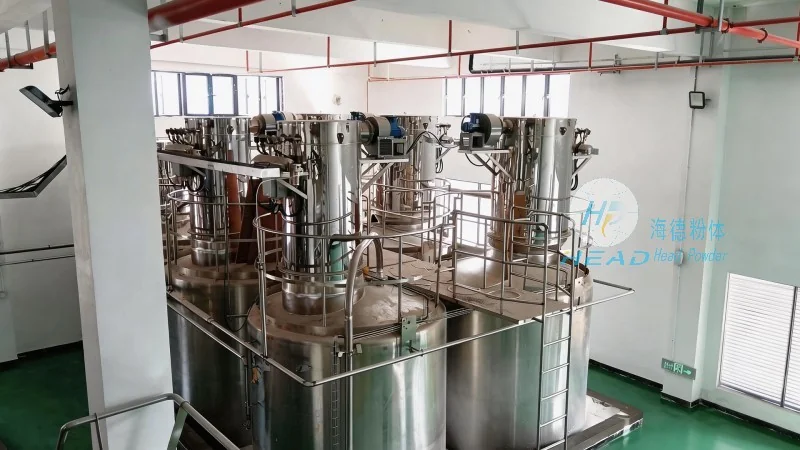
HeadPowder's expertise in dilute phase material conveying systems is built on decades of experience and a commitment to innovation. The company's engineers and technicians work closely with clients to understand their specific material handling challenges and design customized solutions that meet operational requirements, safety standards, and budget constraints. By leveraging advanced engineering principles and state-of-the-art technology, HeadPowder ensures that its dilute phase conveying systems deliver reliable performance, high efficiency, and long-term durability. The company's focus on customer satisfaction and technical excellence has made it a trusted partner for industries worldwide, providing sustainable and efficient material handling solutions.




