HeadPowder, a leading provider of industrial pneumatic conveying solutions, specializes in gravity dust removal systems designed to efficiently transport fine powders and dust particles. This equipment is crucial in various industrial applications, including pharmaceuticals, food processing, and chemical manufacturing, where maintaining air quality and material integrity is paramount. The gravity dust removal pneumatic conveying equipment from HeadPowder Engineering Co., Ltd. is engineered to handle high volumes of fine materials while ensuring minimal environmental impact and operational efficiency.
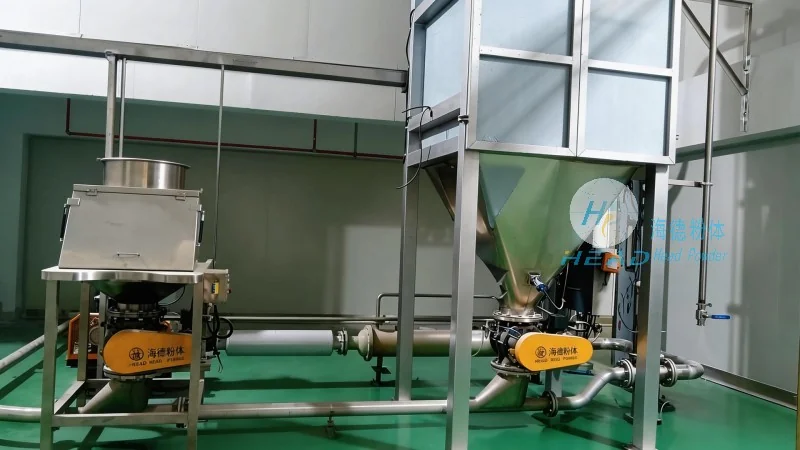
Working Principle of the Gravity Dust Removal System
The core of the gravity dust removal pneumatic conveying equipment lies in its ability to utilize gravity and air flow to separate and transport dust particles. The system typically consists of a hopper, a conveying pipe, and a dust collector. As material is introduced into the hopper, it flows under gravity into the conveying pipe. Simultaneously, a controlled airflow is introduced, creating a low-pressure environment that draws the material through the pipe. The design ensures that only fine particles are conveyed, while larger or heavier particles settle back into the hopper due to gravity. This separation process minimizes material loss and ensures efficient transport. The air compressor plays a vital role in generating the necessary airflow, which is adjusted based on the material's characteristics and the required conveying distance. The system's efficiency is enhanced by the use of smooth, corrosion-resistant pipes and optimized hopper designs that prevent material buildup and ensure consistent flow.
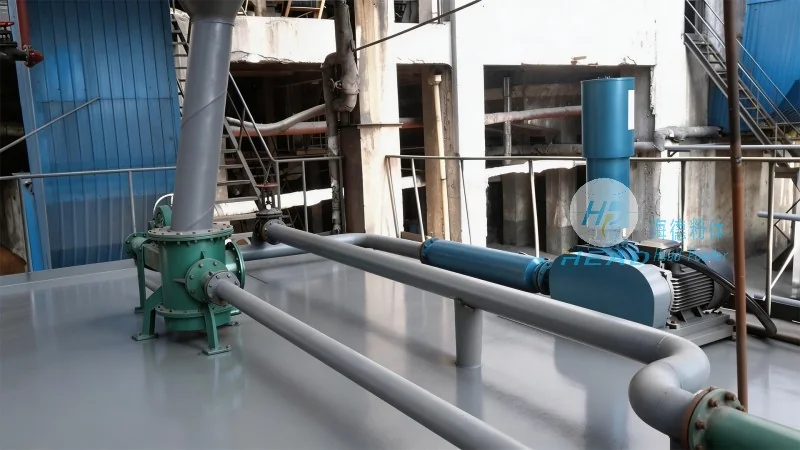
Operation Process of the Pneumatic Conveying System
The operation of the gravity dust removal system begins with the loading of material into the hopper. The hopper is equipped with a feeding mechanism that controls the flow rate of the material, preventing overloading and ensuring a steady supply to the conveying pipe. Once the material is in the hopper, the conveying system is activated. The air compressor generates a steady airflow that is directed into the conveying pipe, creating a negative pressure that pulls the material from the hopper into the pipe. As the material travels through the pipe, it is mixed with the air, forming a slurry-like mixture. The mixture then reaches the destination point, where the material is discharged into a storage bin or processing unit. The air, now carrying fine particles, is directed to a dust collector, which employs filtration or cyclonic separation to remove the particles from the air stream. The clean air is then either returned to the system for reuse or exhausted to the environment, depending on the system's configuration. The system operates continuously, with the hopper and conveying pipe designed to handle high volumes of material without clogging or loss, ensuring consistent performance over extended periods.
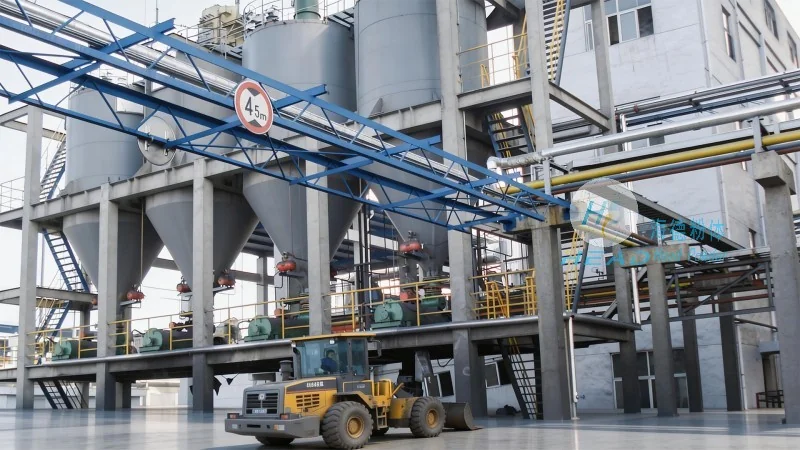
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in the design, development, and production of advanced pneumatic conveying equipment. With years of experience in the industry, the company has built a strong reputation for delivering high-quality, reliable, and efficient solutions tailored to meet the specific needs of its clients. The company's commitment to innovation and customer satisfaction has enabled it to serve a wide range of industries, providing customized solutions that enhance operational efficiency and reduce costs. HeadPowder's team of engineers and technicians work closely with clients to understand their unique requirements and develop tailored systems that optimize material handling processes. The company adheres to strict quality control standards, ensuring that each piece of equipment meets or exceeds industry benchmarks for performance, durability, and safety. With a focus on sustainability and environmental responsibility, HeadPowder's products are designed to minimize energy consumption and reduce emissions, aligning with global trends toward greener industrial practices.




