Desulfurizer powder conveying equipment is a critical component in modern industrial processes, particularly within the framework of flue gas desulfurization (FGD) systems. These systems are engineered to efficiently transport desulfurizer powders, which are essential for reducing sulfur dioxide (SO₂) emissions from industrial sources. The reliable operation of such equipment directly impacts the effectiveness of pollution control measures and overall environmental compliance, making it a vital asset for industries committed to sustainable operations.
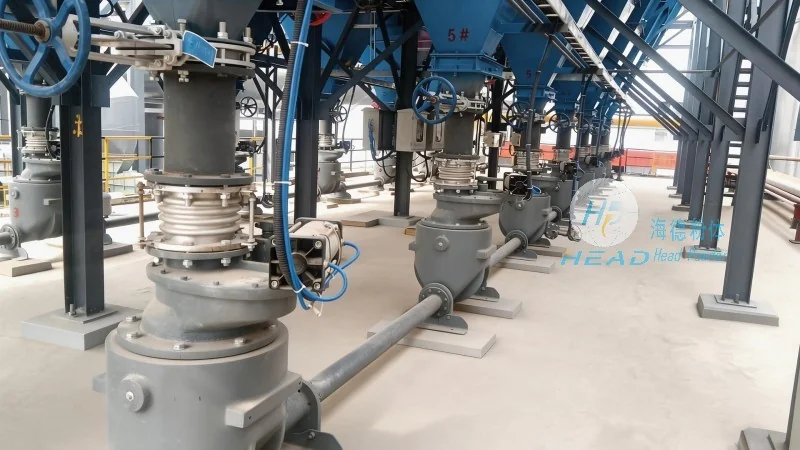
Company Profile and Corporate Identity
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in engineering solutions for powder handling and conveying systems. With its operational base in Shandong, China, the company has established a strong reputation for delivering high-quality, customized equipment tailored to the unique needs of various industrial sectors. HeadPowder's expertise lies in understanding the challenges associated with handling fine powders, such as desulfurizer materials, and developing innovative solutions that ensure optimal performance, safety, and longevity. The company's commitment to quality and customer satisfaction has positioned it as a trusted partner in the field of industrial powder processing.
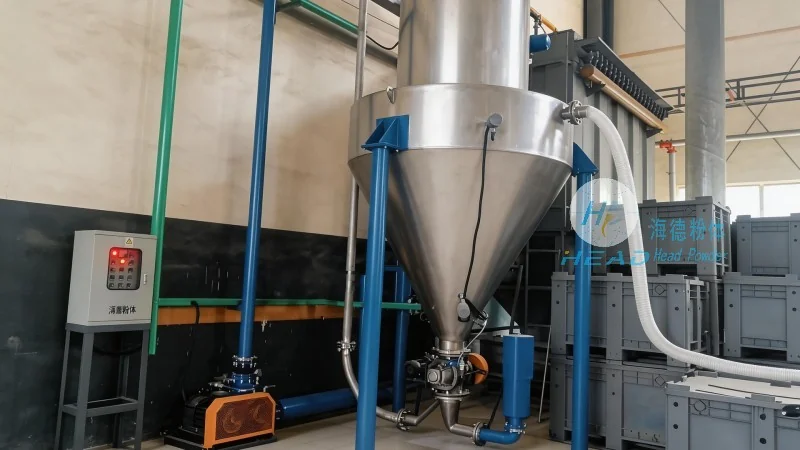
The Fundamental Principle of Desulfurizer Powder Conveying Equipment
The core principle of desulfurizer powder conveying equipment revolves around the efficient transport of fine powders from storage to processing units. These systems typically employ either pneumatic or mechanical methods to achieve material movement. Pneumatic conveying utilizes compressed air to create a flow that carries the powder through pipelines, while mechanical systems may utilize screw conveyors, belt conveyors, or bucket elevators. The choice of method depends on factors like particle size, moisture content, and the required conveying distance. For desulfurizer powders, which are often fine and hygroscopic, pneumatic systems are commonly preferred due to their ability to handle delicate materials without causing degradation or agglomeration. The equipment is designed to maintain consistent flow rates and pressure, ensuring reliable delivery of the desulfurizer to the reaction tower or processing unit.
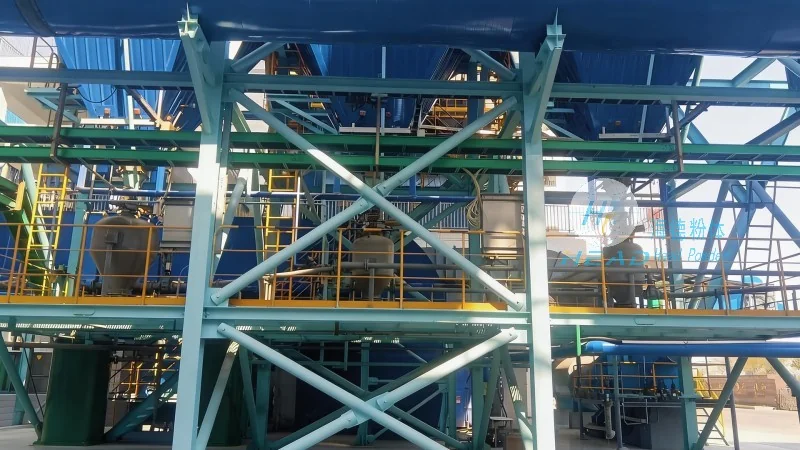
Working Scene Characteristics and Application Environments
The working scene characteristics of desulfurizer powder conveying equipment vary significantly based on the industrial application. In coal-fired power plants, for example, these systems are integrated into the FGD process, where they transport limestone or other alkaline powders to reaction towers. The equipment must operate under high-pressure and high-temperature conditions, ensuring consistent flow rates and minimal downtime. In chemical manufacturing facilities, the conveying equipment may be part of a larger production line, handling desulfurizer powders for downstream processing. The key characteristics in such scenarios include high capacity, low maintenance requirements, and the ability to handle abrasive materials without causing wear on components. Additionally, the equipment must be designed for easy integration with existing infrastructure, allowing for seamless operation within the plant's workflow. The working environment may also involve exposure to corrosive substances, requiring equipment constructed from corrosion-resistant materials to ensure durability and longevity.
Key Features and Advantages of the Equipment
Desulfurizer powder conveying equipment from HeadPowder is engineered with several key features that enhance performance and reliability. These include advanced control systems that monitor flow rates, pressure, and material levels in real-time, ensuring precise operation. The equipment is also constructed with corrosion-resistant materials to withstand the acidic and alkaline environments typical of desulfurization processes. Another advantage is the ability to handle varying particle sizes and moisture content, making it versatile for different applications. The systems are designed for low energy consumption, contributing to cost savings and environmental sustainability. Furthermore, the equipment is equipped with safety features such as pressure relief valves and emergency shut-off mechanisms, ensuring operational safety and compliance with industrial standards. The equipment's design also emphasizes ease of maintenance, with accessible components that allow for quick repairs and replacements, minimizing downtime and operational disruptions.
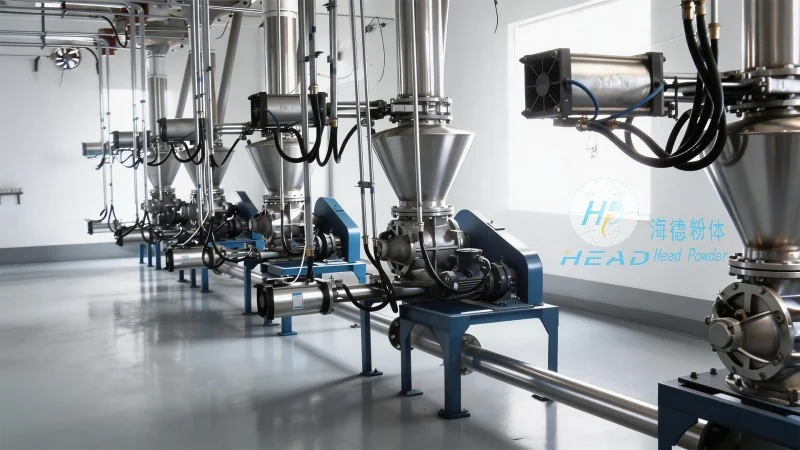
Real-World Application Examples and Industry Impact
Real-world applications of desulfurizer powder conveying equipment demonstrate its critical role in reducing air pollution. In coal-fired power plants, the efficient transport of desulfurizer powders is essential for maintaining the FGD system's effectiveness, which in turn reduces sulfur dioxide emissions by up to 95%. In industrial chemical plants, the equipment ensures a steady supply of desulfurizer materials, supporting continuous production and meeting environmental regulations. The impact of these systems extends beyond pollution control; they also contribute to operational efficiency by minimizing material waste and reducing the need for manual handling, which can be hazardous. By providing reliable and efficient conveying solutions, HeadPowder's equipment helps industries achieve their environmental goals while maintaining productivity. The equipment's performance directly correlates with the overall success of the desulfurization process, making it an indispensable component in modern industrial operations.




