Quartz stone powder, a widely used material in various industries such as construction, ceramics, and electronics, requires efficient and reliable conveying systems to ensure smooth production processes. The process of transporting quartz stone powder from storage to processing equipment is critical for maintaining productivity and product quality. This article explores the working principle and key characteristics of quartz stone powder conveying systems, providing insights into how these technologies operate and their advantages in industrial applications.
Working Principle of Quartz Stone Powder Conveying
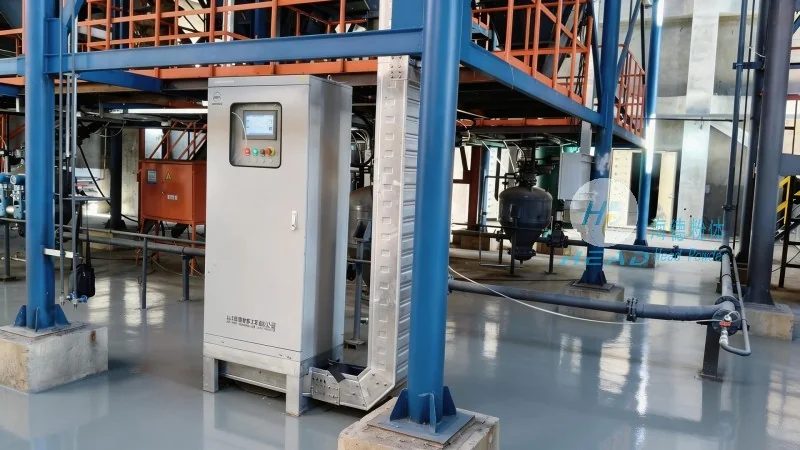
The working principle of quartz stone powder conveying typically involves a series of components and steps designed to handle the material's properties, such as its fine particle size and potential for dust generation. The process generally starts with the storage of quartz stone powder in a hopper or silo. From there, the material is fed into a conveyor system, which may include screw conveyors, pneumatic conveyors, or bucket elevators, depending on the specific requirements of the application.
Screw conveyors are commonly used for horizontal or slightly inclined transport of quartz stone powder. They consist of a rotating screw within a trough, which moves the material forward by friction. This method is suitable for moderate to high volumes and is relatively simple to install and maintain. Pneumatic conveyors, on the other hand, use air pressure to transport the powder through a pipeline. This system is ideal for long-distance or vertical transport and can handle fine powders effectively, minimizing the risk of blockages.
Bucket elevators are another option, particularly for vertical transport of quartz stone powder. These systems use a series of buckets attached to a belt or chain that moves the material upward. The design ensures that the powder is contained within the buckets, preventing spillage and dust emission. Control systems, including sensors and valves, regulate the flow rate and pressure to maintain consistent operation.
Key Features of Quartz Stone Powder Conveying
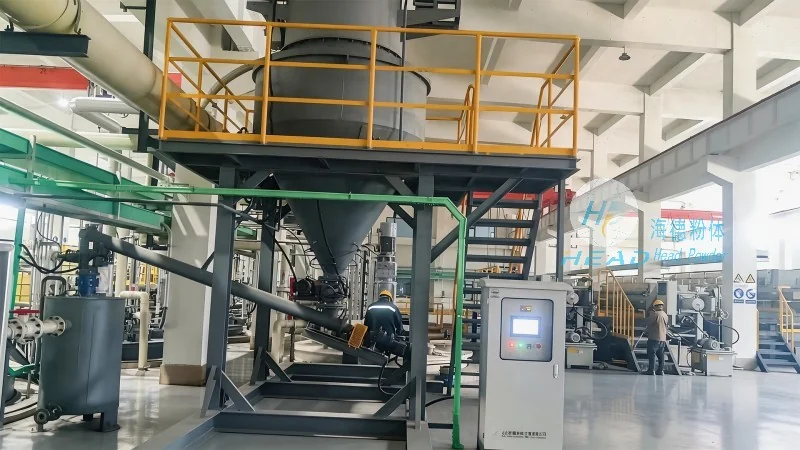
Several key features distinguish effective quartz stone powder conveying systems, making them suitable for diverse industrial needs. One of the primary features is the ability to handle fine powders without clogging or blockages. This is achieved through the use of specialized materials for conveyor components, such as stainless steel or food-grade plastics, which resist abrasion and corrosion from the quartz stone powder.
Another important feature is the system's efficiency in maintaining material integrity. Quartz stone powder is often sensitive to moisture and contamination, so conveying systems must minimize exposure to these factors. Enclosed designs and sealed components help prevent dust contamination and moisture absorption, ensuring the powder remains in optimal condition for downstream processes.
Energy efficiency is also a significant characteristic of modern quartz stone powder conveying systems. Advanced control technologies, such as variable frequency drives (VFDs), adjust the motor speed based on the material flow rate, reducing energy consumption. This not only lowers operational costs but also contributes to environmental sustainability.
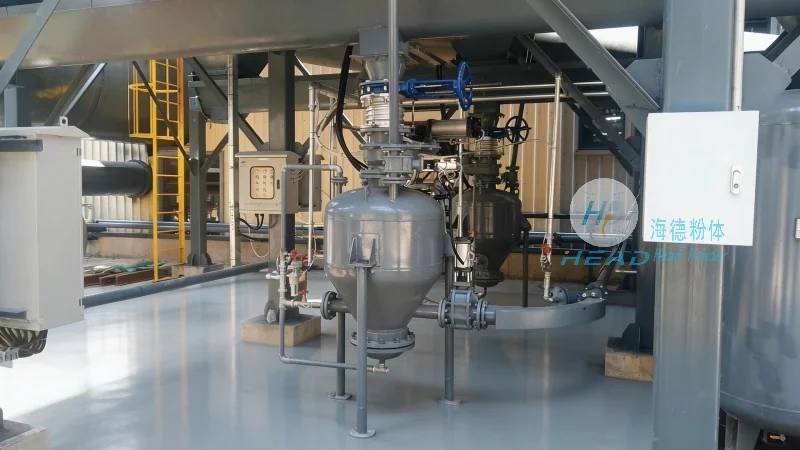
Adaptability to different production scales is another key feature. Whether for small-scale laboratory applications or large-scale industrial production, conveying systems can be customized to meet specific requirements. Modular designs allow for easy expansion or modification, ensuring that the system can grow with the company's needs.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing advanced conveying systems for quartz stone powder and other fine materials. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to develop cutting-edge technologies tailored to global market demands.
The company's team of engineers and technicians works closely with clients to understand their specific conveying needs, offering customized solutions that enhance operational efficiency and product quality. By integrating the latest technologies and adhering to strict quality standards, HeadPowder ensures that its conveying systems meet the highest industry benchmarks. This commitment to excellence has made HeadPowder a preferred choice for businesses seeking reliable and efficient powder handling solutions.




