Rare earth mineral powder material handling is a critical process in industries that rely on these valuable resources. The efficient transportation and processing of rare earth powders require specialized equipment and design principles to ensure safety, efficiency, and product integrity. Understanding the fundamentals of this material handling system is essential for optimizing operations in mining, processing, and manufacturing sectors.
Key Design Principles for Rare Earth Powder Material Handling
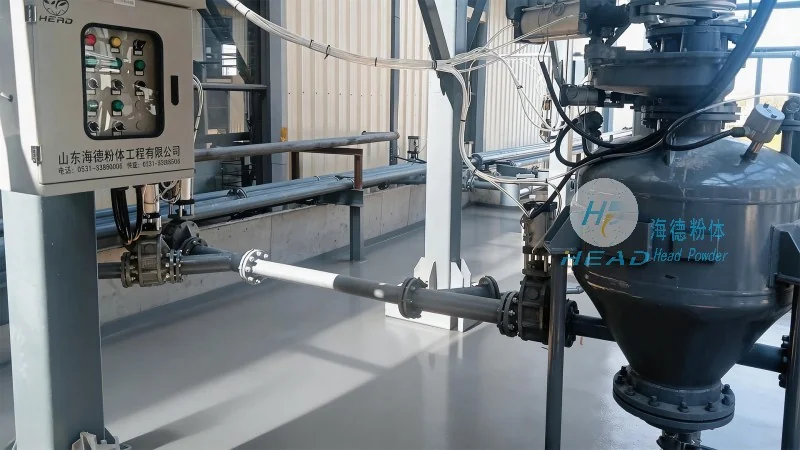
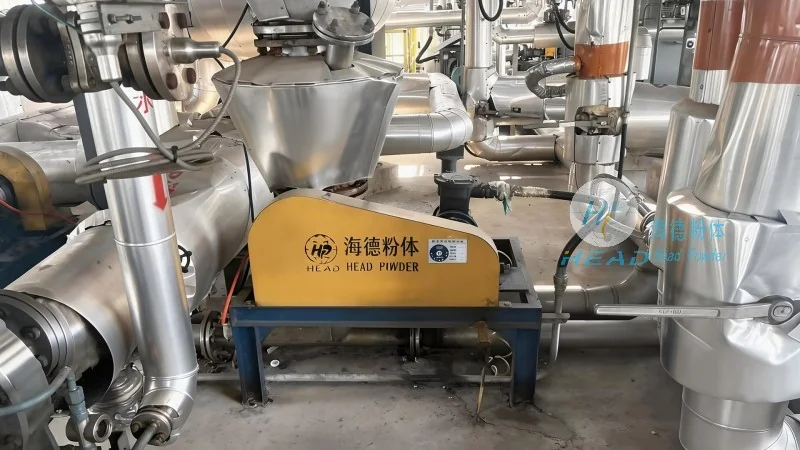
The design of rare earth mineral powder handling systems is guided by several key principles that address the unique properties of these materials. First, the system must be designed to minimize dust generation and control air quality, as rare earth powders can be hazardous if inhaled. This often involves the use of enclosed conveyor systems, dust collection equipment, and proper ventilation. Second, the equipment must be constructed from materials that are resistant to corrosion and wear, as rare earth powders can be abrasive and chemically reactive under certain conditions. Stainless steel, special alloys, and wear-resistant coatings are commonly used in the construction of hoppers, chutes, and conveyor belts. Third, the system should incorporate features that prevent material buildup and blockages, which can lead to system downtime and safety hazards. This includes the use of inclined chutes, vibration feeders, and regular maintenance schedules. Finally, the design must prioritize energy efficiency and operational cost reduction, as rare earth processing is often a high-cost operation. Advanced control systems and energy-saving components are integrated into modern material handling solutions to achieve these goals. Additionally, the system must comply with relevant safety regulations and environmental standards to ensure the well-being of workers and the protection of the environment.
Components of a Typical Rare Earth Powder Material Handling System
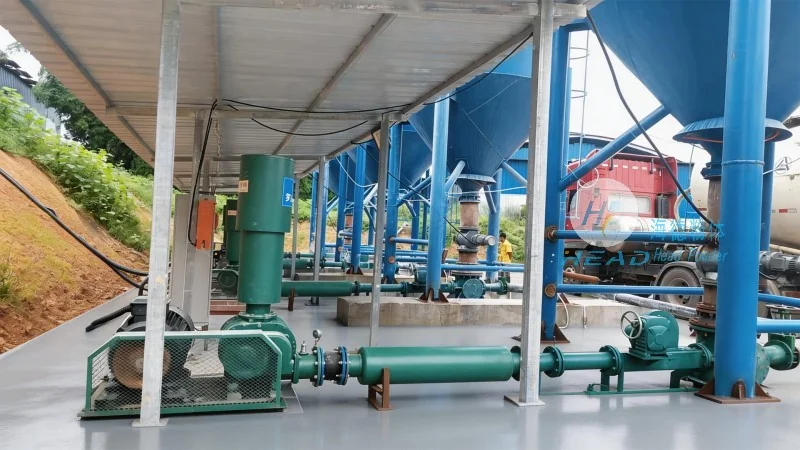
A typical rare earth mineral powder material handling system consists of several interconnected components that work together to transport and process the material. The primary components include feeders, conveyors, storage hoppers, and processing equipment. Feeders, such as rotary valves or vibratory feeders, are used to control the flow rate of the powder from the storage hopper to the conveyor system. These devices ensure a consistent and controlled feed, preventing overloading or underloading of the conveyor. Conveyors, often in the form of belt conveyors or screw conveyors, transport the powder from one location to another within the processing facility. Belt conveyors are commonly used for longer distances and higher capacities, while screw conveyors are suitable for vertical or horizontal transport in confined spaces. Storage hoppers are used to hold the raw rare earth powder before it is processed. These hoppers are typically designed with sloped sides to facilitate material flow and prevent caking or bridging. The processing equipment, such as grinding mills or classifiers, may be integrated into the system to further refine the powder to the desired particle size. Each component is carefully selected and sized based on the specific characteristics of the rare earth material, including its density, moisture content, and flowability. The integration of these components is critical to the overall efficiency and reliability of the material handling system.
HeadPowder's Expertise in Rare Earth Material Handling Solutions
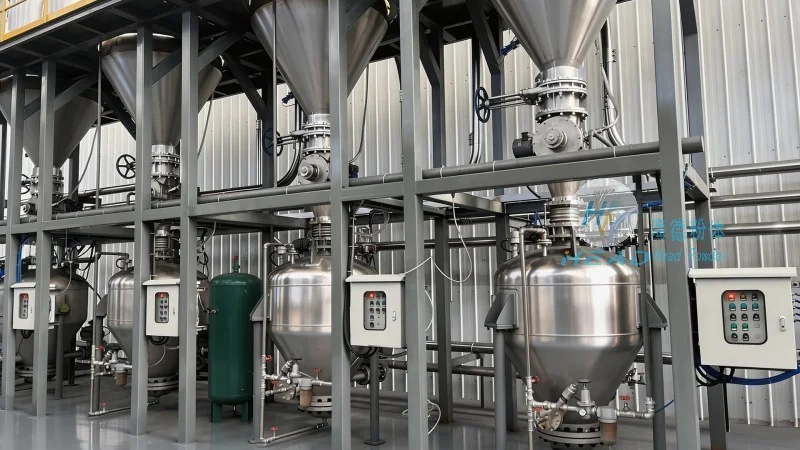
Shandong HeadPowder Engineering Co., Ltd. (often referred to as HeadPowder) is a leading provider of specialized material handling solutions for rare earth mineral powders. With years of experience in the industry, HeadPowder has developed a deep understanding of the unique challenges associated with handling these valuable resources. The company's expertise lies in designing and manufacturing custom systems that meet the specific needs of its clients. HeadPowder's team of engineers and technicians work closely with clients to assess their operational requirements, material properties, and safety standards. This collaborative approach ensures that the final system is optimized for performance, reliability, and cost-effectiveness. The company utilizes advanced design software and testing methodologies to simulate and validate the performance of its material handling systems before installation. This ensures that the system meets or exceeds industry standards for efficiency and safety. HeadPowder's products are known for their durability, low maintenance requirements, and ability to handle the abrasive and corrosive nature of rare earth powders. The company's commitment to quality and customer satisfaction has made it a trusted partner for many companies operating in the rare earth industry. HeadPowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality solutions to clients worldwide.




