Small bag unpacking powder conveying systems are specialized industrial equipment designed to handle the efficient and safe transfer of bulk powders from sealed bags into processing or storage facilities. This equipment is crucial in industries such as pharmaceuticals, food processing, chemicals, and agriculture, where handling powders requires precision and minimal contamination. The system typically integrates several key components, including a bag opening mechanism, a powder suction or feeding unit, and a conveying pipeline that transports the material to its destination. Understanding the design principles behind these systems is essential for optimizing performance, ensuring product quality, and maintaining operational safety.
Key Components of Small Bag Unpacking Powder Conveying Systems
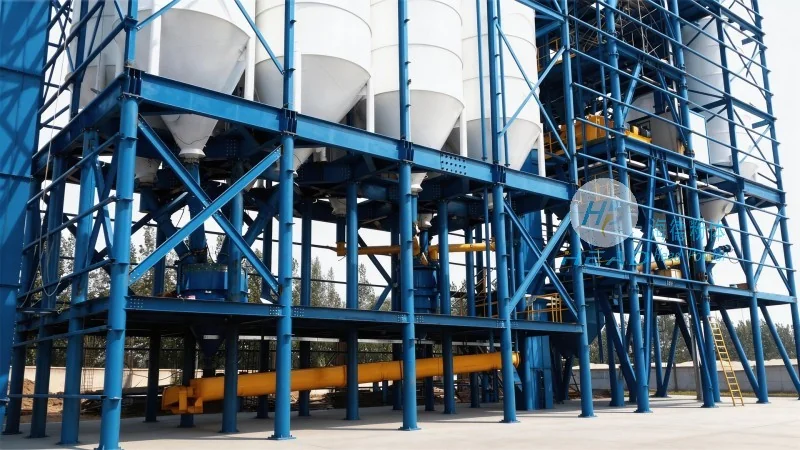
The core components of a small bag unpacking powder conveying system include the bag opening unit, the powder handling module, and the conveying infrastructure. The bag opening mechanism is engineered to safely and hygienically open sealed bags without compromising the integrity of the powder inside. Common methods include mechanical cutting, air pressure release, or automated opening tools that minimize dust generation and product loss. The powder handling module, often equipped with a vacuum or pressure system, draws the material from the opened bag and transfers it to the conveying pipeline. This module may feature filters or separators to remove foreign particles or moisture, ensuring the powder meets quality standards. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, transports the powder to the processing area or storage silo. The system may also include a control panel that monitors and regulates the flow rate, pressure, and other operational parameters to maintain consistent performance.
Design Principles for Efficient Powder Handling
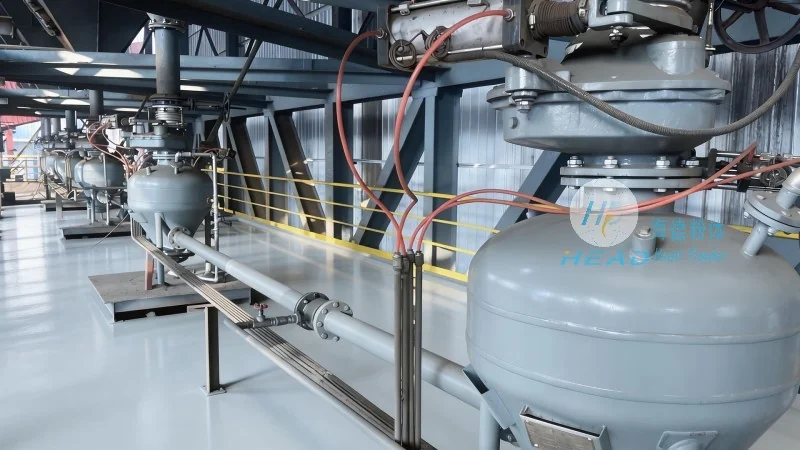
The design of small bag unpacking powder conveying systems is guided by several critical principles aimed at maximizing efficiency, minimizing downtime, and ensuring product purity. One key principle is the minimization of material loss and contamination. This is achieved through careful engineering of the bag opening process, which avoids direct contact with the powder and uses sealed or enclosed systems to prevent cross-contamination. Another principle is the optimization of airflow and pressure to ensure consistent and reliable powder transfer. The system is designed to maintain a stable pressure differential between the bag and the conveying line, preventing air leakage and ensuring the powder flows smoothly without clogging. Additionally, the design incorporates features to handle different powder properties, such as varying densities, flowability, and moisture content. Adjustable parameters, such as the speed of the bag opening mechanism or the suction pressure, allow operators to adapt the system to different materials, enhancing versatility and performance.
Operational Benefits and Applications
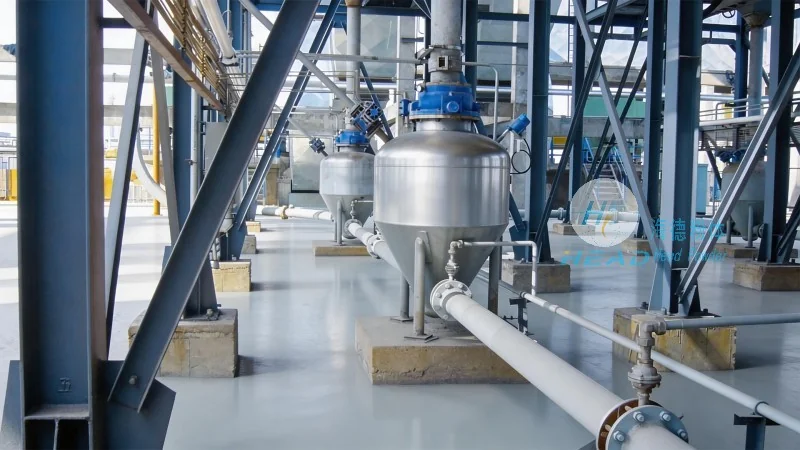
Small bag unpacking powder conveying systems offer numerous operational benefits across various industries. In pharmaceutical manufacturing, these systems enable the safe handling of active pharmaceutical ingredients (APIs) and excipients, reducing the risk of contamination and ensuring compliance with stringent regulatory standards. In the food industry, they facilitate the transfer of ingredients like flour, sugar, and spices, maintaining hygiene and product quality. For chemical manufacturers, the systems help handle bulk chemicals, improving process efficiency and reducing labor costs. The ability to handle multiple bag sizes and types further enhances the system's utility, making it suitable for diverse production environments. Furthermore, the automated nature of these systems reduces the need for manual labor, minimizing human error and improving overall productivity. By streamlining the powder handling process, these systems contribute to cost savings and operational efficiency in industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced powder handling equipment. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. HeadPowder's expertise lies in integrating cutting-edge technology with practical engineering to deliver reliable and efficient systems that meet the highest standards of performance and safety. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing equipment and a team of skilled engineers who work closely with clients to understand their requirements and deliver optimal solutions. By focusing on customer satisfaction and continuous improvement, HeadPowder has built a reputation for excellence in the powder conveying equipment market.




