The dust collection powder conveying system equipment, commonly used in industrial settings, is a specialized machinery designed to handle and transport collected dust and powders efficiently. This equipment plays a crucial role in maintaining air quality and ensuring the safe and effective removal of particulate matter from industrial processes. The system typically integrates dust collection mechanisms with conveying technologies to create a comprehensive solution for powder management.
Key Components and Functionality
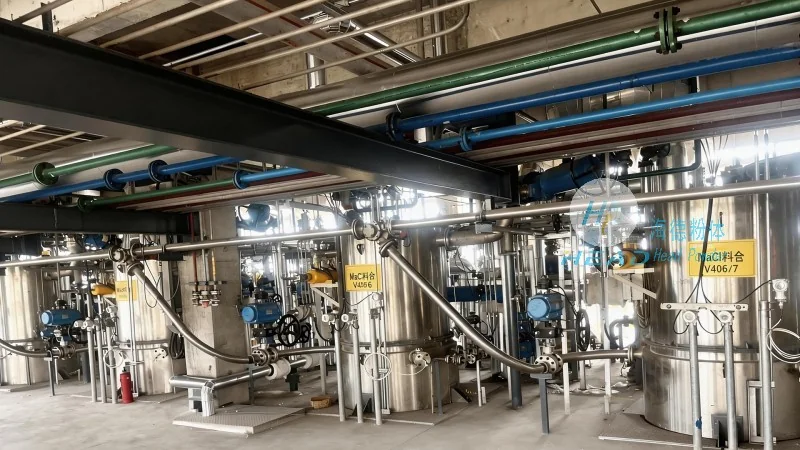
At the core of the dust collection powder conveying system are several key components that work in tandem to achieve optimal performance. The system begins with a dust collector, which captures airborne particles and traps them in a filter or other collection medium. Once the dust is collected, it is transferred to a conveying unit, which may utilize various methods such as pneumatic conveying, mechanical conveying, or a combination of both. Pneumatic conveying, for instance, uses compressed air to move the powder through a pipeline, while mechanical conveying relies on screws, belts, or other mechanical means to transport the material. The choice of conveying method depends on factors like the powder's properties, the distance to be covered, and the required flow rate.
Design Principles and Engineering Considerations
The design of a dust collection powder conveying system equipment is guided by several fundamental principles aimed at maximizing efficiency, reliability, and safety. Engineers must consider the physical properties of the powder, including its particle size, moisture content, and flowability, as these characteristics directly impact the system's performance. For example, cohesive or sticky powders may require specialized equipment like vibratory conveyors or air slides to prevent blockages and ensure smooth transport. Additionally, the system's design must account for the need to maintain consistent pressure and airflow in pneumatic conveying systems to avoid material degradation or loss of product quality. The integration of dust collection and conveying also necessitates careful consideration of material compatibility, ensuring that the equipment components can withstand the corrosive or abrasive nature of the collected dust without degradation over time.
Applications and Industry Use Cases
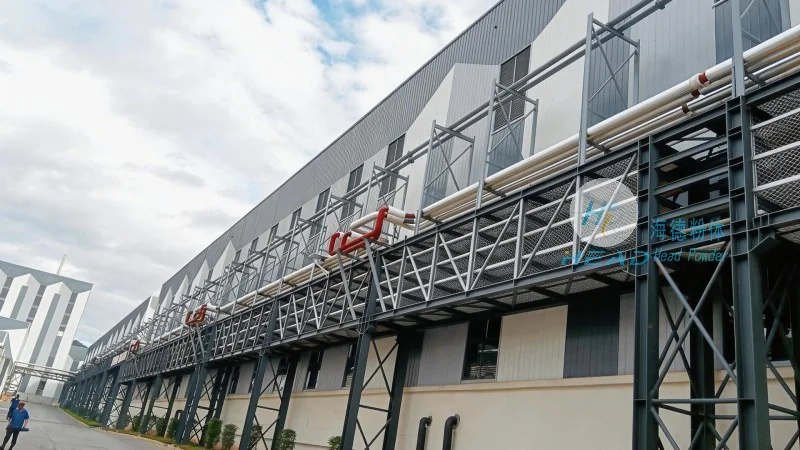
Dust collection powder conveying systems find widespread application across various industries, including manufacturing, mining, and food processing. In manufacturing facilities, these systems are essential for handling powders from processes like grinding, mixing, and drying, where dust generation is common. The equipment helps maintain a clean and safe working environment by preventing dust from spreading into the air and potentially causing health hazards or equipment damage. In mining operations, dust collection systems are used to remove dust from ore processing, reducing the risk of respiratory illnesses among workers and improving overall operational safety. Similarly, in the food industry, specialized dust collection systems are employed to handle powders like flour or sugar, ensuring compliance with hygiene standards and preventing contamination.
Advantages of Using a Dust Collection Powder Conveying System
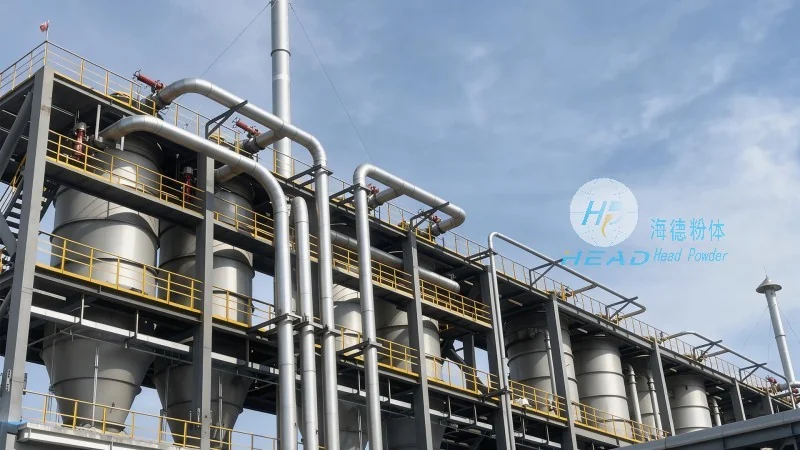
Implementing a dust collection powder conveying system offers numerous advantages for industrial operations. One of the primary benefits is the improvement in air quality, as the system effectively removes particulate matter from the workplace, reducing the risk of respiratory issues and other health problems associated with dust exposure. Additionally, the equipment enhances operational efficiency by streamlining the process of handling and transporting powders, minimizing downtime and labor costs associated with manual handling. The system also contributes to environmental compliance by reducing the amount of dust released into the atmosphere, helping businesses meet regulatory requirements and maintain a positive environmental reputation. Furthermore, the use of automated conveying systems can improve product quality by preventing contamination and ensuring consistent material flow, which is critical in industries where precision and consistency are paramount.
Customization and Integration with Existing Systems
HeadPowder, a leading provider of industrial equipment solutions, offers customized dust collection powder conveying systems tailored to meet the specific needs of each client. The company, based in Shandong, China, understands that each industrial application has unique requirements, and their engineering team works closely with clients to design systems that optimize performance and efficiency. Customization options may include adjustments to the conveying method, the size and capacity of the dust collector, or the integration of additional features such as dust filtration or material drying. HeadPowder also ensures that their systems are compatible with existing infrastructure, allowing for seamless integration into current industrial setups without the need for extensive modifications. This approach not only reduces installation time and costs but also ensures that the new system operates in harmony with the existing processes, minimizing disruptions to production.




