When it comes to handling and transporting cocoa powder efficiently, specialized equipment plays a crucial role in maintaining product quality and operational efficiency. This article delves into the cocoa powder conveying system equipment, exploring its design principles and how they contribute to effective material handling in industrial settings.
Introduction to Cocoa Powder Conveying Systems
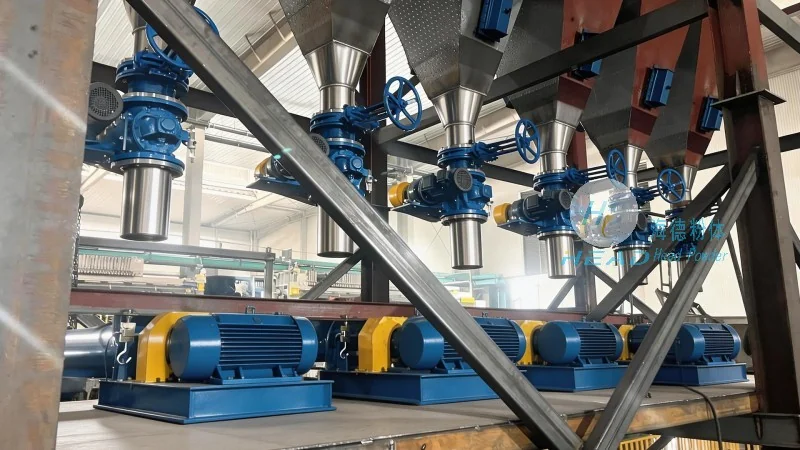
The cocoa powder conveying system equipment is engineered to transport cocoa powder from one location to another within a production facility or processing plant. These systems are essential for ensuring a smooth workflow, minimizing product degradation, and optimizing space utilization. The primary goal is to move the fine, delicate cocoa powder without causing clumping, agglomeration, or loss of quality, which can occur with traditional methods like manual handling or basic pneumatic systems.
Key Components of a Cocoa Powder Conveying System
At the heart of a cocoa powder conveying system are several key components that work in tandem to achieve efficient material transport. These include: conveying lines, which may be made of stainless steel or other food-grade materials to prevent contamination and ensure durability; airlocks that regulate the flow of powder and prevent backflow; filters to maintain air quality and protect the system from dust accumulation; and control panels that allow operators to monitor and adjust the system's performance in real-time.
Design Principles for Efficient Cocoa Powder Conveying
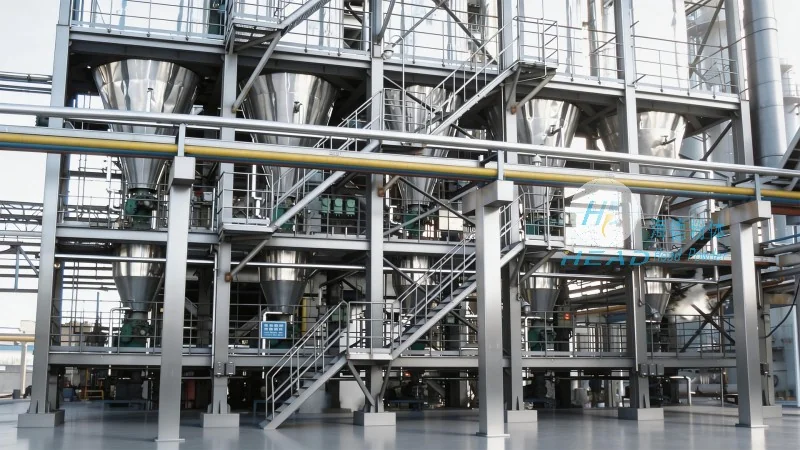
The design of a cocoa powder conveying system is guided by several critical principles aimed at optimizing performance and maintaining product integrity. One of the most important principles is airflow management. Proper air velocity and pressure are essential to prevent the cocoa powder from settling or clogging the system. The system must be designed to handle the specific properties of cocoa powder, such as its fine particle size and tendency to stick to surfaces, ensuring that the material flows smoothly without causing blockages.
Another key design principle is hygiene and sanitation. Since cocoa powder is a food product, the conveying system must meet stringent hygiene standards. Materials used in the construction of the system, such as stainless steel, are non-porous and easy to clean, reducing the risk of bacterial growth or cross-contamination. The system is also designed with smooth surfaces and minimal dead zones where powder can accumulate, making cleaning and maintenance straightforward.
How the System Works: A Step-by-Step Overview
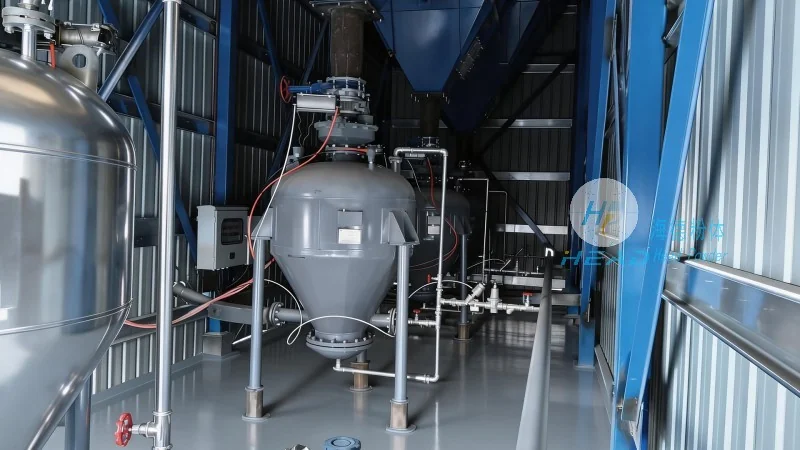
The operation of a cocoa powder conveying system typically involves the following steps: First, the cocoa powder is fed into the system via a hopper or storage silo. The system then uses a combination of air pressure and mechanical components to transport the powder through the conveying lines. Airlocks are used to control the flow and prevent backflow, ensuring that the powder moves in a single direction. Filters are integrated to remove any dust or debris from the air, maintaining air quality and protecting downstream equipment. Finally, the cocoa powder is discharged into the next processing stage or storage container, completing the transport cycle.
Benefits of Using a Cocoa Powder Conveying System
Implementing a dedicated cocoa powder conveying system offers numerous benefits for industrial operations. Firstly, it significantly improves efficiency by automating the material transport process, reducing labor costs and minimizing downtime. Secondly, it enhances product quality by preventing contamination and degradation during handling. The system also optimizes space utilization, as it can be designed to fit into existing production layouts without requiring extensive modifications. Additionally, the hygienic design of the system ensures compliance with food safety regulations, providing peace of mind for manufacturers.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized conveying systems for the food and powder processing industry. With years of experience in designing and manufacturing equipment tailored to the unique needs of cocoa powder and other fine powders, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's commitment to quality, innovation, and customer satisfaction has made them a preferred choice for companies operating in the confectionery, pharmaceutical, and food processing sectors.




